

Direct Factory Sourced Lineup
Industrial & Domestic Fluid Control Assemblies (Showcase I)
Engineered in-house through unified casting, precision machining, and exhaustive pressure calibration. Retained original production inventory ready for direct export deployment.
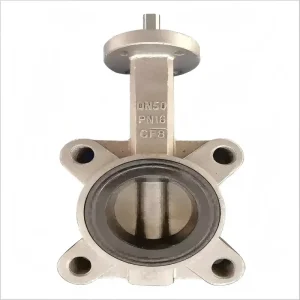
Wholesale Semi Lug Butterfly Valve - Durable & Versatile Flow Control Manufacturers, Manufacturer
Explore Specifications
CE Certification WRAS Approved High-Performance Butterfly Valve 4020G Manufacturer, Factories
Explore Specifications
Wholesale PTFE Lined Butterfly Valve - Durable & Corrosion Resistant Manufacturers, Manufacturer
Explore Specifications
CE Certification Wafer Butterfly Valve,water usage butterfly valve Suppliers, Factories
Explore Specifications
High-Quality Actuator Wafer Butterfly Valve Supplier, Manufacturers
Explore Specifications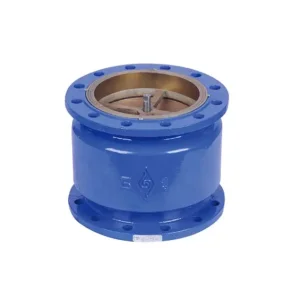
CE Certification Energy-Saving Silencer Check Valve Suppliers, Supplier
Explore Specifications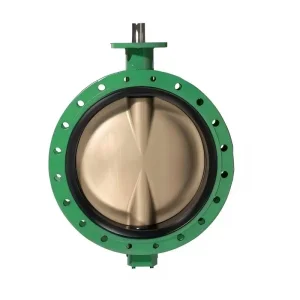
High-Quality Water Used Flanged Butterfly Valve - Durable & Efficient Manufacturer, Factories
Explore Specifications
Executive Engineering Whitepaper
Domestic Application Globe Valves: Next-Generation Engineering Architecture
Analyzing the pivotal shift from rudimentary isolation stopcocks to precision-throttled, CE-certified domestic globe valve assemblies in municipal residential infrastructure.
Strategic Role in High-Density Residential & Light Commercial Infrastructure
In municipal residential architecture, district heating substations, and domestic hot water (DHW) recirculating networks, fluid control dynamics have transcended simplistic on/off isolation. Modern smart buildings demand linear throttling, acoustic cavitation dampening, and rigorous compliance with the European Union's Pressure Equipment Directive (PED 2014/68/EU). Domestic application globe valves provide an S-shaped internal flow geometry that enforces linear volumetric control, safeguarding high-pressure domestic risers against cavitation noise, water hammer shockwaves, and localized seat erosion.
Historically, low-cost gate or ball valves were erroneously deployed in domestic throttling scenarios, yielding catastrophic wire-drawing across seat rings, chronic turbulence, and rapid cavitation at low opening percentages. Contemporary mechanical engineering specifications mandate resilient-seated and precision-ground parabolic plug globe valves conforming to EN 13709, EN 12516, and BS 5154. These valves maintain continuous acoustic silence under high differential pressures (ΔP > 1.5 bar) while ensuring zero micro-leakage at operational shutoff.
- Cavitation Suppression Design: Contoured parabolic plugs dissipate hydraulic kinetic energy smoothly across tortuous paths.
- Micro-Fine Linear Flow Balancing: High stem-thread pitch enables millimeter-scale stroke calibration for hydraulic balancing.
- Acoustic Decoupling: Heavy ductile iron (EN-GJS-450-10) and bronze alloys dampen pipeline vibration below 25 dB(A).
- Hygienic Potable Water Integrity: Lead-free metallurgy and WRAS-approved EPDM/PTFE trim eliminate secondary water contamination.
1996*
Valve Foundry & Machining Origin
100%
Hydrostatic Shell & Seat Test Rate
50+
Global Export Countries Served
0.0
ISO 5208 Rate A Bubble-Tight Leakage
Procurement Engineering
Global Enterprise Sourcing Criteria for CE-Marked Globe Valves
Navigating the exacting metallurgical, hydraulic, and environmental compliance frameworks mandated by tier-one EPC contractors and municipal water boards across Europe and the Americas.
PED 2014/68/EU Module H Conformity
Global EPC buyers strictly audit CE conformity under the European Pressure Equipment Directive. We maintain full traceability from molten charge spectral analysis to certified hydrostatic testing under Module H (Full Quality Assurance), verifying sound engineering practice and safety under fluctuating thermal pressures.
EN 10204 3.1 MTR
Notified Body Audited
Cat I to III Fluid Groups
Potable Water Hygiene & WRAS/NSF
For domestic drinking water loops, procurement protocols demand materials entirely free from toxic element leaching. Valve trim components utilize WRAS-certified non-cytotoxic EPDM, high-grade PTFE, and low-lead dezincification-resistant brass/bronze alloys (CW602N / CC491K) to resist Legionella biofilm formation.
BS 6920 Toxic Extraction
Low-Lead Bronze
Anti-Microbial Polish
Hydraulic Cavitation & Noise Limits
European building codes (such as DIN 4109) specify stringent domestic plumbing acoustic thresholds (≤30 dBA). Sourcing specifications evaluate globe valve parabolic plug designs, verifying cavitation indexes (σ) and Reynolds stability across high dynamic flow velocities up to 3.5 m/s.
DIN 4109 Class I Noise
Linear Kv Profile
Anti-Chatter Stem Guide
Supply Chain Resilience
China Factory 4.0: Integrated Foundry, Elastomers & CNC Synergy
How complete campus-level vertical integration at Tianjin Top Valve eliminates quality blindspots and streamlines lead times for international distributors.
Eliminating Supplier Gaps Through Decades of Foundry & Rubber Synthesis
Unlike asset-light trading companies or mere assembly workshops, Tianjin Top Valve operates from deep industrial roots dating back to Tianjin Dongfang Rubber Factory (founded in 1987) and Tianjin Donglian Valve Factory (founded in 1996). Spanning a 23,000 m² state-of-the-art manufacturing campus in Wuxia Industrial Park, Dongli District, Tianjin, our vertically integrated infrastructure controls the entire production cycle:
| Process Stage | In-House Production Infrastructure | Quality Assurance Control Point | Engineering Benefit to Buyer |
|---|---|---|---|
| 1. Metallurgical Casting | Automated green-sand molding & induction melting furnaces | Optical emission spectrometry & ultrasonic flaw testing | Homogeneous grain structure, zero micro-porosity, high yield strength. |
| 2. Elastomer Compounding | Internal rubber plant (Est. 1987) compounding EPDM, NBR & FKM | Rheometer cure tracking, tensile testing & compression set verification | Superior sealing resilience, longevity under hot water thermal cycles up to 130°C. |
| 3. CNC Precision Machining | Multi-axis CNC turning and horizontal milling centers | CMM coordinate measuring machines, Ra 0.4 μm stem finish | Minimal operating torque, zero thread chattering, precise valve seat alignment. |
| 4. Pressure Testing & Assembly | Computerized hydrostatic shell & seat testing rigs | 100% individual valve testing at 1.5x PN (Shell) & 1.1x PN (Seat) | Guaranteed Zero Leakage (ISO 5208 Rate A) with verifiable batch MTR certificates. |
Application Engineering
Localized Application Scenarios in Modern Building Services
From subterranean district heat exchanges to penthouse domestic booster loops: engineered fluid control where reliability is mission-critical.
Domestic Hot Water (DHW) Return Balancing
Continuous hot water return loops require constant micro-throttling to maintain thermal equilibrium and suppress Legionella growth without eroding valve discs. Parabolic-plug bronze globe valves maintain precision Kv settings over decades of uninterrupted service.
High-Rise Residential Riser Isolation
In multi-story residential towers, static head pressures at base risers frequently exceed 16 bar. CE-marked PN25 ductile iron globe valves provide safe, controlled isolation during maintenance without triggering devastating dynamic pressure spikes across plumbing branch circuits.
Secondary HVAC Chilled & Heating Loops
Installed at secondary building heat exchangers, domestic globe valves enable manual hydraulic tuning across fan coil units (FCU) and hydronic underfloor heating manifolds, eliminating noisy imbalances and reducing variable-speed circulator pump electrical consumption.
Engineering Data Matrix
Standard CE Domestic Application Globe Valve Parameters
Comprehensive design standards, pressure classes, material chemistry, and connection standards for engineering specifications.
| Technical Parameter | Specification Range | Reference International Standard |
|---|---|---|
| Nominal Diameters (DN) | DN15 to DN200 (1/2" to 8" Nominal Bore) | EN ISO 6708 / DIN 2501 |
| Pressure Ratings (PN) | PN10, PN16, PN25, Class 125, Class 150 | EN 1333 / ASME B16.34 |
| Body & Bonnet Materials | Ductile Iron (EN-GJS-450-10 / 500-7), Bronze (CC491K), Cast Steel (1.0619 / WCB), SS304/SS316 | EN 1563 / EN 1982 / ASTM A216 / A351 |
| Disc / Plug Profile | Parabolic Throttling Plug, Flat Face Sealing Disc, Needle Disc for Micro-Metering | EN 13709 / BS 5154 |
| Stem Metallurgy | Stainless Steel (X20Cr13 / 1.4021 / AISI 410, AISI 304, AISI 316) Precision Ground | EN 10088-3 |
| Seat Rings | Integral Bronze, SS304/SS316 Overlay, Resilient WRAS-Approved EPDM, PTFE Clad | EN 12266-1 Rate A / ISO 5208 |
| End Connections | Flanged (EN 1092-2, ASME B16.5), Threaded Female BSPP / BSPT (ISO 7-1), NPT | EN 558 Series 1 / DIN 3202-F1 |
| Operating Temperature | -10°C to +130°C (EPDM Soft Seat) | -20°C to +200°C (PTFE / Metallic Seat) | PED 2014/68/EU Thermal Range |
| Hydrostatic Testing | Shell Test: 1.5 × PN | Seat Leakage Test: 1.1 × PN (Zero Bubble Leakage) | EN 12266-1 / API 598 |
Technical Knowledge Base
Engineering Q&A: Domestic Application Globe Valves
Detailed technical explanations resolving critical engineering inquiries from project consultants, valve distributors, and piping procurement managers.
Why are globe valves preferred over ball or gate valves for domestic throttling and balancing?
Ball valves feature a non-linear flow characteristic: opening the quarter-turn ball by just 15% exposes nearly 40% of full Kv capacity, causing extreme fluid velocity, acoustic whistling, and severe cavitation across the downstream PTFE seat edge. Gate valves are strictly designed for full on/off isolation; partially open wedges flutter in the fluid stream, leading to chatter, seat wear, and early failure. In contrast, globe valves move perpendicular to flow, providing a proportional, linear relationship between handwheel rotations and orifice area. This allows stable, acoustic-dampened flow modulation without mechanical chatter.
What exact certifications verify that your globe valves conform to European CE standards?
Our domestic application globe valves comply with the Pressure Equipment Directive (PED) 2014/68/EU under certified quality assurance modules. Valves exceeding DN25 or PS>0.5 bar carry our CE Mark with Notified Body identification. Metallurgical chemistry and physical properties are documented via EN 10204 Type 3.1 Material Test Reports (MTR). Additionally, our factories maintain ISO 9001:2015, ISO 14001:2015, and ISO 45001:2018 certifications, backed by WRAS material declarations for potable water contact.
How does your in-house rubber factory (since 1987) ensure longer valve seal life?
The elastomer seal is typically the primary point of failure in resilient-seated valves under constant thermal cycling. Because we compound and vulcanize our own rubber via Tianjin Dongfang Rubber Factory (operating within our group since 1987), we control polymer formulation, curing curves, and anti-aging additives in-house. Our EPDM seals exhibit low compression set (≤18% after 1000 hrs at 100°C) and resist chloramine oxidation, preventing premature embrittlement, swelling, or seat bypass.
What are the acoustic advantages of domestic globe valves under DIN 4109 noise regulations?
Under Germany's DIN 4109 and European acoustic standards, water installation noise in domestic living spaces cannot exceed 30 dB(A). Cheap valves create turbulent vortices that resonate through structural concrete. Our globe valves feature hydrodynamic internal water-ways with enlarged bonnet cavities and parabolic plugs. By staging pressure drops through gradual annular expansion, fluid velocity is kept subsonic and laminar, keeping operational noise well within acoustic Class I compliance.
Can Tianjin Top Valve manufacture customized flange drilling and face-to-face dimensions?
Yes. Our multi-axis CNC machining centers can machine flange drillings to EN 1092-2 PN10/PN16/PN25, ASME B16.5 Class 125/150, BS 10 Tables D/E, and JIS B2239 10K/16K. Standard face-to-face dimensions follow EN 558 Series 1 (DIN 3202-F1), with customized retrofitting dimensions available for municipal modernization projects upon review of engineering drawings.
What packaging protocols protect valve finishes and seals during intercontinental shipping?
Export valves undergo a multi-tier protective packaging sequence: end ports receive polyethylene push-in flange protectors; machined stem threads are coated with corrosion-inhibiting wax; valve bodies are sealed in moisture-barrier bubble bags; and assemblies are secured within ISPM-15 heat-treated fumigated wooden crates with internal steel banding to guarantee pristine delivery across extended sea freight transits.
Quality Tested Industrial Series
Certified Flow Control & Check Valve Inventory (Showcase II)
Certified products manufactured with traceable in-house casting and rubber bonding. Retained original production inventory ready for EPC project integration.

CE Certification Compact Low-Pressure Drop Wafer Lift Check Valve Supplier, Factories
Explore Specifications
High-Quality WRAS Approved Butterfly Valve - High Performance & Durability 4020L Supplier, Manufacturers
Explore Specifications
Wholesale Lugless Semi-Shaft Wafer Butterfly Valve - Durable & Reliable Manufacturer, Factory
Explore Specifications
Wholesale Wafer Butterfly Valve - Durable & Efficient Flow Control Solution Suppliers, Factory
Explore Specifications
High-Quality PTFE Lined Pinless Butterfly Valve Supplier, Factories
Explore Specifications
High-Quality Rubber Lined Pinless Butterfly Valve Supplier, Factories
Explore Specifications
CE Certification Stainless Steel Single Disc Wafer Check Valve with Enhanced Corrosion Supplier, Manufacturers
Explore Specifications
CE Certification Quick - Opening Three - Way Flange Ball Valve for Emergency Fluid Diversion Supplier, Factory
Explore Specifications
Tianjin Engineering & Sourcing Consultation
Specifying Valves for Critical EPC or Municipal Infrastructure?
Engage directly with our senior valve engineering staff at Tianjin Top Automation Equipment Co., Ltd. Located in Zone A, Wuxia Industrial Park, Dongli District, Tianjin, China, our team delivers certified dimensional schematics, 3D CAD/BIM model libraries, and material test protocols tailored to your pressure, temperature, and media specifications.
