

Precision Hydrodynamics
Engineered Grooved & Specialized Industrial Valves
Explore Tianjin Top Valve's high-integrity portfolio designed for mechanical piping, severe HVAC, chemical containment, and pressurized distribution grids.
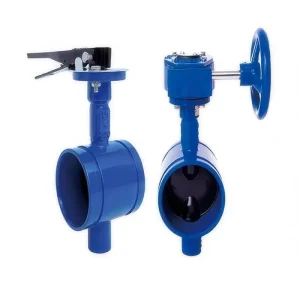
High-Quality Grooved End Butterfly Valve - Durable & Reliable Flow Control Suppliers, Supplier
Technical Specs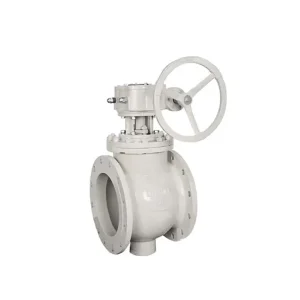
CE Certification High - Pressure Eccentric Plug Valve for Oil and Gas Supplier, Manufacturer
Technical Specs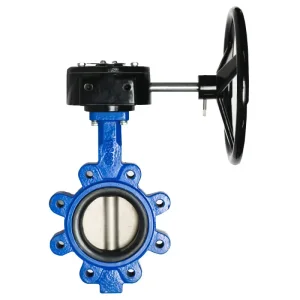
High-Quality Lug type Butterfly valve Suppliers, Manufacturers
Technical Specs
CE Certification WRAS Approved High-Performance Butterfly Valve 4020G Manufacturer, Factories
Technical Specs
CE Certification Flanged Butterfly Valve - Durable & Efficient Flow Control Suppliers, Supplier
Technical Specs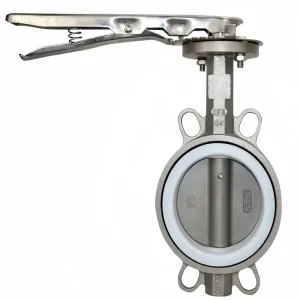
CE Certification PTFE Lined Stainless Steel Butterfly Valve Manufacturer, Factory
Technical Specs
Wholesale PTFE Lined Cast Body Butterfly Valve Suppliers, Factory
Technical Specs
Technical Whitepaper: Flow Mechanics
Engineering Superiority in Grooved Mechanical Piping Systems
An in-depth metallurgical and mechanical analysis of grooved end butterfly valve architectures versus traditional bolted flange connections in contemporary mission-critical piping.
68%
Faster Installation Rate
300 PSI
Continuous Rated Pressure
Zero
Stem Leakage Path via O-Rings
100%
In-House Hydrostatic Testing
Stress Dissipation & Dynamic Damping
Grooved couplings absorb linear thermal expansion, contraction, and seismic deflections. By distributing bending moments across the entire circumferential housing groove, the valve eliminates stress localization that typically compromises traditional flanged neck seals.
Fully Encapsulated Disc Sealing
Our discs are cast from ductile iron (ASTM A536 65-45-12) and encapsulated in cross-linked EPDM or synthetic NBR formulated inside our dedicated rubber plant (operational since 1987). This guarantees low closure torque, high resilience, and zero seat delamination.
Optimized Fluid Hydrodynamics
The hydrodynamic disc profile decreases turbulent boundary layer formation and reduces flow coefficient (Cv) resistance. By narrowing the disc center profile while maintaining high torsional rigidity via 416/304 stainless steel splined stems, pump operating heads are conserved.
Information Gain Highlight: Unlike conventional wafer valves prone to flange bolt relaxation and torque imbalances, grooved-end valves employ self-aligning mechanical couplings. This physical coupling prevents pipeline misalignments, prevents disc impingement against pipe inner diameters, and reduces installation labor by more than 60% across commercial HVAC risers and industrial loops.
Macro-Infrastructure Deployment
Global Industrial Architecture & System Solutions
Procurement teams and mechanical engineering consultants worldwide specify our grooved butterfly valves across diverse industrial paradigms.
NFPA Fire Protection Loops
Certified for automated fire sprinkler arrays, standpipes, and deluge systems. Outfitted with indoor/outdoor rated supervisory tamper switches to interface seamlessly with building fire alarm panels for open/closed state monitoring.
Hyperscale Data Center HVAC
Critical chilled water cooling systems require zero downtime and rapid modular scalability. Grooved butterfly valves allow rapid spool changes, valve isolation, and vibration dampening near primary variable-speed chiller pumps.
Municipal Desalination & Water
Available with high-nickel aluminum bronze disc castings and certified WRAS/NSF elastomers. Resists cavitation and localized pitting in reverse osmosis brine headers and potable water arterial conduits.
Mining Tailings & Slurry Transport
Engineered rubber formulations and reinforced cast bodies withstand high-abrasion, low-solids slurries without carcass erosion, extending turnaround intervals in aggressive processing sites.
Design Compliance
Technical Specification & Standard Cross-Reference
Direct from Tianjin Top Valve's engineering department. Standard configurations and customization parameters for engineering submittals.
| Engineering Parameter | Standard Specification | High-Performance / Corrosive Options | Governing Norm |
|---|---|---|---|
| Nominal Sizing | DN50 – DN300 (2" – 12") Standard | DN350 – DN600 (14" – 24") Heavy Pattern | AWWA C606 / ISO 6182 |
| Working Pressure | PN16 / PN20 / PN25 (175–300 PSI) | Class 250 / High-pressure test up to 350 PSI | EN 12266-1 / API 598 |
| Casting Metallurgy | Ductile Iron ASTM A536 Gr. 65-45-12 | WCB Cast Steel / CF8M 316 Stainless / Al-Bronze | EN 1563 / ASTM A536 |
| Disc Encapsulation | Direct Moulded EPDM (Potable Safe) | NBR (Hydrocarbons) / High-Temp FKM / PTFE | WRAS / FDA 21 CFR 177.2600 |
| Stem Metallurgy | SS416 / SS420 Hardened Hex/Double-D | SS304 / SS316 / 17-4PH Monel Alloys | ASTM A276 / EN 10088 |
| Surface Protection | Fusion Bonded Epoxy (FBE) ≥250μm | Rilsan Polyamide / High-Build Polyurethane | DIN 30677-2 / AWWA C550 |
Factory Direct Verification
In-House Vertical Integration: Foundry to Rubber Vulcanization
Tianjin Top Automation Equipment Co., Ltd. (operating Donglian Valve Factory since 1996 and Dongfang Rubber Factory since 1987) provides unmatched quality assurance that trading agents cannot duplicate.
Direct Metallurgical Control
Our dedicated foundry formulates ductile iron melts under continuous optical emission spectrometry. Every ladle is analyzed for nodularity percentage, tensile strength, and elongation before pouring, preventing casting pinholes and porosity defects.
Proprietary Elastomer Synthesis
The sealing seat is the primary failure vector in quarter-turn valves. Since 1987, our internal rubber facility mixes virgin polymers, controlling rheology, crosslink density, and compression sets. Result: WRAS-compliant potable seals with verified zero-odor and zero-taste alteration.
100% Dual-Direction Pressure Proof
No statistical batch sampling. Every assembled grooved butterfly valve undergoes dual-direction pneumatic low-pressure bubble testing (6 bar) and hydrostatic shell testing (1.5x PN rating) in accordance with ISO 5208 and EN 12266 before packaging.
Innovation Horizon
Engineering Roadmap: Digitalization & Advanced Actuation
Our R&D engineers are driving modernization in pipeline flow monitoring, sustainable materials, and smart facility integration.
Phase 1: Real-Time
Integrated IoT Sensor Hubs
Development of gear operators embedded with low-power wireless torque and vibration sensors to forecast elastomer degradation and pipeline hammer in municipal pump stations.
Phase 2: Tribology
Nano-Composite Discs
Integrating synthetic diamond-like coatings (DLC) on stainless stems and PTFE encapsulations to eliminate friction wear in aggressive chemical recovery lines.
Phase 3: Footprint
Ultra-Lightweight Compact Ductile
Finite element analysis (FEA) disc optimization achieving up to 18% weight reduction without reducing structural body yield strength under cyclic thermal shock.
Phase 4: Green Foundry
Zero-Carbon Casting Facilities
Implementing 100% electric induction smelting systems coupled with closed-loop reclaimed sand casting systems to achieve verified ISO 14064 carbon neutrality compliance.
Comprehensive Catalog
Explore Complementary Industrial Flow Control Units
Factory-tested check, butterfly, and specialized valves engineered to complement grooved installations in large-scale piping designs.
High-Quality PTFE Lined Pinless Butterfly Valve Supplier, Factories
Technical Specs
High-Quality WRAS Approved Butterfly Valve - High Performance & Durability 4020L Supplier, Manufacturers
Technical Specs
High-Quality High - Performance Silent Check Valve for Water Supply Systems Supplier, Manufacturers
Technical Specs
CE Certification Water-Safe Butterfly Valve for Efficient Flow Control Manufacturers, Manufacturer
Technical Specs
High-Quality Actuator Wafer Butterfly Valve Supplier, Manufacturers
Technical Specs
CE Certification Compact Low-Pressure Drop Wafer Lift Check Valve Supplier, Factories
Technical Specs
Wholesale Wafer Butterfly Valve - Durable & Efficient Flow Control Solution Suppliers, Factory
Technical Specs
CE Certification Micro-Resistance Ball Check Valve Manufacturers, Factories
Technical Specs
Technical Clarifications
Frequently Asked Questions: Grooved End Butterfly Valves
Direct technical explanations authored by our chief mechanical engineering staff to guide procurement specifications and pipeline design.
What are the key technical advantages of Grooved End Butterfly Valves over Flanged or Wafer valves?
Grooved end butterfly valves connect via standard mechanical couplings (such as Victaulic-compatible grooved joints) rather than through-bolts or welded flanges. This delivers three core advantages: (1) Speed: Installation time is reduced by up to 68% as only two bolts need to be torqued compared to 8 to 16 bolts per flanged connection. (2) Self-Centering: The coupling collar aligns the valve disc concentric with the pipe bore, eliminating the risk of disc interference with the pipe interior. (3) Stress Dissipation: The mechanical engagement accommodates thermal expansion, structural settlement, and vibration without cracking flanges or pinching elastomer liners.
Can Tianjin Top Valve manufacture grooved valves conforming to international roll-groove and cut-groove standards?
Yes. Our CNC machining operations finish grooved ends in strict compliance with AWWA C606 (standard roll and cut groove dimensions) and ISO 6182. Whether your pipe schedule is Schedule 10, Schedule 40 thin-wall carbon steel, stainless steel, or ductile iron IPS dimensions, our precision tolerances guarantee exact gasket seating depth, groove diameter, and groove width for bubble-tight performance up to 300 PSI (PN20/PN25).
How does in-house rubber compounding protect against long-term seat degradation?
Unlike many assemblers who purchase commercial-grade vulcanized rubber rings from third-party vendors, Tianjin Top Valve operates Tianjin Dongfang Rubber Factory (established 1987). We formulate and compound our own raw EPDM, NBR, and fluoroelastomers with proprietary anti-aging and anti-ozone agents. This yields superior compression set resistance (≤18% after 1,000 hours at 100°C) and ensures that when the disc seals against the encapsulated body, the elastomer retains its elasticity through tens of thousands of cycles without hardening or peeling.
Are your grooved butterfly valves approved for municipal potable water supply?
Yes. We produce models that are certified by the UK's Water Regulations Approval Scheme (WRAS) and compliant with international potable water hygiene standards. Our EPDM formulation undergoes rigorous migration and microbiological testing to ensure zero extraction of heavy metals, cytotoxic compounds, or odor into drinking water distribution systems.
What operator configurations are available for automated systems?
Our grooved butterfly valves feature an ISO 5211 top mounting flange with double-D or keyed shaft arrangements. We supply valves with: (1) 10-position detent levers with locking mechanisms, (2) Heavy-duty worm gearboxes with handwheel and visual position indicators, (3) Dual internal tamper monitoring switches for fire-fighting monitoring, and (4) Direct-mount 24V/110V/220V electric actuators or rack-and-pinion pneumatic actuators with 4-20mA smart positioners for continuous modulation.
How does your factory handle quality tracing and material test certificates?
Every casting poured in our group foundry receives an indelible heat heat-number marking. All finished valves ship with comprehensive EN 10204 Type 3.1 inspection certificates documenting chemical spectrometry analysis (C, Si, Mn, P, S, Mg), mechanical pull tests (tensile yield and elongation), hydrostatic shell test logs, and rubber cure lot tracing. Complete QA files are archived digitally for 10 years to support institutional plant audits.
