
Precision Engineered Flow Control & Isolation Portfolio
Explore our factory-direct severe-service globe, butterfly, and specialized process valves precision-machined in Tianjin, China for global EPC contractors, energy infrastructure, and industrial OEMs.
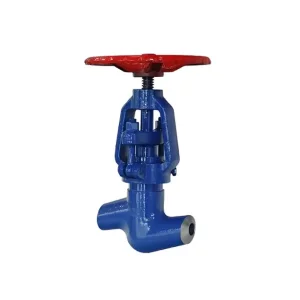
High-Quality High Temperature And High Pressure Power Station Globe Valve Manufacturers, Manufacturer
View Technical Specifications
High-Quality High - Temperature - Vacuum Isolation Globe Valve for Vacuum Heat Suppliers, Factory
View Technical Specifications
Wholesale Straight-Through Ammonia Globe Valve Manufacturers, Factory
View Technical Specifications
High-Quality Water Seal Globe Valve with Quick - Closing Feature Manufacturers, Manufacturer
View Technical Specifications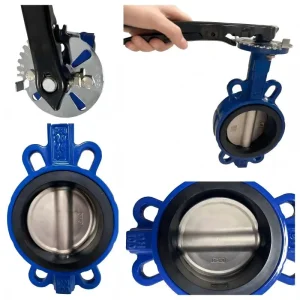
High-Quality WRAS Approved Butterfly Valve - High Performance & Durability 4020L Supplier, Manufacturers
View Technical Specifications
Wholesale Straight-Through Ammonia Globe Valve Manufacturers, Factory
View Technical Specifications
High-Quality EPDM Lining Butterfly Valve - Durable & Corrosion Resistant Suppliers, Manufacturers
View Technical Specifications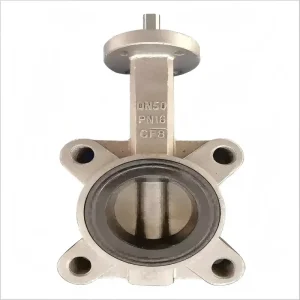
Wholesale Semi Lug Butterfly Valve - Durable & Versatile Flow Control Manufacturers, Manufacturer
View Technical SpecificationsThe Global Severe-Service Fluid Control Landscape & Engineering Imperatives
A technical assessment of modern globe valve operation across supercritical energy complexes, cryogenic refrigeration lines, and high-pressure chemical synthesis plants.
Supercritical Thermal & Nuclear Steam
Modern thermal units operate under superheated steam parameters exceeding 560°C and 25 MPa. Standard gate valves suffer from wire-drawing and seat galling under high differential pressure throttling. Industrial power station globe valves engineered with Stellited seating and pressure-seal bonnets provide the only reliable zero-leakage throttling boundary.
Cryogenic Ammonia & Chemical Refrigeration
Anhydrous ammonia (NH3) transport demands hermetic containment to prevent toxic atmospheric release and system freezing. Standard soft-seated valves fail due to elastomer embrittlement. Straight-through ammonia globe valves equipped with extended stem hoods, back-seating safety mechanics, and PTFE/bellows dual-barrier seals eliminate fugitive emissions entirely.
Deep Vacuum Thermal Processing
Semiconductor crystal growth, vacuum annealing, and aerospace thermal chambers operate down to 10⁻⁴ Pa. Conventional valves experience atmospheric back-diffusion through packing glands. Water-sealed and vacuum-isolation globe valves create a micro-barrier fluid seal around the packing box, halting air ingress and maintaining chamber equilibrium.
China Factory Integration & Supply Chain Resilience: The Tianjin Foundry Advantage
Why Tier-1 EPC contractors select our vertically integrated manufacturing complex over fragmented assembly workshops.
In-House Casting Foundry Since 1996
By operating Tianjin Donglian Valve Factory, we eliminate external foundry markups and raw casting delays. Induction melting furnaces produce ductile iron, WCB, CF8M, and WC9 alloy castings with continuous optical emission spectrometry validation.
Proprietary Rubber Seat Plant Since 1987
Operating Tianjin Dongfang Rubber Factory allows internal compound vulcanization of EPDM, NBR, Viton, and PTFE seats. Complete formulation control ensures minimal compression set and flawless resilience over thousands of duty cycles.
High-Precision CNC Machining Centers
Multi-axis horizontal and vertical CNC machining centers ensure concentricity between valve seat, stem guide, and disc face within 0.005mm tolerance, eliminating micro-clearance leakage under high mechanical stresses.
Tianjin Port Logistics Synergy
Located in the Wuxia Industrial Park, Dongli District, our 23,000 m² campus is only 40 km from Tianjin Port. Direct container dispatch reduces inland freight lead-times and ensures uncompromised export timelines to over 50 countries.
Globe Valve Trim Architecture, Standards & Operational Envelopes
Comprehensive metallurgical matrix and construction standards for industrial project specification.
| Valve Type / Class | Design & Testing Norms | Shell / Body Metallurgy | Disc & Seat Trim | Sealing Architecture | Primary Industrial Application |
|---|---|---|---|---|---|
| Power Station Globe Valve (PN160 - PN420 / Cl. 900-2500) | ASME B16.34, API 623, BS 1873, GB/T 12235 | ASTM A217 WC6, WC9, C12A, WCB | HF Stellite No.6 Overlay / Cobalt-Free Hardfacing | Pressure-seal bonnet with pure flexible graphite & braided rings | Thermal boiler feedwater isolation, main steam throttle, turbine bypass systems. |
| Straight-Through Ammonia Globe Valve (PN25 - PN40) | DIN EN 13709, EN 12266-1, API 602 | ASTM A352 LCC, LCB, Cast Steel WCB | PTFE Soft Insert + Stainless Steel 304/316 Metal Seat | Dual O-ring + back-seating + live-loaded PTFE packing | Industrial cold storage, anhydrous ammonia (NH3) piping, fertilizer plants. |
| Vacuum Isolation & Heat-Seal Globe Valve (PN16 - PN64) | JB/T 4065, ASME B16.34, EN 1092-1 | Carbon Steel WCB, Stainless Steel 304/316 | Chrome-nickel stainless steel + resilient fluoropolymer | Hydro-barrier water ring chamber + bellows seal option | Vacuum heat furnaces, polysilicon CVD reactors, thermal condensation plants. |
| Water Seal Quick-Closing Globe Valve (PN16 - PN25) | GB/T 12235, BS 1873, ISO 5208 | Ductile Iron QT450-10, Cast Steel WCB | Bronze / 2Cr13 Stainless Steel Trim | Water injection cavity seal + internal high-torque counterweight spring | Emergency pump protection, circulating water networks, cooling towers. |
| Corrosive Process Globe Valve (Class 150 - 300) | API 623, ASME B16.34, MSS SP-144 | ASTM A351 CF8M, CF3M, Hastelloy C276 | Solid Alloy 20, Duplex 2205, Monel 400 | Inconel multi-ply bellows seal + Class AH secondary packing | Chemical chlorination units, sulfur recovery, aggressive acid processing. |
Severe-Service Operating Scenarios & Root-Cause Failure Prevention
How specialized globe valve geometries overcome cavitation, turbulent erosion, and micro-channel leakage.
Cavitation Elimination in Boiler Feedwater
When high-pressure water drops below vapor pressure across conventional seats, imploding vapor cavities destroy downstream piping. Our multi-stage tortuous-path cage trims divide pressure drop into non-critical micro-increments, guaranteeing fluid remains in the single-phase liquid envelope.
Aerodynamic Noise & High-Velocity Steam
Supercritical steam expansion across high-drop letdown stations generates destructive acoustic vibration exceeding 110 dBA. Our perforated drilled-hole disc trims attenuate sound waves via acoustic frequency shifting and turbulent kinetic energy dissipation.
Thermal Shock Resistance in Cyclic Service
Frequent plant startup/shutdown causes differential thermal expansion between stem, bonnet, and body. Pressure-seal bonnets leverage internal system pressure to tighten sealing wedge rings, preventing thermal transient weeping common in bolted bonnets.
Technological Roadmap: The Evolution of Intelligent Flow Regulation
Next-generation valve innovations transforming conventional mechanical valves into digital asset nodes.
IIoT Smart Diagnostics & Acoustic Sensing
Integration of wireless piezo-electric acoustic emission sensors within the valve bonnet to detect internal ultrasonic cavitation signatures and packing gland micro-leakage before external loss-of-containment occurs.
Additive Manufactured Multi-Stage Trims
Laser Powder Bed Fusion (LPBF) 3D printing enables flow passage geometries previously impossible via casting or milling. Micro-channel helical trims eliminate vortex-induced cavitation while reducing valve trim weight by 45%.
Fugitive Emissions: Zero-Methane Compliance
As environmental protocols mandate sub-20 ppm fugitive emissions for carbon capture (CCUS) and clean hydrogen pipelines, our dual-barrier welded Inconel bellows seals eliminate dynamic packing interfaces entirely.
Global Project Standards, Third-Party Audits & Field Engineering Support
Uncompromising compliance documentation and engineering assistance for critical pipeline infrastructure.
EN 10204 3.1 & 3.2 Material Traceability
Every critical cast and forged component carries a permanent heat number stamped directly onto the valve body. Full chemical composition, tensile strength, Charpy V-notch impact testing, and hardness reports are delivered with every consignment.
Non-Destructive Examination (NDE) Rigor
In-house ASNT Level II certified technicians perform 100% Radiographic Testing (RT) on high-pressure castings, Liquid Penetrant Testing (PT) on Stellite hardfacing weld overlays, and Magnetic Particle Testing (MT) on valve stems.
Global Field Engineering & Fast Spares
Our application engineers assist EPC contractors across North America, Europe, the Middle East, and Southeast Asia. Standard valve trim components, bonnet gaskets, and spare stems are stocked for rapid air-freight dispatch within 48 hours.
Frequently Asked Questions: Industrial Globe Valve Engineering
Detailed technical answers to common engineering, procurement, and pipeline operational inquiries.
What are the key technical differences between globe valves and gate valves for process isolation? +
When should fluid flow be directed "Under the Seat" vs. "Over the Seat" in globe valves? +
How does your factory prevent fugitive emissions in hazardous ammonia (NH3) service? +
What is the function of a water-seal bonnet in vacuum isolation globe valves? +
What hardfacing alloys are used on high-pressure power station globe valve trims? +
How does Tianjin Top Valve support custom OEM and EPC specification requirements? +
Integrated Flow Control Solutions: Check, Plug & Butterfly Series
Complete pipeline project support featuring our factory-direct check valves, eccentric plug valves, and resilient seated gate valves engineered to global industrial standards.

Wholesale Single Flange Butterfly Valve - Durable & Efficient Flow Control Supplier, Manufacturers
View Technical Specifications
CE Certification High - Pressure Eccentric Plug Valve for Oil and Gas Supplier, Manufacturer
View Technical Specifications
High-Quality High-Quality Wafer Check Valve for Secure Fluid Control Suppliers, Factories
View Technical Specifications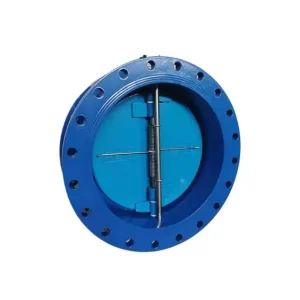
Wholesale Dual Plate Flange Type Check Valve Factories, Factory
View Technical Specifications
Wholesale PTFE Lined Butterfly Valve - Durable & Corrosion Resistant Manufacturers, Manufacturer
View Technical Specifications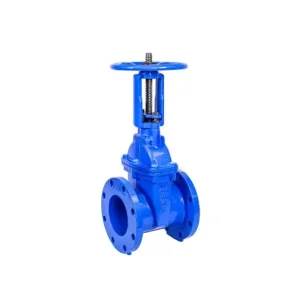
Wholesale Rising Stem Resilient Seat Gate Valve Supplier, Factory
View Technical Specifications
High-Quality Grooved Type Manual Butterfly Valve Suppliers, Manufacturers
View Technical Specifications
