

Industrial Engineering Technical Whitepaper & Catalog

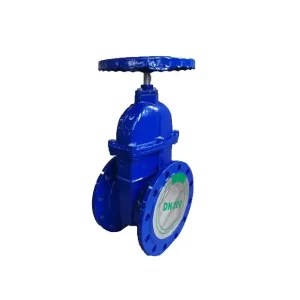
CE Certification Non-rising gate valve Manufacturers & Manufacturer

Direct-from-foundry engineering, precision elastomeric vulcanization, and EN 1171 / DIN 3352 pressure-tested flow infrastructure by Tianjin Top Valve.

PED 2014/68/EU Module H Direct Casting Foundry (Est. 1996) Exported to 50+ Nations
Primary Catalog Portfolio

Featured Fluid Isolation & Flow Infrastructure Hardware

Factory-direct delivery straight from our integrated Tianjin manufacturing complex. Fully verified for leakage prevention, low drive torques, and sustained cycle lifespans.

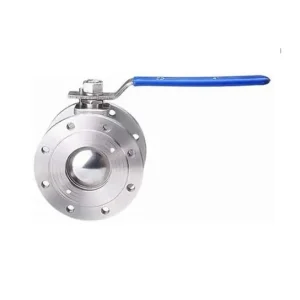
Wholesale Stainless Steel Ultra - Thin Ball Valve

Wholesale Stainless Steel Ultra - Thin Ball Valve with Fire - Safe Design

View Specification
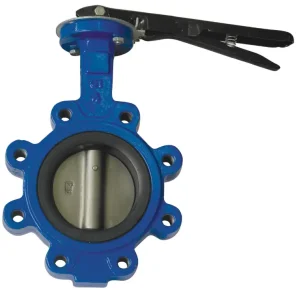
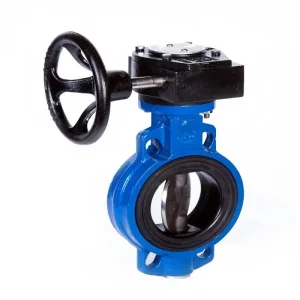
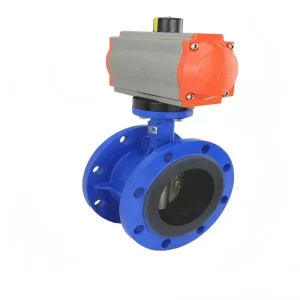
High-Quality Pneumatic Butterfly Valve Reliable Flow Control

High-Quality Pneumatic Butterfly Valve - Reliable Flow Control Solution

View Specification
E-E-A-T Manufacturing Authority

Why Global EPC Leaders Partner with Chinese NRS Valve Manufacturers

Vertical supply chain integration eliminates casting micro-porosities, mitigates rubber degradation, and delivers unmatched cost-performance resilience.

Foundry-Level In-House Metallurgy

Unlike assembling workshops that source unverified commercial iron from external brokers, Tianjin Top Valve operates its proprietary casting foundry established in 1996. We perform strict spectroscopic spectral analysis on Ductile Iron (EN-GJS-450-10 / EN-GJS-500-7) to guarantee tensile strength above 450 MPa and elongation exceeding 10%.

In-House Elastomeric Compounding

Leveraging our dedicated rubber division (Tianjin Dongfang Rubber Factory, operating continuously since 1987), we custom compound high-density EPDM and NBR liners. Our proprietary rubber curing prevents vulcanization blistering, achieves zero compression-set drift, and maintains WRAS-compliant potable water purity over decades of operational service.

Precision CNC Broaching & Stems

Non-Rising Stem (NRS) valves rely entirely on internal stem nut engagement. We precision machine cold-rolled Stainless Steel (SS304/SS316/SS420) and high-tensile brass stem nuts with automated multi-axis thread chasing, cutting operational torque by 35% while eliminating galling hazards common to sub-standard alloys.

Engineering Deep Dive

Non-Rising Stem (NRS) Gate Valves: Structural Architecture

A critical technical assessment of internal mechanics, CE compliance matrices, and why NRS gate valves are chosen for congested subterranean and marine utility routing.

In contrast to Outside Screw & Yoke (OS&Y) rising stem configurations, Non-Rising Stem (NRS) resilient seated gate valves operate by rotating the stem within the stationary thrust collar, translating the internal encapsulated wedge linearly along an internal trapezoidal spindle nut. This spatial conservation renders NRS models mandatory in municipal tunnel conduits, buried pipeline installations with road access boxes, shipboard engine bilge spaces, and compact pumping vault configurations where vertical headroom is severely limited.


Engineering Parameter EN 1171 / DIN 3352 Standard Tianjin Top Valve CE NRS Spec Procurement Advantage
Pressure Rating Class PN10 / PN16 / PN25 Shell: 1.5× PN; Seat: 1.1× PN (Bi-directional) Zero Bubble Leakage Rate A
Face-to-Face Standard EN 558 Series 14 (DIN F4) / Series 15 (DIN F5) Interchangeable Drop-in Replacement Standardized retrofitting across global pipework
Stem Sealing Mechanics Gland packing or elastomeric rings Triple O-Ring EPDM/NBR + Dust Seal Wiper Maintenance-free service lifetime; zero weeping
Wedge Encapsulation Partial or full elastomer lining 100% Core Vulcanized EPDM (Bonded > 3.0 MPa) Zero bare-iron exposure; prevents corrosion scaling
Internal Coating Tech Liquid epoxy or fusion bonded WRAS-Compliant Fusion Bonded Epoxy ≥ 250 μm Dielectric holiday testing at 3 kV verification

Under CE Marking guidelines (Pressure Equipment Directive 2014/68/EU), our non-rising gate valves conform to Module H Full Quality Assurance. This ensures every individual casting heats undergoes rigorous mechanical testing: Charpy V-notch impact validation down to -10°C, hydrostatic shell integrity tests held for 180 seconds, and bi-directional low/high pressure pneumatic and hydraulic seat tests. We supply EN 10204 Type 3.1 inspection certification with every industrial procurement batch.

1987
Rubber Plant Inception
1996
Foundry Casting Inception
23,000 m²
Integrated Facility Base
100%
Hydrostatic Shell & Seat Tested
50+
Countries Exported
Application Engineering

Targeted Deployment Across Critical Fluid Infrastructure

From municipal water works in Europe to deep-well desalination complexes in the Middle East, our NRS valves are engineered to withstand severe environments.

Buried Municipal Networks

Designed for direct underground burial without construction of concrete maintenance chambers. Paired with telescopic extension spindles and surface road boxes, saving municipal contractors substantial civil excavation expenditure.

HVAC District Chilled Water

High-rise building basements and district cooling utility tunnels demand zero stem movement during actuation. Our low-torque NRS valves seamlessly pair with ISO 5211 direct-mount electric actuators for smart building automation.

Desalination & Seawater

When paired with nickel-aluminum bronze internal trim, stainless duplex stems, and high-performance fusion-bonded coatings, our gate valves prevent galvanic corrosion across harsh saline environments.

Wastewater Treatment (WWTP)

Features a straight-through bore without bottom recess pockets. Suspended grit, sand, and fibrous sludges flow uninhibited without wedging under the gate, maintaining tight shut-off integrity.

Strategic Market Analysis

Future Industry Trends & Global Procurement Requirements

Addressing digital asset tagging, smart IoT actuation, drinking water hygienic mandates, and supply resilience.

Smart Digital Pipeline Integration (IoT)

Modern infrastructure tenders increasingly require gate valves with pre-engineered smart sensing brackets. Tianjin Top Valve manufactures NRS gate valves featuring integrated stem stroke feedback sensors, wireless position monitors, and torque limit switches that transmit health diagnostics to municipal SCADA centers.

Stringent Potable Water Health Compliance

Regulatory authorities across the EU and North America have unified requirements under stringent biological leachability testing (WRAS, NSF/ANSI 61, ACS, UBA). By utilizing peroxide-cured EPDM formulated within our in-house rubber factory, our elastomeric wedges eliminate organic leaching, micro-bacterial proliferation, and heavy metal migrations.

Specialized Industrial Lines

High-Integrity Valve Assemblies for Demanding Process Networks

Explore specialized flow engineering solutions including abrasion-resistant elastomeric gate units, cryogenic ammonia valves, and high-pressure metal seated assemblies.

Wholesale Stainless Steel Butterfly Valve Durable & Corrosion-Resistant

Wholesale Stainless Steel Butterfly Valve - Durable & Corrosion-Resistant

View Specification
Supply Chain Security

Export Packaging & Comprehensive Quality Control

Zero transit deflection, zero coating abrasion, and 100% component trace documentation.

100% Hydrostatic Quality Release

Every non-rising gate valve undergoes hydrostatic pressure testing according to EN 12266-1 and ISO 5208 before packing. Our testing regimes inspect shell pressure at 1.5 times the nominal working pressure and seat integrity with zero drops allowed under bi-directional holding times.

Anti-Scratch Multi-Tier Packing

To protect the electrostatically applied epoxy coating during multimodal sea container voyages, valve bodies are individually bubble-wrapped with edge flange protectors. Products are secured within heavy-duty, heat-treated plywood crates compliant with ISPM 15 standards.

Remote Live Video Audits

Procurement teams and third-party inspectors (SGS, TÜV, Bureau Veritas) can conduct remote live video inspections. We guide engineers through spectrometry chemical analysis, ultrasonic wall thickness checks, coating holiday testing, and torque pressure benchmarking in real time.

Technical FAQ

Frequently Asked Questions: NRS Gate Valve Procurement

Clear technical answers addressing engineering standards, material verifications, CE compliance, and order logistics.

What specific CE certifications apply to your Non-Rising Stem (NRS) gate valves?
Our valves conform to the European Union's Pressure Equipment Directive (PED) 2014/68/EU under Module H (Full Quality Assurance), certified through independent Notified Bodies. This qualifies our valves for industrial pipeline applications handling Group 1 (hazardous) and Group 2 (non-hazardous) liquids and gases, fully backed by EN 10204 Type 3.1 material test certificates.
What is the functional difference between Non-Rising Stem (NRS) and Rising Stem (OS&Y) gate valves?
A Non-Rising Stem valve features internal stem threads; as the handwheel turns, the stem remains in fixed vertical alignment while the internal gate wedge moves along the threaded spindle. In contrast, an Outside Screw & Yoke (OS&Y) valve exposes its threads externally and lifts the entire stem upward during opening. NRS valves offer significant advantages in tight underground conduits, buried direct services, and congested pump vaults where headroom is restricted.
How does your in-house rubber factory ensure resilient wedge longevity?
Because we operate Tianjin Dongfang Rubber Factory (founded 1987), we control our own elastomeric formulations. We utilize premium, peroxide-cured EPDM polymers without unrefined fillers. Our proprietary high-pressure injection molding process vulcanizes the rubber onto the ductile iron core with bond strengths surpassing 3.0 MPa, preventing de-bonding, shearing, or micro-cracking over extensive operating cycles.
Can Tianjin Top Valve produce gate valves matching regional dimensional standards?
Yes. Our standard manufacturing molds accommodate EN 558 Series 14 (DIN 3202 F4 short body) and EN 558 Series 15 (DIN 3202 F5 long body). We also machine flange drilling patterns to EN 1092-2 PN10/PN16/PN25, ASME B16.1 Class 125, ASME B16.42 Class 150, BS 10 Table D/E, and AS 4087 patterns.
What internal surface coatings are applied to prevent corrosion?
All ductile iron bodies are shot-blasted to SA 2.5 cleanliness and coated with fusion-bonded epoxy (FBE) powder applied electrostatically to a minimum dry film thickness of 250 μm. Coatings are non-toxic, WRAS/potable water approved, and verified using high-voltage dielectric holiday testers at 3 kV to guarantee pinhole-free corrosion isolation.
What is the typical production and delivery lead time for export orders?
For standard DN50 to DN300 NRS resilient seated gate valves, common parts are kept in stock, enabling order assembly and pressure testing within 15–20 business days. Large custom project orders (up to DN1200 or specialized alloys like Ni-Al bronze or Duplex) generally require 30–45 days. Our factory is located near Tianjin Port, facilitating efficient sea container dispatch worldwide.
Are replacement parts, extension spindles, and actuator brackets available?
Yes. We provide complete modular support, including custom telescopic extension stems for deeply buried pipelines, street surface access boxes, ISO 5211 direct-mounting top flanges for electric/pneumatic actuators, position indicators, and replacement wedge subassemblies.