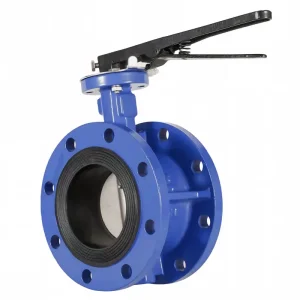
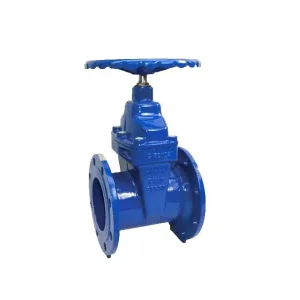
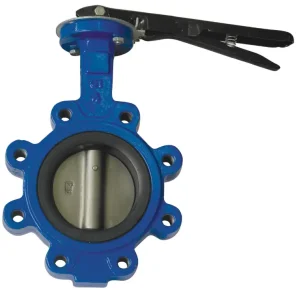
Featured Industrial Valve Engineering Solutions
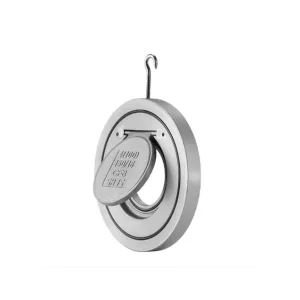
Explore precision-machined isolation and dynamic backflow mitigation units manufactured under ISO 9001 and CE directives for mission-critical hydraulic loops.



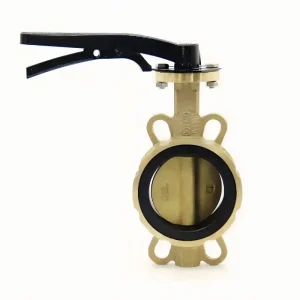



Industrial Evolution & Macro Procurement Dynamics
Modern fluid control systems demand zero-compromise engineering. Double flange butterfly valves have evolved from basic isolation units into precision throttling assets capable of continuous service under severe hydraulic shocks.
Total Cost of Ownership (TCO)
Procurement committees prioritize life-cycle longevity over nominal purchase outlay. In double flange installations, full-face rubber lining and integrally cast feet eliminate flange gasket misalignment, slashing plant maintenance labor by up to 43% over a standard 20-year cycle.
Rigid Structural Resistance
Unlike wafer designs that depend entirely on long cross-flange stud tension, double flanged architectures feature discrete bolting per face. This design absorbs massive pipeline tensile loads and seismic bending moments without distorting the internal seating bore.
Environmental & Fugitive Controls
Stringent international directives against atmospheric emissions mandate advanced stem packing geometry. Multi-stage O-ring seals coupled with internal blowout-proof stems safeguard critical installations from volatile discharge and potable distribution loss.
Vertically Integrated Foundry to Finished Assembly
Through Tianjin Donglian Valve Factory (since 1996) and Tianjin Dongfang Rubber Factory (since 1987), we control the metallurgy and polymer chemistry entirely within our 23,000 m² footprint.
| Component Assembly | Material Specification Options | Design Standard Compliance | Engineering Value Addition |
|---|---|---|---|
| Body Shell | Ductile Iron EN-GJS-450-10, GGG40, WCB, CF8M, C95800 | EN 593 / BS 5155 / API 609 Cat. B | In-house foundry ensures precise nodularity >90% and zero porosity in thick flanges. |
| Disc Geometry | Ductile Iron (Epoxy/Rilsan coated), 316 SS, Bronze, Ceramic | EN 1092-2 / ASME B16.5 / AWWA C504 | Hydrodynamically profiled disc edge reduces cavitation index and throttling drag. |
| Elastomer Seat | Food-grade EPDM (WRAS certified), NBR, FKM, Virgin PTFE | ISO 16915 / BS 6920 Drinking Water | Moulded and vulcanised in-house; compression set values tracked under ASTM D395. |
| Shaft & Bearing | SS410, SS420, 17-4PH, SS316, Monel K-500 | EN 12266-1 / API 598 Pressure Test | Self-lubricating PTFE-backed bronze bearings eliminate shaft seizure and lower torque. |
Macro Industry Engineering Solutions
Tailored flanged valve configurations engineered to solve hydrodynamic shocks, extreme corrosive saline immersion, and long-distance transmission surges.
Municipal Water Networks
Urban distribution mains demand zero leakage without water degradation. Our WRAS-compliant double flanged butterfly valves with certified EPDM liners prevent heavy metal leaching while sustaining millions of operating cycles across high-volume trunk lines.
Desalination & Marine Pipelines
Handling raw seawater and aggressive brine rejects causes rapid pitting in conventional iron trims. We engineer nickel-aluminum bronze (C95800) and duplex steel double flanged valves with fusion bonded epoxy coatings exceeding 300 microns for galvanic resistance.
Thermal & Hydro Power Generation
Turbine cooling loops and penstock isolation require rapid, fail-safe actuation. Our heavy-duty double eccentric flanged butterfly valves utilize hydraulic counterweight actuators to guarantee controlled, slam-free closure during sudden electrical trip emergencies.
Full Lifecycle Verification & Traceability
EPC project managers rely on uncompromising technical verification. Every production order includes documented chemical, mechanical, and pressure test certifications.
EN 10204 3.1 Traceability
From raw furnace melt charge to final hydrostatic pressure logging, every valve body carries cast heat numbers linked directly to spectrometry records and elongation test data in our physical-chemical laboratory.
Expedited Global Logistics
Located in Wuxia Industrial Park, Dongli District, Tianjin, our factory sits within 30 minutes of Tianjin Xingang Port. Every valve is sealed in moisture-proof bubble packing and robust seaworthy timber crates compliant with ISPM-15 phytosanitary rules.
Factory Witness & Remote Auditing
We facilitate third-party witness inspections (SGS, TÜV, Bureau Veritas) and offer live video factory walk-throughs, enabling project procurement teams to inspect hydrostatic bench tests and coating thicknesses from anywhere in the world.
Technology Roadmap: Intelligent Valves & Materials
The industrial valve sector is converging toward predictive maintenance and smart flow modulation. Here is how our R&D engineering center is pioneering future-proof valve architectures.
IoT-Integrated Smart Actuation
Development of integrated torque sensors and partial stroke testing (PST) protocols within our electric and pneumatic actuator interfaces to predict seal degradation and identify scale buildup prior to operational failure.
Advanced Elastomeric Nano-Composites
Building upon our rubber facility's compounding legacy, our chemists are synthesizing fluorocarbon and graphene-infused EPDM formulations designed to resist chloramine degradation and abrasive silt scour at elevated pressures.
Low Carbon Foundry Practices
Transitioning toward automated electric induction casting processes paired with recycled metallic charge to deliver documented reductions in embodied carbon per metric ton of cast valve body.
Frequently Asked Engineering & Procurement Questions
Clear technical answers addressing double flange geometry, material selection, standard interchangeability, and international certifications.
Why choose a double flange butterfly valve over a wafer or lug type?
Are your flanged butterfly valves certified for drinking water distribution?
How does an in-house rubber factory impact valve reliability?
Which international flange drilling and face-to-face standards do you supply?
What testing procedures are applied to every double flange butterfly valve?
Can your valves be retrofitted with third-party electric or pneumatic actuators?
Industrial Gate, Globe, Check & Flanged Valves
Comprehensive flow regulation assemblies engineered for power plants, industrial refrigeration, underground municipal lines, and extreme temperature services.