

Direct Factory Supply
Engineered Cryogenic & High-Pressure Globe Valves
Precision-machined isolation and regulation valves manufactured under certified ISO 9001 and CE quality systems, offering zero-leakage security in severe duty applications.
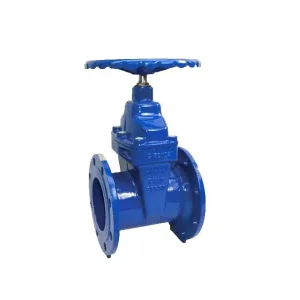
Non-Rising Stem Elastic Seat Gate Valve
Inquire Now →
Pneumatic Fast-Actuation Butterfly Valve
Inquire Now →
Full Rubber Coated Non-Return Check Valve
Inquire Now →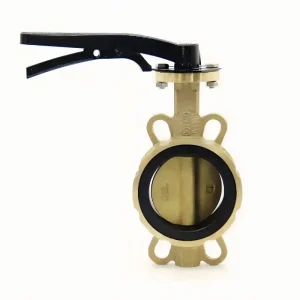
Corrosion-Resistant Aluminum Bronze Valve
Inquire Now →
CE Compact Low-Pressure Drop Check Valve
Inquire Now →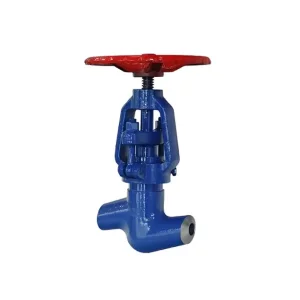
High-Temp High-Pressure Power Station Valve
Inquire Now →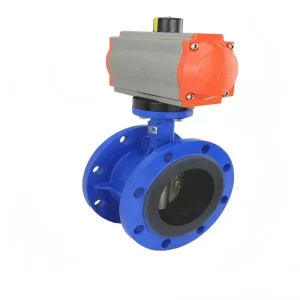
Pneumatic Lug Flanged Flow Valve
Inquire Now →Industry Insight & Whitepaper
Navigating Severe Low-Temperature Dynamics: The Industrial Cryogenic Imperative
In the global transition toward cleaner fuel vectors and intensified industrial gas processing, Cryogenic Globe Valves represent the critical barrier between safe containment and catastrophic pipeline failure.
LNG & Clean Energy Scaling
With the aggressive ramp-up of liquefaction terminals, floating production storage and offloading (FLNG), and bunkering stations, valves operating at -162°C require zero thermal contraction binding, precise cavitation management, and fugitive emissions control according to ISO 15848-1.
Air Separation (ASU) Demands
Handling liquid oxygen (LOX), liquid nitrogen (LIN), and liquid argon (LAR) at temperatures as low as -196°C requires thorough degreasing, ultrasonic cleaning, and ASTM G93 compliance to prevent violent exothermic ignition under oxygen flow conditions.
Liquid Hydrogen (LH2) Frontiers
Operating at an extreme -253°C, liquid hydrogen pushes metals to their physical embrittlement limit. Advanced austenitic stainless steels (316L/316LN) and specialized Kel-F (PCTFE) seat seals prevent structural cleavage and preserve seat sealing under cryogenic cycles.
Standardization & Parameters
Technical Matrix: CE Pressure Equipment Directive (PED 2014/68/EU) Standards
Every cryogenic valve manufactured under our quality assurance regimen is designed, cast, machined, and certified in accordance with strict international standards.
| Parameter / Metric | BS 6364 / ASME B16.34 Baseline | Top Valve Extended Bonnet Execution | Operational Value Delivered |
|---|---|---|---|
| Operating Temperature | -46°C to -196°C | -196°C to +120°C (LH2 optional to -253°C) | Full spectrum containment of LNG, LOX, LIN, and LAR. |
| Bonnet Design | Extended Vapor Column | Vapor Column Length compliant with BS 6364 / EN 12567 | Maintains gland packing in gas state to eliminate stem freezing. |
| Body & Trim Metallurgy | ASTM A351 CF8M / CF3M | Electroslag Remelted 316L / Dual Certified SS with Charpy V >45J | Eliminates low-temperature ductile-to-brittle transition risk. |
| Seat & Disc Interface | Stellite Hardfaced or PCTFE | Stellite 6 Overlaid + Renewable Cryogenic Grade PCTFE Soft Insert | Achieves ISO 5208 Rate A (Bubble-tight zero leakage). |
| Compliance Certification | Standard Factory Test Report | CE-PED Module H, EN 10204 3.1 / 3.2, ATEX, ISO 15848-1 | Audit-ready compliance across the European Union and worldwide. |
Global Footprint & Innovation
Field-Proven Deployment & Next-Generation Roadmap
Combining 30+ years of vertical manufacturing with continuous R&D into cryogenic dynamics, smart actuation, and digital emissions tracking.
Regional Engineering Hubs
Fast-track technical verification, hydrostatic shell re-testing, and local stocking programs for critical LNG bunkering hubs across Europe, Southeast Asia, and the Middle East to minimize downtime.
Digital Cavitation Sensing
Incorporating smart IoT piezoelectric sensor taps within the globe valve throat to analyze acoustic signatures, providing real-time alerts for seat erosion, micro-flashing, or localized cavitation.
Hydrogen Liquefaction Focus
Developing zero-loss thermal barrier jackets and non-destructive magnetic permeability testing to maintain ultra-low boil-off rates and metallurgical stability in high-purity hydrogen service.
Knowledge Base
Frequently Asked Technical Questions
Common inquiries from EPC contractors, design institutes, and procurement managers evaluating CE-certified cryogenic globe valves.
Q1. Why is an extended bonnet mandatory on cryogenic globe valves?
The extended bonnet acts as a vapor column (per BS 6364). By elevating the stem packing area away from the cryogenic fluid (-162°C to -196°C), the boil-off gas trapped inside warms to near ambient temperatures. This prevents the graphite or PTFE gland packing from freezing, preserving elastic recovery and preventing stem leaks.
Q2. What does CE Certification (PED 2014/68/EU) require for cryogenic service?
CE-PED compliance requires materials with proven low-temperature impact toughness (minimum Charpy V-notch energy of 27J at -196°C), verified non-destructive testing (NDT/RT/PT), validated pressure wall thickness calculations, and Module H full quality assurance surveillance by a Notified Body.
Q3. How do you prevent internal cavity overpressurization?
Globe valves are less vulnerable to trapped cavity overpressurization than floating ball valves due to their single-seated profile. In bi-directional or balanced cage designs, an upstream pressure-equalization drill hole or directional seat relief port is engineered to vent trapped boil-off gas automatically.
Q4. Which cleaning protocols are executed for cryogenic oxygen duty?
Valves built for oxygen duty undergo ultrasonic degreasing using halogen-free agents, complete black-light inspection under ultraviolet lamps (ASTM G93 / EN 12300 standard), and hermetic dual-layer bagging with desiccants to maintain zero hydrocarbon contamination.
Comprehensive Portfolio
Engineered Butterfly, Check & Control Valve Series
Complementary high-reliability piping components for cryogenic, municipal, power, and industrial chemical process facilities.

CE Gear Operated High-Torque Butterfly Valve
Inquire Now →
Compact Flow Control Wafer Butterfly Valve
Inquire Now →
Rubber Lined Leak-Proof Pinless Valve
Inquire Now →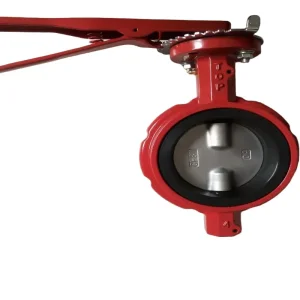
Lugless Semi-Shaft Resilient Wafer Valve
Inquire Now →
CE Certified Municipal Water Butterfly Valve
Inquire Now →
PTFE Lined Anti-Corrosive Cast Valve
Inquire Now →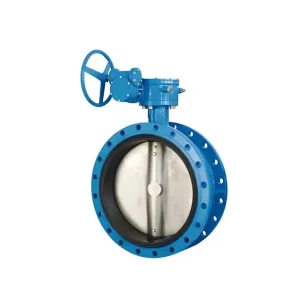
Low-Torque Flanged Heavy-Duty Valve
Inquire Now →
