

Anti-abrasive resilient seated gate valve built with reinforced wedge technology for slurry and particulate resistance.
Wholesale Anti - Abrasion Elastic Seat Gate Valve with Reinforced Seat Suppliers, SupplierPrecision-manufactured valves tested under stringent hydrostatic requirements for enterprise systems.
Anti-abrasive resilient seated gate valve built with reinforced wedge technology for slurry and particulate resistance.
Wholesale Anti - Abrasion Elastic Seat Gate Valve with Reinforced Seat Suppliers, Supplier
Corrosion-barrier PTFE seated and encapsulated disc butterfly valve suited for aggressive chemical processes.
Wholesale PTFE Lined Cast Body Butterfly Valve Suppliers, Factory
Heavy-duty double flanged butterfly valve engineered to EN 593 dimensional constraints for dependable pipe isolation.
CE Certification Flanged Butterfly Valve - Durable & Efficient Flow Control Suppliers, Supplier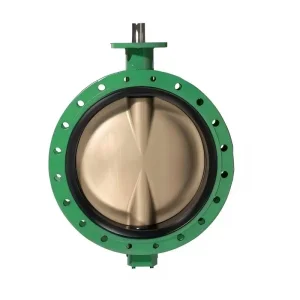
Municipal water network compliant butterfly valve offering low hydrodynamic resistance and longevity.
High-Quality Water Used Flanged Butterfly Valve - Durable & Efficient Manufacturer, Factories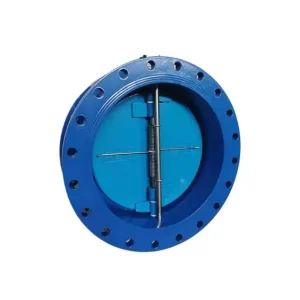
Compact dual-plate spring-assisted check valve for slam-free operation and backflow protection in pumping stations.
Wholesale Dual Plate Flange Type Check Valve Factories, Factory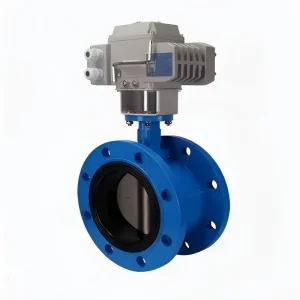
Quarter-turn automated valve coupled with intelligent electric actuators for automated process plant throttling.
High-Quality High-Performance Electrical Butterfly Valve for Seamless Control Suppliers, Manufacturers
Slim profile wafer connection butterfly valve engineered for versatile installation between multiple flange ratings.
Wholesale Wafer Butterfly Valve - Durable & Efficient Flow Control Solution Suppliers, Factory
Pneumatically actuated wafer assembly for high-cycling rapid shut-off in critical industrial process lines.
High-Quality Actuator Wafer Butterfly Valve Supplier, ManufacturersIn standard butterfly valve manufacturing, the disc is joined to the operating drive shaft by through-pins, taper pins, or tangential bolts. While functional for benign environments, through-pin designs inevitably introduce significant long-term failure points: continuous dynamic cycle loads shear mechanical pins, media breaches the disk through penetrating pin holes, and galvanic corrosion accelerates around uneven joints. For mission-critical piping systems within European and international jurisdictions, specifying CE Certification Pinless Butterfly Valves manufactured by integrated precision facilities has transitioned from an elective engineering choice to an operational mandate.
The pinless valve architecture isolates the working fluid entirely from the valve shaft. Torque transmission is achieved strictly via internal geometric profiles: splined stems, high-tolerance double-D interfaces, or internal broached polygons. By eliminating through-holes on the flow disc, the internal hydrodynamic profile remains streamlined, lowering the overall cavitation index and ensuring zero secondary migration paths for toxic or aggressive media to encounter the stem packing.
Pinless disc design generates higher flow coefficients (Cv) than pinned alternatives because the absence of obtrusive pin hubs lowers localized turbulence. Pressure losses across the valve seat are reduced by up to 14% under high Reynolds numbers, resulting in lower operational pumping costs throughout the lifetime of the infrastructure facility.
| Evaluation Parameter | Conventional Pinned Butterfly Valve | Engineered Pinless Butterfly Valve |
|---|---|---|
| Disc-to-Stem Sealing Integrity | Multiple through-hole piercing points vulnerable to seal degradation and fluid bypass. | Completely solid disc face; 100% dry stem design eliminates internal leak paths. |
| Cyclic Torque Transmission | Point-loaded shear stress concentrated along tiny pin diameters; subject to shear fatigue. | Distributed planar torque across double-D, keyed, or internal precision broached splines. |
| Maintenance Downtime | High. Seized, corroded pins often require drilling or destruction of the complete disc-stem set. | Rapid non-destructive disassembly; slip-fit shafts allow modular seat replacement on-site. |
| Erosion & Cavitation Resistance | Pin protruding contours trigger localized eddy currents, leading to pitting erosion. | Smooth hydro-contoured disc profile minimizes vortex shedding and seat abrasion. |
How end-to-end metallurgical control, automated foundries, and integrated rubber synthesis deliver global value.
Unlike international assemblers dependent on outsourced castings, Chinese manufacturing centers in industrial clusters like Tianjin operate fully integrated smelting, casting, and thermal normalization plants. Group-owned foundries guarantee traceable spectrometer chemistry across every ductile iron (QT450-10, GGG40/50), WCB, CF8M, and nickel-aluminum bronze pouring heat.
With rubber compounding legacies operating continuously since 1987, factory-direct manufacturers formulate raw elastomers internally. EPDM, high-nitrile NBR, and fluoroelastomers (FKM) are custom-compounded to optimize compression set, elongation, and abrasive recovery, preventing seat extrusion and premature tear-out under high differential pressures.
Pinless valve stems rely entirely on micrometric manufacturing tolerances. Modern workshops deploy specialized horizontal and multi-axis CNC broaching centers that machine drive flats, square drives, and polygon discs with tolerances maintained within ±0.012 mm. This eliminates backlash, chattering, and rotational hysteresis when coupled with precise electric or pneumatic actuators.
Every individual CE-marked valve undergoes automated dual-phase hydrostatic testing matching ISO 5208 Rate A standards. Shell tests at 1.5× nominal pressure rating and bi-directional seat tests at 1.1× rated pressure ensure that absolutely zero droplet leakage occurs before packaging, eliminating field commissioning failures for global EPC projects.
By clustering metallurgy, rubber synthesis, machining, electrostatic epoxy coating lines, and international logistics near deep-water transport terminals like Tianjin Port, Chinese valve factories compress project lead times by 35% compared to Western counterparts while maintaining competitive capital expenditure margins for international contractors.
Where high-performance metallurgy, digital smart monitoring, and decarbonization converge.
With strict international carbon and pollutant targets, ISO 15848-1 certified live-loaded stem seals are now directly integrated into pinless butterfly valve yokes. Multi-level O-rings backed by PTFE V-rings ensure that no volatile organic compounds escape past the stem collar.
The industry is advancing past basic rubber liners toward high-crystallinity fluoropolymers like melt-processable PFA, Halar (ECTFE), and engineered ceramic disc inserts. These coatings enable pinless butterfly valves to operate in highly acidic, chlorinated, and aggressive slurry conditions.
Modern enterprise infrastructure demands digital twin alignment. Pinless butterfly valves are increasingly pre-machined with standard ISO 5211 direct-mount flanges and outfitted with embedded torque monitors, angular Hall sensors, and predictive seat wear monitors.
The massive global expansion of SWRO (Seawater Reverse Osmosis) desalination and green hydrogen cooling circuits requires lightweight, non-corroding flow hardware. Pinless designs utilizing super duplex stainless steel and nickel aluminum bronze discs are leading this critical shift.
Tailoring pinless disc performance to complex fluid dynamics and extreme operational parameters.
Standard pinned valves frequently leach contaminants or fail hygienic approvals due to pockets behind the disc pins. WRAS and CE approved pinless butterfly valves with bonded food-grade EPDM seats eliminate stagnant water crevices, preserving water quality across multi-kilometer municipal distribution mains.
Ballast water management and marine cooling systems face relentless crevice corrosion from chloride-rich seawater. By deploying pinless butterfly valves cast from C95800 Nickel-Aluminum Bronze paired with vulcanized nitrile seats, shipbuilders achieve fail-safe operation resistant to marine biofouling and galvanic decay.
Chilled water loops and high-rise commercial HVAC riser applications require tight throttling control and dependable thermal cycling stability. The low breakout torque of pinless stems reduces actuator motor size requirements by 15-20%, driving tangible electrical efficiencies in massive building automation projects.
Corrosive chemical scrubbing applications attack internal valve components. Pinless butterfly valves completely encapsulated with virgin PTFE or Halar resins present a seamless chemical barrier. The absence of mechanical pin penetrations removes the risk of aggressive vapor migration into the shaft packing.
Handling abrasive fly ash and lime slurry quickly erodes mechanical disc pins, resulting in disc detachment. Specialized pinless valves utilizing abrasion-resistant hard-faced stainless steel or solid structural ceramic discs maintain mechanical integrity under persistent high-velocity scouring.
The mandatory verification steps international engineering contractors (EPCs) demand before vendor list onboarding.
When Tier-1 global procurement divisions audit an industrial valve factory for international contracts, regulatory compliance extends well beyond physical appearance. Pinless butterfly valves intended for European Union infrastructure or international petrochemical ventures must satisfy stringent legal mandates defined under the Pressure Equipment Directive (PED 2014/68/EU), CE Marking protocols, and comprehensive quality assurance systems.
Tianjin Top Automation Equipment Co., Ltd. incorporates these global technical mandates directly into daily production runs across its 23,000 m² manufacturing campus. Because casting chemistry, rubber compounding, precision machining, and non-destructive examination (NDE) operate on a consolidated site, procurement executives can audit every link in the quality chain directly.
Factory production systems are certified under full quality assurance Module H of the Pressure Equipment Directive. This authorizes the design, production, final inspection, and pressure testing of valves intended for Category I through Category III pressurized hazards with notified body oversight.
Global projects demand verifiable material test reports (MTR). Every batch of raw melt from the group's foundry is supplied with authentic 3.1 certificates detailing exact chemical spectrometry (C, Si, Mn, P, S, Cr, Ni, Mo) and physical tensile/yield testing traceable to unique cast heat numbers stamped on the valve body.
Rubber components undergo strict rheometer cure verification, ASTM D395 compression set analysis, and micro-hardness testing. Valves destined for potable water distribution carry verifiable WRAS and NSF certifications guaranteeing zero cytotoxic plasticizer leaching over decades of service.
Fully traceable, CE-certified valve inventory ready for global project deployment.
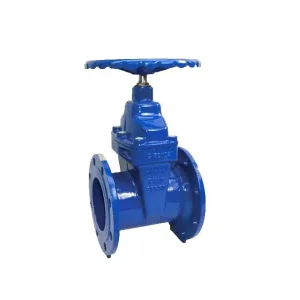
Compact vertical profile non-rising stem elastic seated gate valve for underground pits and low-headroom pipelines.
High-Quality Non-Rising Stem Elastic Seat Sealing Gate Valve Manufacturer, Factory
WRAS certified lug butterfly valve featuring threaded bolt lugs designed for dead-end terminal line service.
Wholesale WRAS Approved Lug Type Butterfly Valve 4325G Supplier, Factories
High-reliability wafer butterfly valve optimized for potable water systems, equipped with precision gear operator.
CE Certification WRAS Approved High-Performance Butterfly Valve 4020G Manufacturer, Factories
Lever-operated certified lug pattern butterfly valve providing instant 90-degree visual shut-off status.
High-Quality WRAS Approved Butterfly Valve Lug Type 4325L Manufacturer, Factories
Multi-standard certified metal-to-metal hard seal butterfly valve engineered for elevated temperature and steam networks.
Wholesale CE/ISO/DIN/BS High Pressure Metal Seal Hard Seal Butterfly Valve Manufacturers, Manufacturer
Self-cleaning micro-resistance ball check valve for sewage, stormwater pumping, and viscous wastewater lines.
CE Certification Micro-Resistance Ball Check Valve Manufacturers, Factories
Corrosion-engineered pinless butterfly valve lined with high-purity ECTFE/Halar for handling aggressive chemicals.
Wholesale Halar Lined Pinless Butterfly Valve Supplier, Manufacturer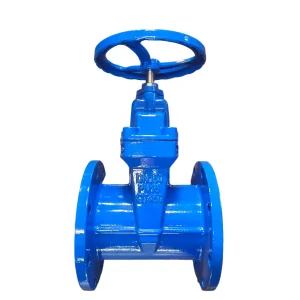
Heavy-duty industrial resilient seat gate valve delivering full-bore, low-pressure-drop fluid isolation.
Wholesale High-Quality Gate Valve for Reliable Flow Control Manufacturer, FactoriesDirect answers to the most common questions raised by pipeline engineers and EPC buyers.
Pinless butterfly valves eliminate through-shaft holes in the disc body. In pinned designs, these holes introduce leak paths, weaken the disc structure, and cause localized galvanic corrosion between the pin and disc. The pinless architecture utilizes internal torque transfer interfaces (such as square drives, splines, or double-D connections), resulting in a 100% dry stem design, reduced flow turbulence, lower dynamic torque, and significantly simplified seat replacement during plant maintenance.
Our CE-marked valves comply with the European Pressure Equipment Directive (PED 2014/68/EU) Module H, EN 593 (industrial butterfly valves), EN 12516 (shell strength), EN 1092-2 (flange connection specs), and ISO 5208 / EN 12266-1 (Rate A zero-leakage hydrostatic pressure testing). Valves designated for drinking water networks are also tested to comply with WRAS (Water Regulations Advisory Scheme) and NSF-61 material toxicity limits.
The elastomer liner determines the sealing longevity and torque requirements of a butterfly valve. Because our group operates Tianjin Dongfang Rubber Factory (established in 1987), we do not buy generic third-party liners. We compound and vulcanize high-grade EPDM, NBR, and fluoroelastomers in-house, closely monitoring tensile properties, recovery, and compression set. This avoids premature hardening, extrusion, and seat tearing under high cycle frequencies.
Our wafer, lug, and double-flanged pinless butterfly valves are produced with universal flange locating holes and precise drilling that align with EN 1092-1/2 (PN10/PN16), ASME/ANSI B16.1 Class 125, ASME B16.5 Class 150, BS 10 Table D/E, and JIS B2238/2239 (10K/16K). Full technical datasheets and CAD/3D dimensional drawings are provided during the submittal phase to ensure proper pipeline fit.
Yes. Every valve body is cast and machined with an integral ISO 5211 direct-mount top flange. This standardization permits direct, low-profile mounting of pneumatic scotch-yoke actuators, rack-and-pinion units, electric quarter-turn actuators, or manual worm gears without bulky intermediate brackets, minimizing mechanical play and hysteresis.
Every single valve undergoes a 100% two-step pressure test in accordance with ISO 5208: a hydrostatic shell test at 1.5 times the rated PN, and a bi-directional seat leakage test at 1.1 times the rated PN (achieving zero bubbles under Rate A criteria). Coating thickness checks (typically 250 μm electrostatic epoxy), spectrometer chemical verification, and operational torque tests are recorded under EN 10204 Type 3.1 documentation supplied with your shipment.
