Industrial Precision Engineering
High-Integrity Valve Solutions Under CE Protocols
Explore our core certified valve units manufactured with integrated casting and mechanical processing to guarantee bubble-tight isolation.
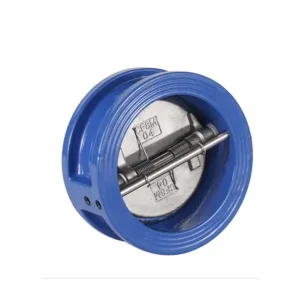
High-Quality High-Performance Dual Plate Wafer Check Valve for High-Flow Systems
Request Specs & CAD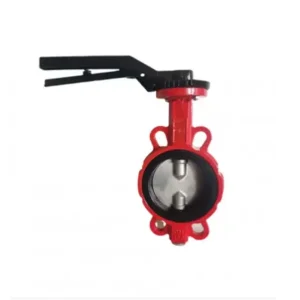
High-Quality Double Half Shaft Wafer Butterfly Valve Supplier & Factory
Request Specs & CAD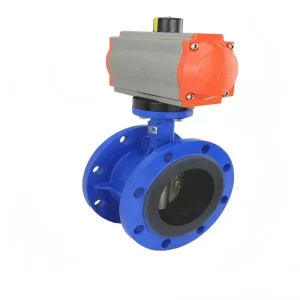
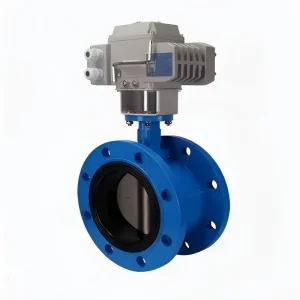
High-Quality Pneumatic Butterfly Valve Reliable Flow Control Solution
Request Specs & CAD
Wholesale Straight-Through Ammonia Globe Valve Manufacturers & Plant
Request Specs & CAD
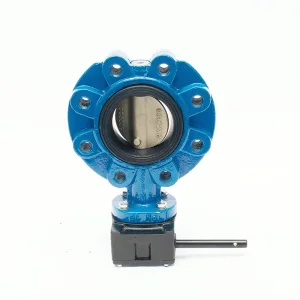
CE Certification Gear Operated Butterfly Valve - Durable & Reliable Supplier
Request Specs & CAD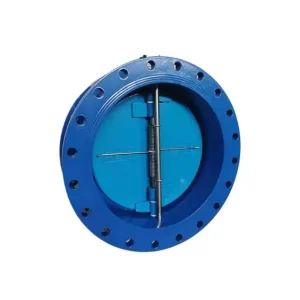
Wholesale Dual Plate Flange Type Check Valve Factories & Manufacturer
Request Specs & CAD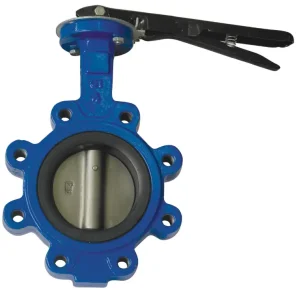
High-Quality Lug Type Manual Operated Butterfly Valve Factory
Request Specs & CAD
Engineering White Paper
CE-Certified Manual Operated Globe Valves: Technical Anatomy & Flow Control Dynamics
Analyzing seat load integrity, stem buckling resistance, and Pressure Equipment Directive (PED 2014/68/EU) compliance in critical process piping networks.
PED 2014/68/EU & Module H Compliance
Manual operated globe valves specified for European industrial deployment mandate thorough conformity under Category III/IV pressure vessels. Complete material traceability (EN 10204 3.1 certification), finite element analysis (FEA) of body wall thicknesses, and strict burst-safety design factors safeguard systems under fluctuating thermodynamic loads.
Stem Guiding & Torque Transmission
Unlike quarter-turn valves, manual globe valves convert rotational input torque into precise linear force via acme-threaded stems. Our precision-ground trapezoidal screw threads reduce operator rim-effort by over 35%, ensuring precise throttling resolution while preventing galling across severe thermal cycling.
Hard-Faced Seating & Leak Prevention
Equipped with Stellited (Cobalt-base alloy) or high-grade stainless steel weld overlays on both disc and body seat rings, manual globe valves prevent high-velocity steam cavitation and wire-drawing erosion. Verified to EN 12266-1 Rate A zero-leakage standards.
| Design Attribute | Standard Globe Valve Spec | Tianjin Top Valve CE-Grade Execution | Operational Impact |
|---|---|---|---|
| Pressure Standards | ASME B16.34 / Class 150-300 | EN 13709 / EN 12516 / PN16 to PN100 | Guaranteed compliance across EU process plants |
| Stem Packing Integrity | Basic PTFE Packing | Die-formed flexible graphite + Inconel wire mesh | Zero fugitive emission (ISO 15848-1 Class AH/BH) |
| Disc Profiling | Flat Seating Plug only | Parabolic Throttling Plug / Needle Regulating Disc | Linear flow characteristic with 0.5% throttling accuracy |
| Bonnet Architecture | Standard Bolted Bonnet | OS&Y (Outside Screw & Yoke) with integral back-seat | Stem repacking capability under full pipeline pressure |
Foundry-Direct Scale
Why Tier-1 EPCs Source CE Globe Valves from Tianjin Top Valve
Combining legacy metallurgical foundry capability (since 1996) with in-house elastomer vulcanization (since 1987) to eliminate trading markups and ensure end-to-end traceability.
In-House Group Foundry
By casting our ductile iron (EN-GJS-400-15), cast steel (GP240GH / WCB), and stainless steel (1.4408 / CF8M) bodies internally, we maintain complete control over melt chemistry, microstructure porosity, and tensile performance before machining starts.
Elastomer & Polymer Mastery
Backed by Tianjin Dongfang Rubber Factory (founded 1987), our proprietary EPDM, NBR, FKM, and PTFE compounding delivers low compression set, high chemical resilience, and extended seal life under thermal stress.
Advanced CNC Cell Centers
Multi-axis horizontal machining centers ensure tight tolerances for body neck bores, seat tapers, and disc profiles. Precise dimensional consistency translates into smooth manual handwheel operation and uniform seating contact pressure.
100% Dual Testing Regimen
Every single valve undergoes shell hydrostatic testing at 1.5× PN rating and low/high-pressure seat leakage checks per EN 12266-1 prior to packaging. Complete pressure-decay data logs are archived for end-user QA audits.
1987
Rubber Sealing R&D Origin
23,000 m²
Integrated Manufacturing Campus
50+
Global Countries Exported
100%
Individual Hydro & Shell Testing
Domain Engineering
Macro Applications & Tailored Industry Solutions
Engineered to handle extreme delta-P pressures, cryogenic flash phases, and erosive velocities across heavy chemical, municipal, and energy production matrices.
Industrial Refrigeration & Ammonia (NH3)
Anhydrous ammonia cooling loops demand zero atmospheric permeability. Our straight-through CE ammonia globe valves integrate deep gland packingboxes, PTFE disc inserts, and specialized bonnet back-sealing to prevent volatile emissions in cold-storage logistics complexes.
Thermal Power Stations & Superheated Steam
High-temperature steam headers (up to 425°C) induce intense thermal shock and body creep. Our GS-C25 / GP240GH cast steel manual globe valves leverage hardened Stellite hard-facing discs to resist steam wire-drawing during micro-throttling bypass routines.
Chemical Processing & Vacuum Isolation
Vacuum systems and hazardous fluid circuits benefit from bellows-sealed and high-density gland manual globe valves. Complete isolation safeguards vacuum distillation column stability down to 1.33 Pa while meeting strict zero-emission environmental criteria.
Strategic Forecast
Emerging Industry Trends & Global Procurement Drivers
Market intelligence overview: how emissions regulations, lifecycle TCO audits, and digital material passports are reshaping global valve supply contracts.
Low-Emission Fugitive Control (ISO 15848-1)
Global refinery and LNG terminal projects increasingly mandate EN ISO 15848-1 Class AH/BH compliance for manual valves. Procurement managers now require certified live-loaded stem packing systems and helium sniffer leak detection tests to eradicate fugitive volatile organic compound (VOC) emissions.
Supply Chain Regionalization & De-Risking
International engineering firms are shifting from fragmented component trading houses to direct-foundry Chinese partners who possess internal metallurgical and elastomer capabilities. Controlling the melt-to-test pipeline provides robust lead-time assurance for fast-track megaprojects.
Total Cost of Ownership (TCO) Prioritization
Procurement criteria have transitioned from lowest initial capital expenditure to life-cycle maintenance cost. Re-grindable valve seat designs, renewable discs, and grease-injected stem bushings extend turnaround cycles from 24 to 72 months in severe operating conditions.
Procurement Knowledge Base
Frequently Asked Questions on CE Manual Globe Valves
Detailed technical, certification, and logistical answers direct from our senior valve engineering team.
What specific CE directives apply to manual operated globe valves exported to Europe?
Manual globe valves destined for European industrial use must conform to the Pressure Equipment Directive (PED) 2014/68/EU. Depending on maximum allowable pressure (PS), nominal bore diameter (DN), and fluid classification (Group 1 hazardous fluids vs. Group 2 non-hazardous fluids), valves fall into Category I, II, III, or IV. Tianjin Top Valve manufactures under Module H quality system conformity, accompanied by EN 10204 Type 3.1 material test certificates and official CE marked identification plates.
How does a manual globe valve differ from a gate or butterfly valve in fluid control?
While gate valves are strictly on/off devices subject to high seat erosion if throttled, and resilient butterfly valves offer compact lower-cost throttling in low-pressure lines, the manual globe valve is expressly engineered for linear throttling precision and frequent cycling. Its plug travels perpendicular to the seat ring, providing short travel distance, proportionate flow regulation, and the capacity to handle high pressure-drop environments without flutter or premature seal failure.
What seat and plug material options are available for severe ammonia or steam services?
For steam services up to 425°C, we provide cast carbon steel (GP240GH / 1.0619) bodies with Stellited (Cobalt Alloy #6) or 13Cr stainless steel overlay seats. For industrial refrigeration ammonia (NH3) circuits, we execute straight-through or angle pattern globe valves with low-temperature carbon steel bodies, PTFE soft-sealing inserts, stainless steel stems, and chambered graphite packing to eliminate micro-leak paths across -40°C to +150°C.
Can your factory supply custom flange drilling standards and face-to-face dimensions?
Yes. We manufacture to both European standards (DIN EN 1092-1 PN16, PN25, PN40, with EN 558 series 1 face-to-face dimensions) and American standards (ASME B16.5 Class 150, 300, 600, with ASME B16.10 dimensions). Furthermore, BS 10 and JIS flange drillings can be accommodated through our precision CNC production cells.
What is the lead time for standard versus customized CE manual globe valves?
Standard inventory sizes (DN15 to DN200 in ductile iron and WCB) are typically assembled, pressure-tested, and prepared for export packing within 15–20 business days. For customized alloy compositions (Duplex, Monel, Aluminum Bronze) or specialized bellows-seal designs, factory lead times average 30–45 days. Our proximity to Tianjin Port provides expedited container freight turnaround to global ports.
Comprehensive Valve Catalog
High-Performance Pipeline Flow Solutions
Explore our extended series of butterfly, check, gate, and specialized marine-duty valves engineered for zero downtime in industrial plants.
CE Certification Compact Wafer Lift Check Valve with Low-Pressure Drop
Request Specs & CAD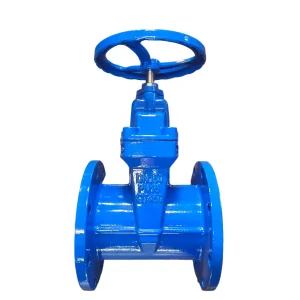
Wholesale High-Quality Gate Valve for Reliable Flow Control Manufacturer
Request Specs & CAD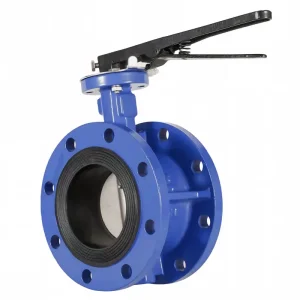
CE Certification Flanged Butterfly Valve with Lever Actuator Factory
Request Specs & CAD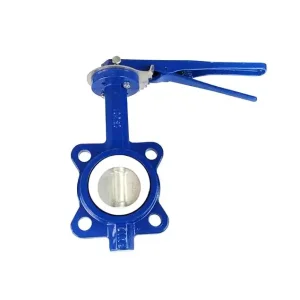
High-Quality PTFE Lined Pinless Butterfly Valve Supplier & Factories
Request Specs & CAD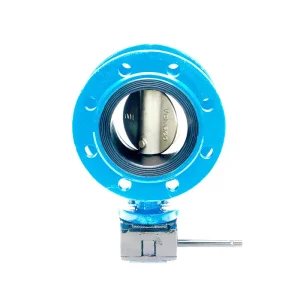
High-Quality Marine Flange Type Manual Operated Butterfly Valve
Request Specs & CAD
CE Certification PTFE Lined Stainless Steel Butterfly Valve Manufacturer
Request Specs & CAD
High-Quality Rubber Lined Pinless Butterfly Valve Supplier & Factories
Request Specs & CAD