Certified High-Performance Industrial Valves
Direct from our manufacturing hubs in Tianjin, China. Each unit is subjected to rigorous 100% shell hydrostatic and bidirectional seat pneumatic pressure testing conforming to EN 12266-1 and API 598 standards.
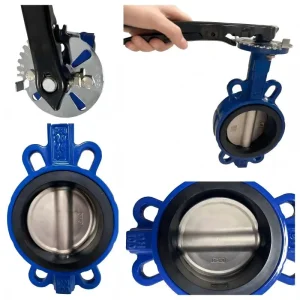
High-Quality WRAS Approved Butterfly Valve - High Performance & Durability 4020L
Explore Specifications
CE Certification Bronze Disc Wafer Butterfly Valve - Durable & Efficient Factory
Explore Specifications
High-Quality Pneumatic Butterfly Valve - Efficient Flow Control Solution Suppliers
Explore Specifications
CE Certification WRAS Approved High-Performance Butterfly Valve 4020G Manufacturer
Explore Specifications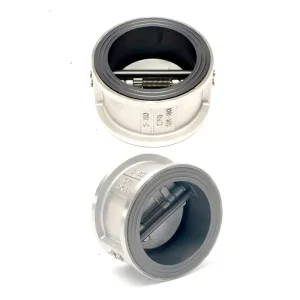



CE Certification & PED 2014/68/EU Actuator Globe Valve Compliance
In automated fluid handling systems, an actuator globe valve represents the primary pressure-retaining and high-precision throttling boundary. Achieving authentic CE marking requires comprehensive technical verification beyond superficial labeling.
For global piping designers, Engineering Procurement and Construction (EPC) conglomerates, and plant safety managers, specifying an actuator globe valve requires stringent adherence to international statutory directives. Within the European Economic Area (EEA) and global markets adhering to harmonized ISO/EN standards, compliance with the Pressure Equipment Directive (PED) 2014/68/EU is mandatory for fluid handling assemblies exceeding allowable pressure-volume thresholds (PS·V > 50 bar·L).
Tianjin Top Automation Equipment Co., Ltd., leveraging over three decades of advanced industrial metallurgy and automated flow-control manufacturing since 1987/1996, operates under certified Module H (Full Quality Assurance) conformity regimes. This ensures that every cast carbon steel (WCB, WCC), low-temperature alloy (LCB, LCC), and austenitic stainless steel (CF8, CF8M, CF3M) valve body undergoes exhaustive non-destructive testing (NDT), finite element pressure boundary analysis, and microstructural verification before actuation coupling.
Pressure Equipment Directive (PED) Conformity
Compliance with PED Category II, III, and IV requires verified wall thickness calculations per EN 12516-2 (Industrial valves - Shell design strength). Valve bonnets, body castings, and gland flanges are mathematically analyzed against cyclic mechanical stress, ensuring burst pressure margins exceed 4× nominal pressure.
Actuator Interface Standardization
All automated globe valves feature precision-machined top mountings adhering to ISO 5210 (Multi-turn valve actuator attachment) and ISO 5211. Whether deploying pneumatic diaphragm linear actuators or intelligent multi-turn electric servomotors, the concentricity of the stem coupling prevents side-load stem galling.
Fugitive Emissions Control (ISO 15848-1)
In toxic chemical, vacuum, or superheated steam service, stem packing integrity is vital. Our CE certified globe valves integrate die-formed flexible graphite rings with braided carbon yarn anti-extrusion rings and live-loaded Belleville disc spring washers, ensuring helium leakage < 10⁻⁴ mbar·l/(s·mm).
China Factory Supply Chain: In-House Foundry & Elastomer Synergy
Why Tier-1 industrial buyers transition from fragmented valve brokers to direct Chinese manufacturing campuses. Total ownership of casting, rubber compounding, machining, and actuation calibration delivers unassailable commercial and technical reliability.
Overcoming the Third-Party Sourcing Vulnerability
Traditional valve assemblers across Europe and Southeast Asia rely heavily on outsourced foundries and external seal vulcanizers. This distributed tier model creates profound operational risks: hidden metallurgical shrinkages, unpredictable pour porosity, elastomer batch variations, and compounding shipment delays.
Tianjin Top Valve eliminates these systemic bottlenecks. Our consolidated industrial ecosystem unites the Tianjin Donglian Valve Factory (established 1996) and Tianjin Dongfang Rubber Factory (operating since 1987) under unified management. By controlling the entire manufacturing pipeline from pig iron charging to final CE Declaration of Conformity issuance, our facility maintains absolute control over lead times and defect prevention.
- Automated In-House Foundry: Direct induction melting furnace control with spectrographic melt chemistry verification prior to pouring.
- Rubber & Sealing Plant: Custom in-house vulcanization of EPDM, NBR, FKM (Viton), and precision machining of modified PTFE seals.
- Advanced CNC Machining Center: Multi-axis CNC boring and turning centers ensuring concentricity of globe valve seat rings to within 0.015 mm.
- Complete Batch Traceability: Heat numbers cast directly onto pressure boundaries, coupled with permanent QR code electronic serial tracking.
| Production Phase | Standard Sourcing Intermediary | Tianjin Top Valve Integrated Model |
|---|---|---|
| Melt & Casting | Subcontracted; limited chemical melt traceability. | In-house foundry; spectro-verified per ASTM A216/A351. |
| Seat & Disc Trimming | Bought from secondary job shops; high variance. | Stellite No. 6 hardfacing & micro-honed in-house. |
| Elastomers / Packing | Commodity bulk purchase; uncertain shelf life. | Proprietary compounding since 1987 (WRAS/FDA formulas). |
| Actuator Integration | Third-party bracket fitting with alignment skew. | Integrated torque/thrust bench calibration & tuning. |
| Standard Lead Times | 14 - 22 Weeks for Class 300+ builds. | 4 - 8 Weeks for custom actuated assemblies. |
Procurement Sizing & Selection Criteria for Actuator Globe Valves
Actuator globe valves serve critical control functions. Sizing cannot rely on pipe diameter matching alone; precise engineering calculation of flow coefficients, cavitation potential, and dynamic closing thrust is mandatory.
Flow Coefficient (Kv / Cv) Calculation
Proper trim selection requires matching the flow coefficient Kv = Q · √(SG / ΔP) across minimal, normal, and peak flow modes. Linear plugs provide stable throttling across steady flow loops, whereas equal-percentage (EQ%) plugs prevent control oscillation under variable differential inlet pressures.
Actuator Thrust vs. Fluid Delta P
Dynamic shut-off calculation must counter upstream pressure over the unbalance plug area: F_thrust = (A_seat · ΔP_shutoff) + F_packing + F_margin. Top Valve engineers calculate a minimum 1.30× safety factor, preventing thermal expansion binding or partial port opening under sudden fluid surges.
Cavitation & Flashing Mitigation
When the vena contracta pressure plummets below liquid vapor pressure, micro-jets cause destructive pitting. We manufacture multi-stage perforated cage trims that step down velocity pressure incrementally, ensuring liquid pressure remains above vapor pressure throughout the throttling geometry.
| Trim Configuration | Seat Leakage Class (ANSI/FCI 70-2) | Permissible Media Temperature | Best Fit Application Environment |
|---|---|---|---|
| Unbalanced Contour Metal Seat | Class IV (≤ 0.01% of rated capacity) | -46°C to +450°C | High-temperature superheated boiler feedwater, low Kv steam lines. |
| Balanced Cage Guided Metal Seat | Class IV or Class V (0.0005 ml/min/psi/in) | -29°C to +400°C | High differential pressure lines where lower actuator thrust is required. |
| Soft Seated (PTFE/PEEK Insert) | Class VI (Bubble-Tight zero gas leakage) | -50°C to +200°C | Gaseous nitrogen, natural gas, ammonia refrigeration systems. |
| Multi-Stage Cavitation Attenuation Cage | Class V (High integrity shut-off) | -20°C to +350°C | High-head boiler feed pump recirculation, high-pressure water letdown. |
Technological Innovations: Digitalization, Smart Actuators & Predictive Asset Health
Modern plants demand intelligent nodes, not isolated mechanical valves. The integration of microprocessor-controlled smart actuators transforms the globe valve into a predictive data terminal within industrial IoT architectures.
Non-Intrusive Smart Actuation
Modern CE certified electric actuators utilize magnetic Hall-effect encoders to continuously report valve position with 0.1% resolution without requiring physical limit switch contact. Bluetooth/Infrared configuration enables commissioning without breaching explosion-proof IP68 enclosures in ATEX Zone 1/2 environments.
Predictive Torque & Signature Diagnostics
Embedded diagnostic algorithms compare real-time stroke torque profiles against baseline factory calibration curves. Sudden increases in dynamic thrust indicate stem scale accumulation or gland over-tightening; signature degradation highlights seat erosion well before an unplanned outage occurs.
Fieldbus & Wireless Connectivity
Seamless field integration via HART 7, Profibus PA, Foundation Fieldbus, and industrial Ethernet (Modbus TCP/IP, PROFINET). Real-time telemetry including motor winding temperature, cycles elapsed, instantaneous travel speed, and supply pressure status streams directly to enterprise SCADA platforms.
Localized Application Scenarios & Severe Service Performance
Engineered to execute precision regulation across extreme temperatures and hostile media. Below are validated installation environments across major industrial sectors.
Thermal Power Generation & Steam Distribution
In superheated main steam throttling and high-pressure boiler blowdown service, fluid temperatures exceed +450°C at pressures upwards of 100 bar. Our chrome-moly alloy globe valves (ASTM A217 WC6, WC9) feature cobalt-based Stellite hardfacing on seats and discs, effectively counteracting thermal shock, wire-drawing, and high-velocity erosion.
Chemical Refining & Acid Injection
Handling nitric acid, chlor-alkali, or caustic solutions requires superior metallurgical integrity. We machine actuator globe valves from solid forged duplex stainless steel (2205/2507) and Hastelloy C276, equipped with dual PTFE V-ring live-loaded packing to eliminate fugitive atmospheric venting in chemical synthesis parks.
Industrial Refrigeration & Ammonia Systems
Sub-zero anhydrous ammonia and industrial coolant circuits require Class VI zero-leakage shut-off. Top Valve manufactures dedicated straight-through low-temperature ductile iron and stainless globe valves with extended bonnets to prevent ice formation at the gland packing boundary, guaranteeing reliable automated modulation.
District Cooling & HVAC Primary Chiller Loops
Large urban infrastructure and commercial centers utilize actuated globe valves for primary chiller decoupling and variable air volume control. The linear travel characteristic ensures exact water temperature balancing, substantially reducing overall energy consumption across central chiller plant cycles.
High-Vacuum Isolation Systems
In metallurgical vacuum furnaces, semiconductor degassing lines, and vacuum distillation vessels, ordinary valve packings fail due to inward air ingress. Our specialized vacuum globe valves incorporate inverted atmospheric bellows seals combined with secondary O-ring buffers to hold vacuum up to 1.33 × 10⁻⁴ Pa.
Municipal Water Treatment & Potable Networks
Working alongside our certified WRAS-approved butterfly valve product portfolio, actuated globe valves provide micro-throttling at water treatment disinfection dosing stations, coagulant mixing manifolds, and pipeline pressure break stations, maintaining precise hydraulic gradients without water hammer spikes.
Frequently Asked Questions: Technical Sizing, Certification & Delivery
Direct answers to the critical technical and commercial questions reviewed by engineering procurement specialists prior to vendor pre-qualification.
What documentation accompanies a CE certified actuator globe valve shipment from Tianjin Top Valve?
Every commercial order ships with an official technical dossiers packet conforming to European harmonized standards. This includes the statutory CE Declaration of Conformity (DoC) referencing the Pressure Equipment Directive 2014/68/EU Module H, a certified EN 10204 Type 3.1 Material Test Report (MTR) verifying heat chemistry and mechanical properties for body/bonnet/stem, hydrostatic and pneumatic test certificates per EN 12266-1/API 598, actuator bench calibration reports (stroke time, current draw, stroke linearity), and comprehensive Installation, Operation, and Maintenance (IOM) manuals.
How do you prevent stem leakage under cyclic temperature and mechanical fluctuations?
Standard packed glands eventually lose sealing load due to packing consolidation, thermal expansion, and mechanical wear. Top Valve integrates engineered live-loaded packing assemblies utilizing paired sets of precision-tempered Belleville disc spring washers. These springs continuously store mechanical energy, absorbing dimensional shifts and maintaining a constant gland packing stress above the fluid process pressure. Combined with mirror-finished stems (Ra ≤ 0.2 μm) and ISO 15848-1 certified graphite or PTFE packing sets, external fugitive emissions are reliably suppressed.
What are the key advantages of selecting an Actuated Globe Valve over an Actuated Butterfly Valve?
While high-performance butterfly valves excel in large diameter, lightweight, cost-effective on/off isolation and coarse throttling, globe valves are the superior choice for precise linear throttling, severe pressure drops, and anti-cavitation control. Because the globe valve disc travels perpendicular to the seat ring, the annular opening changes proportionally with stem displacement, allowing precise fluid metering. Globe valves also offer a wider selection of specialized trims (perforated cages, multi-step pressure reduction) capable of handling severe pressure letdown and high-pressure steam without trim wire-drawing.
Can your factory supply custom flange drilling standards and face-to-face dimensions?
Yes. Because we own and operate our internal CNC machining centers, our automated globe valves are machined to match global pipeline standards, including EN 1092-1 (PN16, PN25, PN40, PN63, PN100, PN160), ASME B16.5 (Class 150, 300, 600, 900), as well as British BS 4504 and Japanese JIS B2220 standards. Face-to-face lengths adhere strictly to EN 558-1 Series 1/2 or ASME B16.10, ensuring drop-in replacement compatibility in existing piping skids.
What actuator brands, control signals, and fail-safe options are supported?
We provide full automation flexibility. Customers can choose our factory-integrated intelligent electric actuators (supporting 4-20mA, 0-10V, Modbus, Profibus, HART) or specify pneumatic multi-spring diaphragm actuators with electro-pneumatic positioners. Fail-safe mechanics include pneumatic spring-return (Fail-Close or Fail-Open) and electric actuators equipped with supercapacitor or battery backup return systems (Fail-In-Position or Fail-Safe Shut). Additionally, we can mount client-specified third-party actuator brands (e.g., Rotork, Auma, Emerson, Festo) using custom-engineered mounting kits.
How does Tianjin Top Valve ensure on-time delivery for large international project batches?
Our 23,000 m² campus in Dongli District, Tianjin operates with full vertical integration. Raw castings and elastomer seals are produced in-house, eliminating external foundry delays. Furthermore, our strategic proximity to Tianjin Port (one of northern China’s largest maritime container terminals) facilitates rapid customs clearance and immediate loading onto direct vessel lines serving Europe, the Middle East, North America, and Southeast Asia.
Explore Allied Flow-Control Solutions
Engineered in our Tianjin foundry and rubber seat facility to complement automated pipeline systems worldwide.