
Engineered Butterfly Valves & High-Integrity Check Valves
Factory-direct industrial valves verified by rigorous shell and seat leakage testing, manufactured with in-house ductile iron castings and proprietary high-durability elastomeric seals.

CE Certification Micro-Resistance Ball Check Valve
Explore Specification →
Wholesale PTFE Lined Cast Body Butterfly Valve
Explore Specification →
Wholesale Anti-Abrasion Elastic Seat Gate Valve
Explore Specification →
CE Certification Flanged Butterfly Valve - Durable Flow Control
Explore Specification →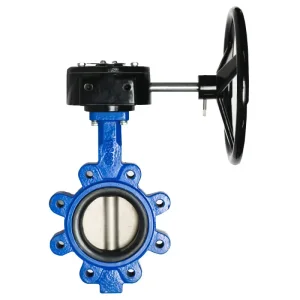
High-Quality Lug Type Butterfly Valve Precision Cast
Explore Specification →
High-Temperature Vacuum Isolation Globe Valve
Explore Specification →
Wholesale Single Flange Butterfly Valve For Pipeline Systems
Explore Specification →
CE Certification Compact Low-Pressure Drop Wafer Lift Check Valve
Explore Specification →The Engineering Excellence of WRAS Approved Butterfly Valves with Worm Gear
WRAS (Water Regulations Advisory Scheme) certification represents the definitive benchmark for water-contact materials in modern piping systems. Coupled with high-torque manual worm gear actuation, these assemblies ensure non-slamming regulation, zero-leakage, and total compliance with human health standards.
Material Toxicity & Microbiological Neutrality
WRAS approval mandates rigorous testing under BS 6920 standards. Our proprietary EPDM seats and epoxy coatings release zero leachates, prevent metallic zinc leaching, and actively resist aquatic microbial biofilm formation, ensuring pure drinking water across municipal lifespans exceeding 30 years.
Self-Locking Worm Gear Actuation
Manual lever actuation on diameters exceeding DN100 poses severe risks of catastrophic water hammer. Our precision heavy-duty worm gearboxes integrate double-lead worms and bronze worm wheels, guaranteeing irreversible mechanical self-locking, smooth fine-throttling control, and IP67 weather sealing.
Concentric vs. Offset Hydrodynamic Profiles
Engineered with streamlined spherical disc contours in Ductile Iron (EN-GJS-450-10) or Stainless Steel (CF8/CF8M), our disc geometry delivers exceptional flow coefficients (Kv values), minimizing systemic pumping head loss while preventing cavitation wear under elevated velocity conditions.
Localized Critical Deployment Scenarios
From water utilities across the UK and the European Union to high-ambient Middle Eastern desalination plants, our worm-gear butterfly valves handle severe operational conditions.
UK & European Municipal Clean Water Grids
Fully conforming to EN 593 and certified via WRAS, our wafer and lug models (4020G, 4325G) are widely standardized in district potable transmission loops, reservoir distribution stations, and underground valve chambers with extended vertical spindles and position transmitters.
Desalination Facilities & Coastal Cooling Circuits
By pairing high-nickel ductile iron or Nickel-Aluminum Bronze (C95800) discs with certified EPDM vulcanization, our assemblies resist pitting corrosion and galvanic attacks caused by aggressive seawater and high-chloride brackish feedwaters up to PN16 / Class 150.
Mission-Critical Data Center Chilled Water Loops
Hyperscale IT cooling demands 100% uninterrupted thermal dissipation. Our worm gear butterfly valves deliver bubble-tight bi-directional isolation, enabling live maintenance on chiller banks, cooling towers, and plate heat exchangers without systemic pressure dips.
Global Commercial Landscape & Valve Industry Trends
Infrastructure renewal policies and urban sustainability goals are transforming global valve procurement expectations toward long-term life-cycle economy.
Aging Pipeline Infrastructure Upgrades
In mature economies across North America and Europe, legacy gate valves with metal-to-metal seating are systematically replaced by resilient-seated butterfly valves. Their compact face-to-face dimensions and one-third lower structural weight minimize retrofit structural engineering costs while cutting installation labor in half.
Regulatory Convergence on Hygienic Standards
With the integration of the revised European Drinking Water Directive (EU 2020/2184) and stringent UK Water Regulations, international suppliers lacking accredited certifications like WRAS or ACS are being excluded from governmental tenders. Audited hygienic safety is now a mandatory commercial prerequisite.
Transition to Automated & Monitored Networks
Modern municipal smart grid designs require manual worm gears to feature standardized ISO 5211 direct-mounting flanges. This ensures that manually throttled valves can later accept smart valve positioning modules, micro-limit switches, or rapid retrofitting into electric actuators without line de-pressurization.
China Factory Supply Chain Resilience & Efficiency Advantages
Operating in Tianjin's industrial manufacturing heartland, our vertically integrated group provides full quality traceability from molten iron to sea-freight container packing.
In-House Foundry (Since 1996)
Operating our proprietary smelting plant eliminates supply bottlenecks. We execute spectrographic chemical analysis per casting heat, validating ductile iron nodularity (>85%) before batch machining.
Polymer Plant (Since 1987)
Tianjin Dongfang Rubber Factory controls compounding, vulcanization, and tensile endurance testing in-house, eliminating elastomeric compression set failures that plague companies buying third-party seats.
CNC Multi-Axis Machining
Automated CNC boring, turning, and facing centers ensure strict dimensional tolerances for flange sealing faces, stem keyways, and disc edges, minimizing seat interference friction while ensuring bubble-tight sealing.
Rapid Tianjin Port Logistics
Situated in Wuxia Industrial Park, our direct access to Tianjin Xingang Port allows container consolidation and flexible maritime scheduling with minimal domestic transit lead times to international destinations.
Technological Roadmap & Future Outlook
Pioneering smart water management, long-life polymer formulations, and net-zero manufacturing standards.
IoT-Enabled Smart Gearbox Diagnostics
Developing low-power Bluetooth and LoRaWAN vibration and torque-sensing modules integrated directly onto manual worm gear housings to enable real-time cavitation warnings, predictive seal wear monitoring, and pipeline asset health dashboards.
Bio-Sourced Drinking-Water Elastomers
Progressing into next-generation rubber polymers synthesized without petrochemical volatile curing agents, lowering carbon footprints while ensuring compliance with anticipated 2030 global non-leaching clean water directives.
Ultra-Low Friction Solid-Film Coatings
Testing nanocomposite surface infusions for disc edges and stem shafts, reducing operating torque by an additional 25%, extending seat sealing longevity beyond 50,000 continuous full-stroke cycles.
Localization Support, Testing Protocols & Regulatory Compliance
Comprehensive project qualification and transparent engineering document packages tailored to meet project audit criteria worldwide.
Comprehensive Multi-Standard Flange Sizing
Valves are engineered to seamlessly align with universal flange drillings including EN 1092-2 PN10/PN16, ASME/ANSI B16.1 Class 125/150, BS 10 Table D/E, and JIS B2239 10K, eliminating mismatch risks for EPC contractors.
100% Hydrostatic Quality Testing
Every single valve undergoes pressure testing per EN 12266-1 / ISO 5208 before release: shell test at 1.5x PN and bubble-tight seat leakage test at 1.1x PN. Complete 3.1 Mill Test Certificates are provided with each dispatched consignment.
On-Demand Digital Engineering Assets
Distributors and consulting engineers receive rapid turn-around access to native CAD files, 3D STEP models, hydraulic flow characteristic curves, and comprehensive material compatibility datasheets within 24 hours.
Complete Fluid Control Valve Inventory
Explore our specialized butterfly and check valve solutions engineered for diverse operating temperatures, aggressive chemicals, and demanding pressure ratings.
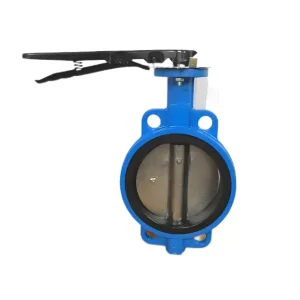
Wholesale Low-Pressure Wafer Type Butterfly Valve
Explore Specification →
High-Quality Grooved Type Manual Butterfly Valve
Explore Specification →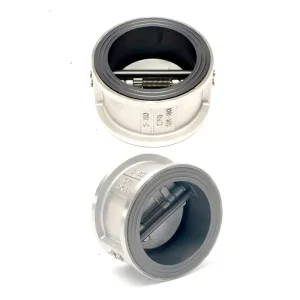
Compact Wafer Lift Check Valve Low-Pressure Drop
Explore Specification →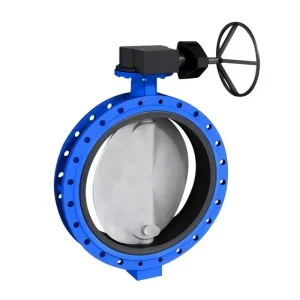
Wholesale High-Quality U-Section Butterfly Valve
Explore Specification →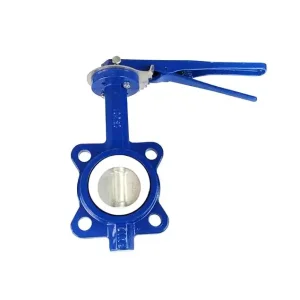
High-Quality PTFE Lined Pinless Butterfly Valve
Explore Specification →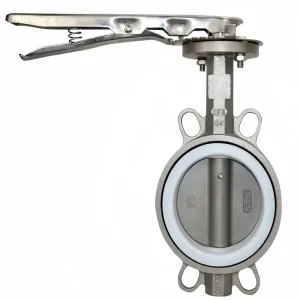
PTFE Lined Stainless Steel Butterfly Valve
Explore Specification →
High-Quality Wafer Check Valve Secure Fluid Control
Explore Specification →
High-Quality Electrical Butterfly Valve Actuation
Explore Specification →Frequently Asked Questions: WRAS Butterfly Valves with Worm Gear
Clear engineering answers addressing specifications, torque calculations, and potable water testing protocols.
