
Critical Isolation & Flow Control Solutions
Featured pressure-rated valves engineered for rigorous high-temperature loops, utility power stations, and municipal transmission lines.

High-Quality EPDM Lining Butterfly Valve - Durable & Corrosion Resistant
View Product Details
Wholesale Single Flange Butterfly Valve - Durable & Efficient Flow Control
View Product Details
Wholesale WRAS Approved Lug Type Butterfly Valve 4325G
View Product Details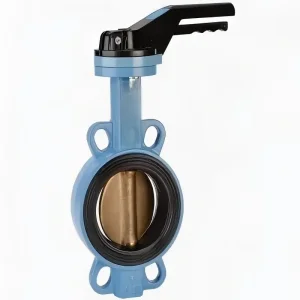
CE Certification Bronze Disc Wafer Butterfly Valve - Durable & Efficient
View Product Details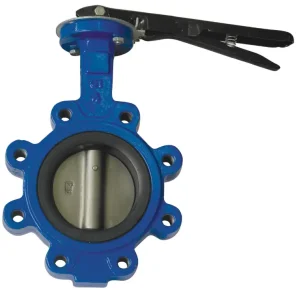
High-Quality Lug Type Manual Operated Butterfly Valve
View Product Details
High-Quality High-Temperature Vacuum Isolation Globe Valve
View Product Details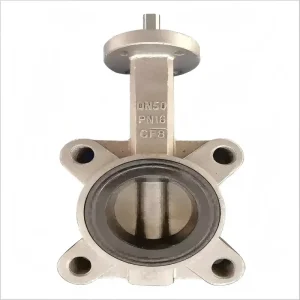
Wholesale Semi Lug Butterfly Valve - Durable & Versatile Flow Control
View Product Details
High-Quality Electrical Butterfly Valve Supplier
View Product DetailsEvolution of High-Pressure Power Station Globe Valves
Analyzing aerodynamic body contouring, creep resistance metallurgy, and sealing mechanics for supercritical (SC) and ultra-supercritical (USC) thermal cycles.
Engineering Core Insight: In modern thermal power plants operating under high pressures exceeding 32 MPa and superheated steam temperatures reaching 610°C, traditional bolted bonnet globe valves suffer from thermal fatigue, cyclic bolt stretch, and catastrophic fugitive bonnet emissions. Next-generation power station globe valves transition exclusively toward self-sealing pressure seal bonnets and forged monoblock body designs conforming to ASME B16.34 standards.
Pressure Seal Integrity
Utilizing internal system line pressure to drive the sealing wedge against the flexible metallic gasket. As thermodynamic fluid force intensifies, gasket seating stress increases proportionately, eliminating the leakage vulnerabilities typical of bolted bonnet connections under extreme transient cycles.
Creep-Resistant Metallurgy
Forged alloy bodies cast from ASTM A182 F91 (9Cr-1Mo-V), F92, and F22 are engineered to mitigate intergranular carbide precipitation and creep rupture over 100,000+ operational hours, guaranteeing high fracture toughness and dimensional stability across supercritical thermal steam lines.
Cobalt-Base Hardfacing (Stellite 6)
Precision Plasma Transferred Arc (PTA) automated welding deposits Stellite 6/21 alloys on both disc faces and integral seat rings. This engineering approach eliminates cavitation pitting, severe throttling wire-drawing, and galling wear during continuous micro-throttling conditions.
| Valve Design Architecture | Nominal Pressure Class | Body Material Specification | Maximum Design Temp | Primary Power Loop Placement |
|---|---|---|---|---|
| Pressure Seal Globe Valve | ASME Class 1500 – 4500 | ASTM A182 F91 / F92 / WC9 | 620°C (1148°F) | Main Steam Isolation, Feedwater Booster |
| Hermetic Bellows Globe Valve | ASME Class 600 – 1500 | Forged F22 / SS316H / Hastelloy | 550°C (1022°F) | Turbine Vacuum Exhaust, Toxic Heat Loops |
| Y-Pattern Slanted Spindle Valve | ASME Class 900 – 2500 | ASTM A217 WC6 / C12A Forged | 595°C (1103°F) | Boiler Blowdown, High Pressure Drain Lines |
| Multi-Stage Cavitation Trim Valve | ASME Class 1500 – 2500 | Monoblock F91 + Hardfaced Core | 565°C (1049°F) | Attemperator Spray, Boiler Feed Pumps |
Worldwide EPC Procurement Dynamics & Valve Requirements
Balancing grid balancing demands, flexible cyclic operation, and ultra-low emission standards across global energy installations.
Daily Peaking (Two-Shift Grid) Fatigue
With renewable power variability (solar/wind), fossil-fired and combined-cycle gas turbine (CCGT) plants now operate under aggressive cyclic start-stop patterns. Globe valves must withstand extreme thermal transients without stem seizure or packing-chamber relaxation.
Stringent Fugitive Emission Compliance
Under ISO 15848-1 Class AH and API 624 standards, procurement engineers reject valves prone to stem seal degradation. Live-loaded packing arrangements with die-formed flexible graphite rings are essential to prevent microscopic steam venting into boiler halls.
Total Cost of Ownership (TCO)
Unplanned power plant outages can incur over $150,000 daily in lost capacity. Sourcing teams prioritize field-renewable seat architectures and modular bonnets that can be refurbished on-site within hours, reducing boiler turnaround windows.
China Industry 4.0: Supply Chain Resilience & Top Valve Infrastructure
Vertical manufacturing integration eliminates quality handoffs between foundry, rubber compounding, machining, and hydrostatic validation.
Vertically Integrated Manufacturing
Founded on an industrial heritage dating back to 1987 (Tianjin Dongfang Rubber) and 1996 (Tianjin Donglian Valve), our 23,000 m² modern manufacturing hub unites foundry casting, proprietary elastomer compounding, precision CNC machining, and inspection under a singular ISO 9001:2015 umbrella.
In-House Spectral & NDT Laboratories
Every high-pressure alloy heat is verified through Optical Emission Spectrometry (OES), Positive Material Identification (PMI), Ultrasonic Testing (UT), and Radiographic Testing (RT) to ensure internal voids, shrinkage, or alloy segregation are rooted out prior to final pressure-shell assembly.
Digitalized Lean Delivery Scheduling
Positioned within the Bohai Rim economic zone in Tianjin, our logistics ecosystem leverages automated ERP scheduling and immediate access to Tianjin Port, trimming typical delivery lead times for specialized power-grade globe valves by 25–40% compared to Western manufacturers.
Localized Engineering Application Scenarios
Specific field configurations where our high pressure power station globe valves solve operational failure modes.
Boiler Continuous Blowdown
Demands severe wire-drawing resistance under critical flashing conditions. Configured with multistage throttling plugs and hardened solid Stellite seats to eliminate erosive degradation across high pressure drops.
Main Steam & Reheat Steam Traps
Operates under extreme high temperatures up to 600°C. Heavy-pattern Y-globe valves reduce pipeline drag coefficient (Cv loss) by 45% while resisting thermodynamic steam thermal shocking.
Feedwater Pump Recirculation
High velocity demineralized water flow prone to cavitation bubbles. Our specialized multi-hole labyrinth disc reduces flow velocity progressively, keeping local pressure strictly above liquid vapor levels.
Turbine Bypass & Extraction Lines
Demands fast zero-leakage isolation to shield the turbine from reverse water ingress or steam condensation shock. Integrated with pneumatic or high-speed electric smart actuators.
High-Performance Power & Industrial Flow Units
Engineered for high chemical resistance, high pressure duty, and tight mechanical shut-off requirements.
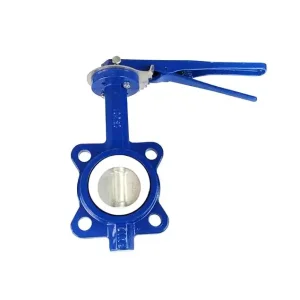
High-Quality PTFE Lined Pinless Butterfly Valve Supplier
View Product Details
CE Certification WRAS Approved High-Performance Butterfly Valve 4020G
View Product Details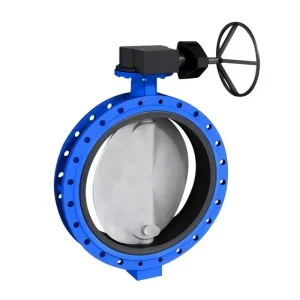
Wholesale High-Quality U Section Butterfly Valve for Reliable Flow Control
View Product Details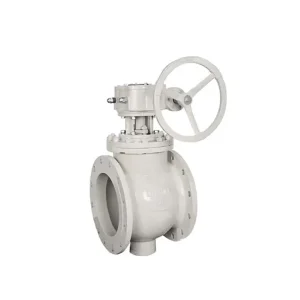
CE Certification High-Pressure Eccentric Plug Valve for Oil and Gas
View Product Details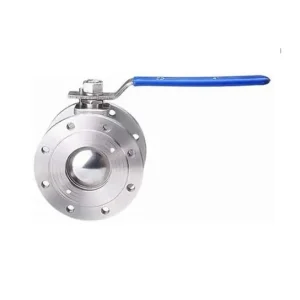
Wholesale Stainless Steel Ultra-Thin Ball Valve with Fire-Safe Design
View Product Details
Wholesale Halar Lined Pinless Butterfly Valve Supplier, Manufacturer
View Product Details
High-Quality Actuator Wafer Butterfly Valve Supplier, Manufacturers
View Product Details
CE Certification Flanged Butterfly Valve - Durable & Efficient Flow Control
View Product DetailsFrequently Asked Questions: High-Pressure Power Station Valves
In-depth engineering answers addressing metallurgy, sealing certifications, pressure classes, and plant retrofit protocols.
