
High-Performance Valves for London Infrastructure
Direct factory supply of resilient flow control hardware engineered for demanding civil networks, district cooling systems, and commercial utilities across London.

London Project Ceramic Disc Wafer Butterfly Valve
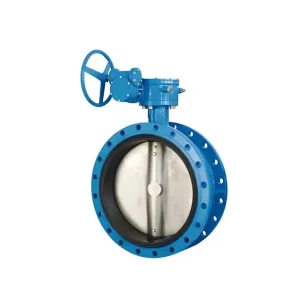
Low-Torque Flanged Butterfly Valve for London Water Systems

Quick-Closing Water Seal Globe Valve - Greater London Specification

Full Rubber Coated Check Valve for London Sub-Surface Networks
Engineering Fluid Control for London’s Dense Urban Fabric
The Greater London industrial and municipal market presents exceptional challenges for pipeline engineers and MEP contractors. With dense metropolitan infrastructure ranging from the Thames Tideway Tunnel to large-scale data center corridors in Slough and commercial skyscrapers in the City of London, valve reliability is directly linked to asset safety and non-revenue water containment.
Valves serving London require uncompromising adherence to stringent UK regulations. Butterfly valves installed in potable water booster plants, chilled-water HVAC circuits, and municipal treatment stations must withstand cyclic pressure shifts, maintain bubble-tight shutoff, and eliminate elastomer degradation caused by aggressive chemical treatment regimens.
- WRAS Compliance (BS 6920): Absolute microbiological inertness and non-toxicity in potable mains.
- EN 593 & BS EN 1092-2: Dimensional interchangeability across wafer, lug, and double-flanged patterns.
- Low Breakaway Torque: Seamless integration with electric and pneumatic actuators, lowering system kWh usage.
Smart Urban Decarbonization Mandates
London’s ambitious target to reach Net Zero by 2030 requires commercial cooling networks and municipal utilities to optimize pumping efficiency. Conventional heavy valves impose high hydrodynamic drag and excessive operational torque.
Our streamlined disc profiles, compounded EPDM seals, and low-friction CNC-finished bearings reduce hydraulic head losses across central London utility substations by up to 18% compared to standard generic castings.
Send Technical RFQ to UK SpecialistsChina Factory 4.0: Supply Chain Agility for Global Contractors
Combining vertically integrated foundries, polymer synthesis, and robotic machining to mitigate geopolitical supply delays and deliver institutional-grade valves directly to the UK market.
Vertically Integrated Foundry
By pouring ductile iron (EN-GJS-400-15/500-7) and stainless steel in-house, we eliminate external casting backlogs. Spectral metallurgical testing ensures nodularity and tensile compliance before machining ever begins.
Dedicated Elastomer Compounding
Unlike competitors relying on third-party rubber suppliers, our dedicated facility (established 1987) manufactures vulcanized EPDM, NBR, and Viton seats engineered to prevent compression set and premature teardown failure.
Predictive Quality & Digital Traceability
Every single valve undergoes digital hydrostatic shell and seat leak testing in strict alignment with EN 12266-1 Rate A (zero leakage). Traceable QR batch IDs guarantee transparency from raw pig iron to project delivery.
Macro Fluid Solutions Engineered for London Sectors
Targeted flow control architectures designed to resolve specific operational challenges across high-density residential developments, maritime locks, and industrial plants.
1. Commercial HVAC & Data Center District Cooling
High-density computing facilities surrounding the M25 ring and modern office towers in Canary Wharf demand zero downtime. Our wafer and lugged resilient-seated butterfly valves deliver exceptional throttling accuracy for chilled water balancing, equipped with ISO 5211 top flanges for direct mounting of Modbus and BACnet actuated controls.
2. Thames Estuary & Marine Operations
Dockside handling, ballast pipelines, and river infrastructure along the River Thames require aggressive corrosion defense. We produce high-tensile Aluminum Bronze (C95800 / CuAl10Fe5Ni5) butterfly valves designed specifically to resist biofouling, cavitation, and chloride pitting.
3. Water Treatment & Waste Regeneration
Modernizing water treatment works along the Lee Valley requires valves capable of handling coagulants, flocculants, and abrasive slurries. Our specialized ceramic disc butterfly valves and PTFE-lined bodies isolate corrosive media entirely from the ductile iron casting, ensuring multi-year service lifespans without unplanned rebuilds.
4. Fire Sprinkler & Standpipe Systems
UK fire safety directives require rapid-assembly grooved and flanged valves with supervisory switches. Our valves deliver low hydraulic friction coefficients, verifying that maximum water pressure is preserved at top-floor riser terminals.
Standard & Engineered Industrial Valves
Examine our full lineup of high-durability valves certified for rigorous industrial and municipal procurement specifications.

London Spec PTFE Lined Cast Body Butterfly Valve
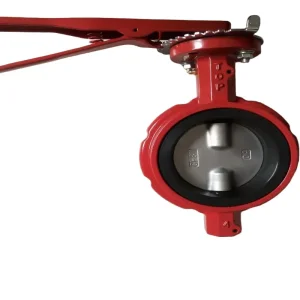
Lugless Semi-Shaft Wafer Butterfly Valve for London Riser Systems
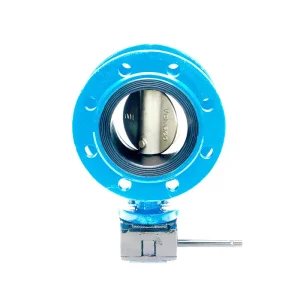
Marine Flange Type Manual Butterfly Valve - Thames Vessel Service

CE Certified Gear-Operated Butterfly Valve - London Plant Spec
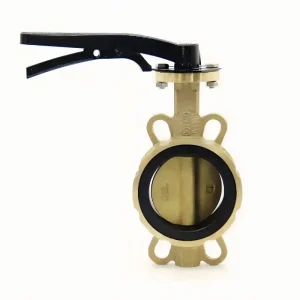
London Seawater Service Aluminum Bronze Butterfly Valve
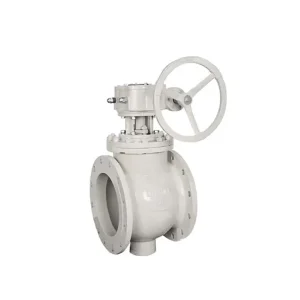
High-Pressure Eccentric Plug Valve for Industrial Petrochemical Duty
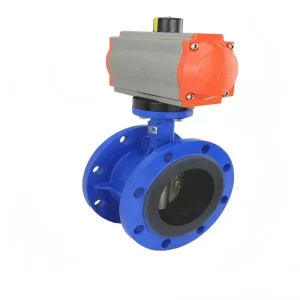
Fast-Acting Pneumatic Lug Butterfly Valve - London Automation Line

WRAS Approved 4020G High-Performance Butterfly Valve
Frequently Asked Procurement Questions
Clear, definitive answers regarding UK certifications, logistics timelines, testing standards, and customization capabilities.
