
High-Performance Industrial Valve Portfolio
Direct manufacturing execution across resilient-seated, lined, and severe-service valves engineered for seamless pneumatic actuation.





The Shift Toward Pneumatic Automated Valving
In high-throughput process piping, the convergence of functional safety, ultra-fast cycle switching, and fugitive emission mitigation is driving enterprise pneumatic valve adoption worldwide.
High-Cycle Response & ESD
Unlike motorized electric gearboxes, pneumatic rack-and-pinion or scotch-yoke actuators provide instantaneous full-bore stroke capabilities under 1 second. This fast-acting response is critical for emergency shutdown (ESD) loops, chemical batch dosing, and compressor surge prevention where delayed actuation creates catastrophic line over-pressurization.
Intrinsically Safe (ATEX) Fluid Loops
In explosive petrochemical vapors, offshore drilling units, and hydrogen gas processing facilities, pneumatic air loops offer native explosion-proof protection without bulky flameproof enclosures. Compressed instrument air inherently eliminates spark propagation risk, reducing CAPEX while achieving complete compliance across Class 1 Div 1 and ATEX Zone 0 environments.
TCO Optimization & Cavity Relief
By pairing precision investment cast bodies with self-relieving seats and live-loaded dynamic PTFE/graphite packing, our pneumatic operated ball valves eliminate unseated torque spikes. The outcome is smaller required actuator frame sizes, lower compressed air consumption, and drastically extended seat longevity across continuous chemical campaigns.
From In-House Foundry Metallurgy to Automated Assembly
Operating dedicated foundry assets since 1996 and proprietary elastomeric polymer compounding since 1987, Tianjin Top Valve guarantees complete metallurgical and functional traceability.
Metallurgical Chemistry Control
Most valve assemblers purchase external castings, risking porosity and brittle grain boundaries under high pneumatic torque. Our Tianjin foundry utilizes spectrometer-verified melts for CF8M, CF3M, WCB, and Duplex 2205 alloys, ensuring tensile integrity and zero defect microstructures before precision CNC machining begins.
Direct ISO 5211 Mounting
Eliminate side-load friction and stem galling. Our valve bodies incorporate integral direct-mount ISO 5211 actuation flanges and dual-D or square precision drive stems. This direct interface removes clumsy brackets and couplers, reducing hysteresis and guaranteeing perfect concentric alignment with pneumatic cylinders.
100% Shell & Automated Leak Testing
Every pneumatic valve assembly undergoes automated testing in accordance with API 598 and EN 12266-1. Actuator breakout torque, running torque, end-position limit switch calibration, and high-pressure nitrogen/hydrostatic bubble-tight shutoff are fully validated and documented with serialized digital MTRs.
Engineered Deployment Across Global Industrial Scenarios
Specific field configurations optimized for demanding regional operating environments and process media.
Chemical & Corrosive Skids
Equipped with Virgin/Reinforced PTFE seats, PFA linings, and SS316L ball trim. Resists chlorinated organic solvents, sulfuric acid manifolds, and aggressive industrial pickling streams without polymer leaching or seal swelling.
Automated Tank Farm Terminals
High-flow 2-piece and 3-piece flanged pneumatic valves engineered for tanker truck bottom loading and bulk fuel unloading. Integrated with spring-return actuators for automated fail-close safe positioning during power outages.
Desalination & Seawater Brine
Aluminum Bronze disc and duplex stainless steel ball cores matched with hard chrome plating. Prevents severe pitting corrosion and marine cavitation typical of high-pressure reverse osmosis (SWRO) reject lines.
Pharmaceutical Clean Utilities
Sanitary cavity-filled TFM1600 seats combined with electro-polished 0.4μm Ra internal bore finishes. Prevents bacterial entrapment in clean-in-place (CIP) and steam-in-place (SIP) biopharma loops.
Strict Global Standards & Local Engineering Support
Ensuring cross-border project compliance with regional pipeline directives, material declarations, and international certifications.
CE & Pressure Equipment Directive (PED)
Our valves fully satisfy European Union PED 2014/68/EU Module H full quality assurance. CE marking guarantees compliance across pressurized gas, liquid group 1 hazardous fluids, and high-temperature steam lines throughout the EU single market.
Potable Water Safety (WRAS / NSF)
For municipal utilities and drinking water infrastructure, our specialized elastomer compounding satisfies UK WRAS and international NSF/ANSI 61 requirements. Formulated without toxic zinc plasticizers, assuring zero heavy metal migration over decades.
Rapid Logistics via Tianjin Seaport
Located in the Wuxia Industrial Park, Dongli District, our production hub enjoys expedited bonded highway access directly to Tianjin Port (Xingang). This strategic export corridor guarantees fast shipping turnaround, standard export crating, and robust shipping documents for clients in over 50 countries.
Next-Generation Valve Automation Roadmap
Strategic engineering developments transitioning fluid control from purely mechanical isolation to AI-assisted predictive diagnostics.
Smart HART / IO-Link Positioners
Integrated micro-transducers monitoring real-time air consumption, actuator chamber pressures, and partial stroke test (PST) decay curves to prevent sticky stem incidents.
Silicon Nitride & Ceramic Internals
Developing ultra-dense structural ceramic ball and seat architectures engineered to resist extreme cavitation and high-velocity abrasive catalyst slurries.
Zero-Bleed Pneumatic Manifolds
Ultra-low leakage directional pilot solenoids and spring returns engineered to reduce clean air generation emissions by up to 34% per operating station.
AI-Assisted Failure Prognostics
Cloud-synchronized operating profiles flagging dynamic seat degradation, temperature-induced torque expansion, and scheduled seal kit replacement intervals.
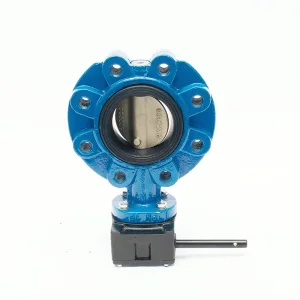
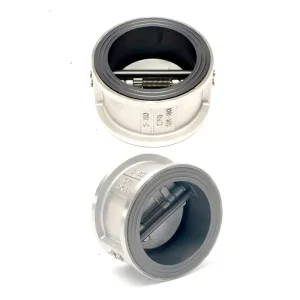
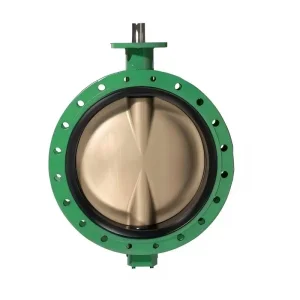
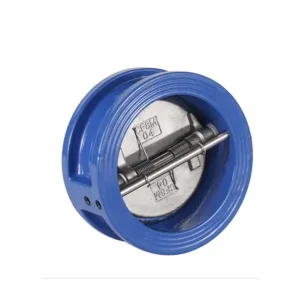
Specialized Heavy-Duty & Check Flow Lineup
Comprehensive plant-wide valves engineered to international ANSI, DIN, and JIS standards for complete pipeline integrity.


Frequently Asked Questions (Pneumatic & Automated Ball Valves)
Expert engineering insights regarding actuator sizing, sizing safety factors, material selection, and direct procurement advantages.
We recommend a 25% safety factor above measured dynamic unseating torque for clean water or light lubricating oils. For dry gas, viscous chemical slurries, or media prone to crystallization, we apply a 35% to 50% sizing safety margin. This ensures break-torque spikes never stall the pneumatic rack-and-pinion pistons even during extended resting intervals.
Double-Acting (DA) actuators utilize plant air supply to drive the pistons in both the opening and closing directions, maximizing torque output while requiring continuous pneumatic signal line integrity. Spring-Return (SR) or single-acting actuators rely on high-durability internal alloy springs to automatically return the ball to a designated Fail-Closed (NC) or Fail-Open (NO) position whenever air pressure is lost.
By executing body casting, rubber seat compounding, and CNC machining within our unified Tianjin campus (Donglian Valve Foundry est. 1996 and Dongfang Rubber est. 1987), we eliminate intermediary supplier surcharges and scheduling bottlenecks. Engineering alterations, custom ISO drilling patterns, and non-destructive examination (NDE) proceed without third-party logistics overhead.
Every delivery includes comprehensive documentation: EN 10204 3.1 Mill Test Certificates verifying body chemical spectrometry and mechanical tensile test values, hydrostatic and pneumatic test certificates (API 598), CE Declaration of Conformity (PED 2014/68/EU), WRAS material declarations (for drinking-water rated resilient seats), and ISO 9001/14001/45001 factory qualification copies.
