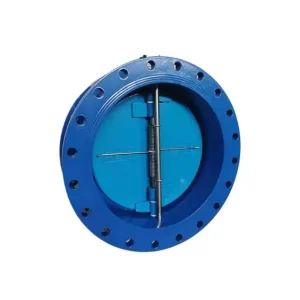
High-Quality Pneumatic Butterfly Valve - Efficient Flow Control Solution Suppliers, Factories
Explore Product
Explore Tianjin Top Valve's factory-direct quarter-turn valves and engineered fluid handling components.
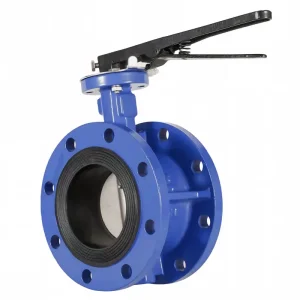
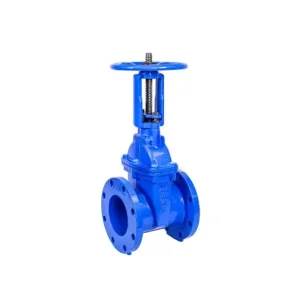

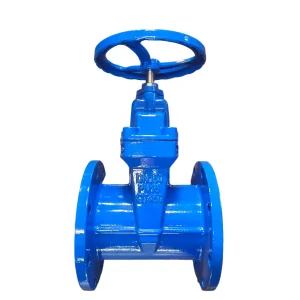

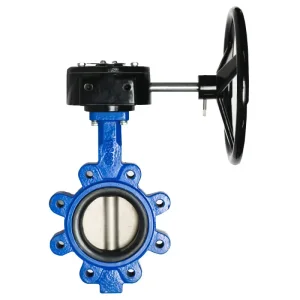
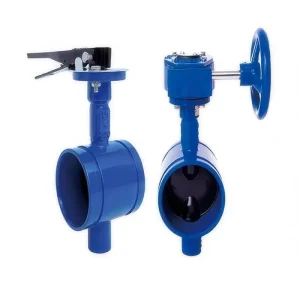
Transitioning from grey cast iron to spheroidal graphite iron: Mechanical resilience in critical fluid infrastructure.
Micro-nodulization treatment with magnesium/cerium transforms brittle flake graphite into round nodules, boosting tensile strength from 200 MPa to over 450 MPa while significantly expanding pressure envelope margins up to PN25 and ANSI Class 150/300.
Ductile iron valve castings receive fusion-bonded epoxy (FBE) electrostatic coating per EN 14901 and AWWA C550. With minimum dry film thicknesses of 250 μm and zero-porosity spark testing, subterranean installations achieve 50-year service lifespans.
Streamlined disc profiles engineered via Computational Fluid Dynamics (CFD) minimize flow separation, reducing the head loss coefficient (zeta) and preventing cavitation, yielding massive cumulative kWh energy savings across municipal pumping stations.
Vertical manufacturing eliminates subcontracting overheads, delivering end-to-end quality assurance and accelerated delivery schedules.
Automated resin-sand and lost-foam molding lines pour GGG40/GGG50 ductile iron with optical emission spectrometry ensuring exact chemical composition and nodularity.
In-house elastomer compounding since 1987 vulcanizes drinking-water safe EPDM, fuel-grade NBR, and Viton seats with precise compression set and Shore A hardness control.
Heavy horizontal and vertical CNC machining centers machine valve seat bores, disc sealing edges, and top flange mounting pads (ISO 5211) down to micron-level tolerances.
Every single valve undergoes bi-directional hydrostatic shell testing at 1.5× PN rating and resilient seat tight-shutoff testing at 1.1× PN per EN 12266-1 and API 598 standards.
Comprehensive engineering reference for piping engineers, procurement managers, and EPC consultants.
| Component | Material Standard | Equivalent Grade | Mechanical / Chemical Advantage |
|---|---|---|---|
| Valve Body | Ductile Iron (EN-GJS-400-15 / 500-7) | ASTM A536 Gr. 65-45-12 / QT450-10 | High tensile threshold, anti-rupture, absorbs pipeline surge and thermal vibration. |
| Valve Disc | DI (Nickel Plated/Epoxy), CF8, CF8M, C63200 | 304 SS, 316 SS, Nickel Aluminum Bronze | Corrosion resistance against chlorinated water, raw sewage, and marine brine. |
| Valve Stem / Shaft | Martensitic / Austenitic SS (416, 420, 304, 316) | 1.4005, 1.4021, 1.4401 | High torsional shear resistance; pinless stem options prevent leak paths. |
| Resilient Seat Liner | EPDM (Drinking Water), NBR (Nitrile), PTFE, FKM | WRAS Approved Elastomer Compound | Zero-leakage bi-directional bubble-tight shutoff (ISO 5208 Rate A); operating: -20°C to +130°C. |
| Anti-Corrosion Surface | Fusion Bonded Epoxy (FBE) Electrostatic Powder | EN 14901 / AWWA C550 / DIN 30677 | Non-toxic, dielectric barrier against soil acidity and aggressive industrial atmospheres. |
| Flange Compatibility | EN 1092-2 PN10/16/25, ASME B16.1 / B16.5 | BS 4504, JIS B2238 10K/16K | Universal wafer centering holes, tapped lug bodies for dead-end, and double-flanged bodies. |
Purpose-built valve trim designs tailored to challenging environmental parameters across 50+ countries.
WRAS-approved resilient seated valves (Models 4020G, 4020L, 4325G, 4325L) with certified non-leaching EPDM seats ensure sanitary compliance for urban drinking supply networks.
Wafer and lug valves mounted with intelligent on/off or modulating 4–20mA actuators regulate chilled water loops and cooling tower cycles with tight thermal control.
Ductile iron bodies fitted with Aluminum Bronze (C95800 / C95400) discs resist pitting, galvanic deterioration, and marine bio-fouling in seawater ballast and intake headers.
Grooved-end butterfly valves engineered for UL/FM-aligned wet/dry fire standpipes, featuring integrated supervisory tamper switches for fast, bolt-free mechanical coupling.
Addressing the shifting demands of EPC contractors, civil utilities, and international valve distributors.
Global procurement teams prioritize valves with ISO 5211 direct-mount flanges compatible with HART, Modbus, and Profibus smart positioners for predictive asset monitoring in digitalized utility plants.
Procurement is pivoting from initial purchase cost to Total Cost of Ownership. Field-replaceable bonded seats, anti-friction shaft bushings, and blowout-proof stem systems significantly lower maintenance downtime.
By eliminating trading intermediaries, international buyers obtain Mill Test Certificates (EN 10204 3.1), custom machining, specialized coating thicknesses, and dependable logistics within tight deadlines.
In-depth responses from our metallurgy, elastomeric sealing, and export logistics team.
Ductile iron contains spheroidal graphite nodules created by magnesium inoculation, yielding double the tensile strength (≥400 MPa vs ~200 MPa) and impact ductility (≥12% elongation vs <1%). This prevents brittle fracture from water hammer surges and mechanical pipeline stresses.
Valve sealing longevity depends on rubber compound purity, vulcanization density, and compression set. Operating our rubber plant since 1987 allows complete control over raw polymer formulations, preventing seat hardening, cracking, and premature leakage.
Wafer valves sit sandwiched between flanges using long tie rods; Lug valves feature threaded bolt holes allowing downstream line disassembly while maintaining upstream pressure; Double-Flanged valves offer rugged structural stability in large diameter lines (DN350 to DN2400).
Every valve undergoes 100% pressure verification according to ISO 5208, EN 12266-1, and API 598. Shell tests occur at 1.5× PN; seat tests occur bi-directionally at 1.1× PN to guarantee zero leakage (Rate A), accompanied by EN 10204 3.1 inspection certification.
Reliable check, ball, and resilient-seated valve configurations for municipal and industrial piping systems.