Primary Engineered Flow Control Catalog
Explore our core API, ASME, and DIN resilient-seated and hard-faced industrial valves manufactured with full material traceability.

High-Quality Buried Elastic Seat Gate Valve for Reliable Flow Control
Inquire Technical Spec
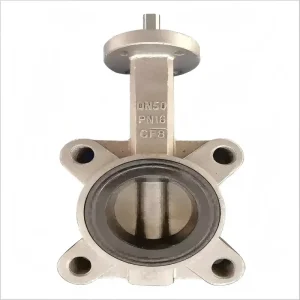
High-Quality WRAS Approved Butterfly Valve Lug Type 4325L Manufacturer
Inquire Technical Spec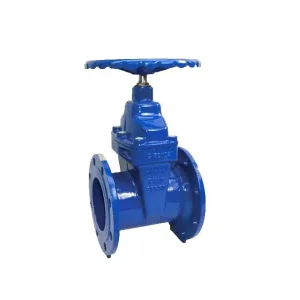
High-Quality Non-Rising Stem Elastic Seat Sealing Gate Valve Factory
Inquire Technical Spec
Wholesale Wafer Butterfly Valve - Durable Flow Control Solution
Inquire Technical Spec
High-Quality Wafer Check Valve for Secure Fluid Control Suppliers
Inquire Technical Spec
CE Certification Gear Operated Butterfly Valve - Durable & Reliable
Inquire Technical Spec
Wholesale PTFE Lined Cast Body Butterfly Valve Suppliers, Factory
Inquire Technical Spec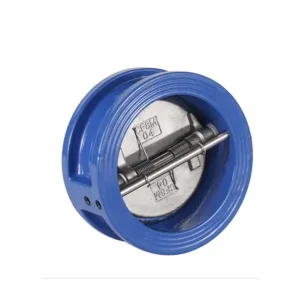
High-Performance Dual Plate Wafer Check Valve for High-Flow Lines
Inquire Technical SpecThe Global Commercial & Industrial Landscape of ANSI Flanged Globe Valves
In modern high-pressure piping architectures, globe valves remain the indispensable standard for fine throttling and linear fluid control where gate and ball valves fall short.
ASME B16.34 Boundary Integrity
Our ANSI flanged globe valves are engineered under strict ASME B16.34 pressure-temperature boundaries. Utilizing high-purity ASTM A216 WCB, ASTM A351 CF8M, and alloy castings, every pressure-retaining wall is structurally modeled via FEA to eliminate thermal deflection under cyclical steam loads ranging from -29°C to 425°C.
Fugitive Emissions Prevention (API 622/641)
Environmental compliance and workplace safety demand ultra-low fugitive emissions. Our deep-stuffing box architectures integrate pre-compressed, graphite-intercalated packing systems combined with dynamic Belleville spring live-loading to maintain helium mass-spectrometer tested seal integrity below 50 PPM.
Severe Trim Aerodynamics & Hardfacing
High-differential fluid passage causes cavitation erosion and wire drawing. We standardly offer API trim configurations including Trim 5 (Full Stellite 6) and Trim 8 (Stellite 6 / 410SS), utilizing automated plasma-transferred arc (PTA) welding to ensure seating surfaces exceed 40 HRC for severe flashing and high-velocity steam.
China Factory Efficiency & Integrated Manufacturing Superiority
Vertical integration removes the trading friction and multi-tier sub-supplier margins that inflate procurement budgets in Western supply chains.
In-House Foundry Control
Operating an independent advanced foundry since 1996, Tianjin Top Valve governs molten metal chemistry directly through real-time optical emission spectrometry (OES). We prevent internal micro-porosity, blowholes, and sand inclusions before rough castings ever touch the machining floor.
Elastomer Plant Heritage
Having established the Tianjin Dongfang Rubber Factory in 1987, our compounding, mold development, and vulcanization for resilient seating (EPDM, NBR, FKM, PTFE) are executed entirely in-house. This complete vertical mastery eliminates premature elastic degradation and compression set failure.
5-Axis CNC Precision
Tolerance mismatches are the leading cause of bonnet stem misalignment and premature gland wear. Our climate-controlled CNC centers machine flange finishes (serrated concentric/spiral 125-250 AARH), seat ring threads, and guide discs to micron-level runout accuracy.
100% Traceable Metrology
From raw ingot spectroscopic analysis to ultrasonic wall thickness verification and API 598 hydro testing, every single valve is permanently marked with an individual heat number and tracked through our ERP. Complete EN 10204 3.1 material test reports accompany every shipment.
Critical Localization & Infrastructure Deployment Matrix
ANSI flanged globe valves provide superior fluid control characteristics across mission-critical industrial duties.
| Operating Sector | Typical Pipeline Medium | Recommended Body & Trim | Specific Flow Function | Applicable Codes |
|---|---|---|---|---|
| Thermal Power Stations | Superheated Main Steam, Boiler Feedwater | ASTM A217 WC6 / WC9 + Stellite Trim 5 | Precise high-pressure bypass and boiler feed throttling | ASME B16.34, IBR, CE/PED |
| Refining & Petrochemicals | Hydrocarbons, Hydrogen, Alkylation Acid | ASTM A216 WCB / A351 CF8M + Trim 8 / 12 | Accurate flow modulation and volatile vapor isolation | API 623, API 600, API 624 |
| Industrial Cryogenics & LNG | Liquid Nitrogen, Methane, Liquid O2 | ASTM A351 CF8 / CF3M + Extended Bonnet | Low-temperature throttling without stem packing freeze | BS 6364, ASME B16.34 |
| Industrial Ammonia Refrigeration | Anhydrous Ammonia (R717), Brine | Ductile Iron / Low-Temp Carbon Steel (LCC) | Hermetic zero-bubble vapor cut-off and regulation | EN 12284, ASME B31.5 |
| Municipal Water Infrastructure | Potable Water, Booster Pump Stations | Ductile Iron GGG50 / WCB + WRAS EPDM/Bronze | Anti-surge throttling and line depressurization | WRAS, AWWA C509, EN 1074 |
Global Megatrends & Procurement Demands in Industrial Valves
How the evolution toward digital asset management, decarbonization, and modular EPC contracting is reshaping valve procurement.
Direct Digital Automation Ready
Modern process control requires smart diagnostic feedback. Tianjin Top Valve manufactures ANSI flanged globe valves with standardized ISO 5211 direct mounting pads. This enables plug-and-play field integration with intelligent pneumatic positioners, 4-20mA HART transmitters, and Foundation Fieldbus loops without custom bracket fabrication.
Total Life-Cycle Cost (LCC) Optimization
Global procurement teams have moved beyond evaluating raw purchase price. An unscheduled shutdown of a steam cracker or high-pressure water header can cost millions per day. Through PTA Stellited hard-facing, rolled stem threads, and modular trim replacements, our globe valves reduce maintenance frequency and total cost of ownership by up to 40%.
Comprehensive ESG & Low-Emission Mandates
With stringent global Net-Zero regulations, valves operating on volatile organic compounds (VOCs) must meet verifiable fugitive emission thresholds. Our API 624 certified graphite multi-ring packings ensure compliance across prolonged cycling tests, providing international contractors with complete environmental vetting proof.
Engineering & Procurement FAQ
Detailed technical responses to core questions asked by EPC project directors and valve reliability specialists.
What is the structural flow difference between an ANSI globe valve and a gate valve?
A gate valve is designed strictly for on/off isolation; positioning a gate disc in a partially open position causes violent fluid turbulence, vibration, and seat erosion. Conversely, an ANSI flanged globe valve forces flow through an S-shaped internal body path with a plug moving parallel to the flow direction. This design allows accurate throttling, stable flow resistance, and precise regulation without seat distortion.
How do you guarantee material integrity against high-pressure steam wire drawing?
Wire drawing occurs when high-velocity wet or superheated steam slips past an imperfect seat interface. We prevent this by utilizing API Trim 5 (solid Stellite 6 overlay) on both the disc and seat ring, achieving a surface hardness of 38-42 HRC. Furthermore, all seat rings are continuously seal-welded to the cast body or machined as integral stellite seats rather than threaded joints that can leak.
Can Tianjin Top Valve accommodate customized flange facings and non-standard drillings?
Yes. Our CNC machining facilities easily execute standard ASME B16.5 Raised Face (RF) 125-250 AARH, Ring Type Joint (RTJ) for Class 600/900/1500 severe duties, Flat Face (FF) for ductile iron piping systems, as well as EN 1092-1 PN16/25/40 and JIS B2220 drillings under direct customer drawing specifications.
What quality testing and traceability documentation do you furnish with export orders?
Every shipment is accompanied by a comprehensive dossier including EN 10204 Type 3.1 Material Test Reports (MTRs) with certified heat analysis, API 598 pressure testing certificates (hydrostatic shell, hydrostatic back-seat, and low-pressure pneumatic seat leak test), non-destructive testing (NDT/RT/UT/MT) reports upon request, and CE/PED compliance declarations.
Specialized Pipeline Infrastructure Solutions
Review our extended portfolio of flanged, lug, and resilient seated process control valves exported to over 50 countries.

Wholesale Single Flange Butterfly Valve - Durable Flow Control Supplier
Inquire Technical Spec
High-Quality EPDM Lining Butterfly Valve - Corrosion Resistant
Inquire Technical Spec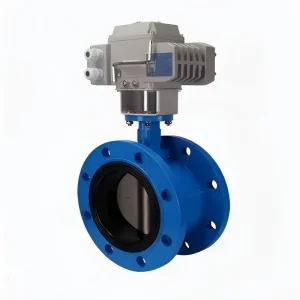
High-Performance Electrical Butterfly Valve for Seamless Control
Inquire Technical Spec
Wholesale Stainless Steel Butterfly Valve - Durable & Corrosion-Resistant
Inquire Technical Spec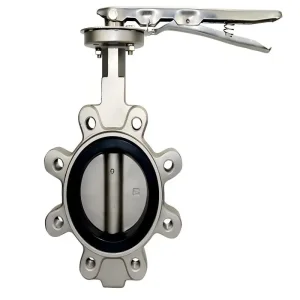
High-Quality LUG Stainless Steel Butterfly Valve - Reliable Supplier
Inquire Technical Spec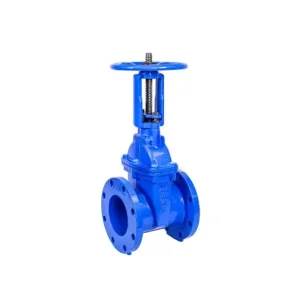
Wholesale Rising Stem Resilient Seat Gate Valve Factory
Inquire Technical Spec
CE Certification Water-Safe Butterfly Valve for Efficient Flow Control
Inquire Technical Spec