
High-Integrity Flanged Butterfly Valves for Sydney Delivery
Direct from our specialized foundry to Port Botany: certified flow control assemblies pre-configured to AS 4087, AS 2129 Table E, and ASME/BS standards.
-
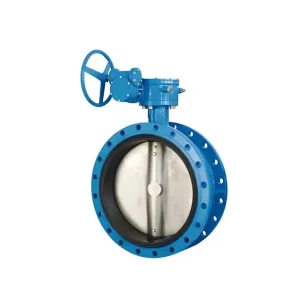
Low-Torque Flange Type Butterfly Valve for Sydney Distribution
Explore Product Details -

Durable & Efficient Flanged Flow Control Valve - Sydney Standard
Explore Product Details -
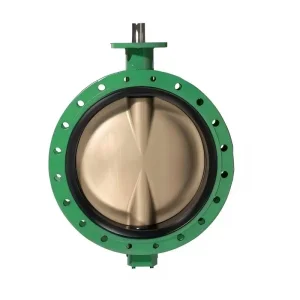
Water-Duty Double Flanged Butterfly Valve for Sydney Utilities
Explore Product Details -

CE Certified Heavy-Duty Flanged Butterfly Valve - Sydney Supply
Explore Product Details
Industrial Context: Flanged Flow Control in Sydney & Global Trade
An engineering analysis of how Sydney’s multi-billion dollar capital expenditure programs intersect with international metallurgical supply chains.
Sydney Commercial & Civil Landscape
Greater Sydney represents one of the Southern Hemisphere’s most demanding fluid handling arenas. With extensive water security initiatives driven by Sydney Water, expansions at the Western Sydney Aerotropolis, and urban upgrades surrounding Barangaroo and Parramatta, infrastructure reliability is paramount.
- Strict AS 4087 & AS 4795 compliance expectations
- Deep ocean outfall and coastal saline resistance
- High demand for pipeline end-of-line isolation capability
Global Metallurgy & Sourcing Shifts
Globally, the flanged butterfly valve sector has shifted decisively toward vertically integrated manufacturing. Engineering procurement houses have moved away from non-integrated brokers, demanding origin validation, raw rubber compounding telemetry, and in-house cryogenic/pressure testing.
- Shift toward EN-GJS-500-7 ductile iron bodies
- Microprocessor-driven vulcanization monitoring
- Mitigation of marine logistics delays via direct factory routing
Modern Industry Evolution & Trends
The valve sector is moving past rudimentary mechanical actuation into smart SCADA-integrated intelligence. For flanged installations where line-stops require major shutdowns, life-cycle durability and low operational torque dominate design considerations.
- Dual-offset & centric geometry optimization
- Low breakaway torque reducing electric actuator size
- Fusion-bonded epoxy (FBE) certified to AS/NZS 4020
Where Our Flanged Valves Operate in Greater Sydney
From deep utility tunnels underneath the Sydney CBD to regional industrial wastewater treatment in Western NSW.
Municipal Potable Water Networks
Installed directly into arterial mains and pumping station headers across Sydney's distribution network. Our double flanged bodies allow independent downstream pipeline disassembly under full working pressure without media leakage.
Seawater Desalination & Marine Ports
Serving Kurnell Desalination Plant auxiliary networks and Port Botany marine bunkering stations. We pair Nickel-Aluminum Bronze (C95800) discs with vulcanized high-grade EPDM/NBR liners to withstand high chloride corrosion.
High-Rise HVAC & Data Centers
Mission-critical district cooling loops for Tier-3 data centers in Alexandria and major commercial towers in North Sydney. Zero-leakage resilience prevents cooling medium loss in mission-critical chiller manifolds.
Vertical Integration: From Raw Foundry to Field-Ready Valves
Understanding why in-house casting and compounding deliver structural reliability that generic suppliers cannot match.
Spectrometric Casting Control
Every melt batch of ductile iron (GGG40/50) is tested via optical emission spectrometry to ensure elongation parameters exceeding 15% and tensile thresholds over 450 MPa.
In-House Rubber Vulcanization
Compounded since 1987 in our proprietary elastomer facility, ensuring exact cross-linking density for zero compression set under 25-bar cyclic loading conditions.
Dual-Flange CNC Machining
Flange faces, bolt-hole drillings (AS 4087 / EN 1092-2), and hydrodynamic disc profiles are finished on 5-axis CNC centers within micro-tolerances.
1.5x Hydrostatic Pressure Test
100% of manufactured units undergo hydrostatic shell (1.5x PN) and pneumatic/water seat (1.1x PN) inspection with recorded leak test charts prior to maritime packaging.
Standardizing Flow Solutions for NSW Projects
Are you drafting an EPC tender, water utility upgrade, or industrial distribution expansion in New South Wales? Our bilingual engineering division provides full drawing packages, flange compatibility assessments, and factory-direct pricing schedules.
Comprehensive Flanged & High-Performance Valve Collection
Complete valve configurations engineered for seamless integration into Sydney municipal and commercial piping installations.
-
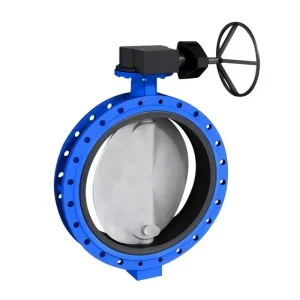
High-Quality U-Section Flanged Butterfly Valve - Sydney Distribution
Explore Product Details -

Compact Single Flange Butterfly Valve - Sydney Mechanical Systems
Explore Product Details -
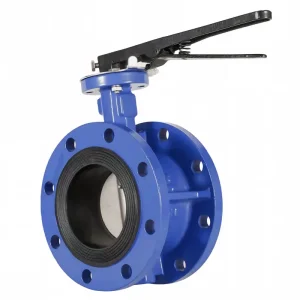
Lever-Actuated Flanged Butterfly Valve for Rapid Sydney Isolation
Explore Product Details -
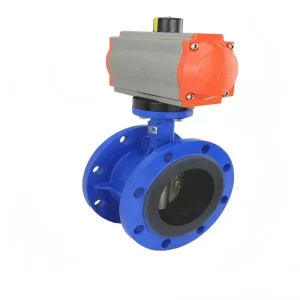
Pneumatic Actuated Flanged Butterfly Valve for Sydney Plant Automation
Explore Product Details -
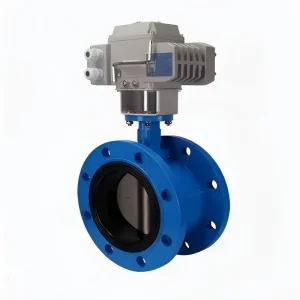
Intelligent Electric Actuated Butterfly Valve - Sydney SCADA Ready
Explore Product Details -

Wafer Check Valve Anti-Backflow Asset - Sydney Pumping Stations
Explore Product Details -
Pneumatic Control Lug & Flanged Valve - Sydney Treatment Lines
Explore Product Details -
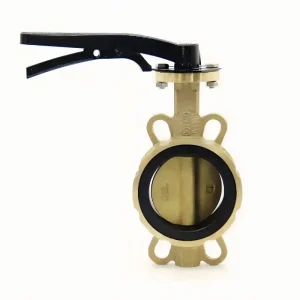
Aluminum Bronze Marine Butterfly Valve - Sydney Harbour Marine
Explore Product Details
Frequently Asked Questions: Sydney Specifications
Clear, engineering-level answers regarding flange standards, rubber compounding, coatings, and import processes into Australia.
Can you drill flanges to Australian Standard AS 4087 and AS 2129 Table E?
Yes. While international projects frequently request EN 1092-2 PN10/PN16 or ASME B16.5 Class 150 drilling, our automated CNC machine centers routinely execute AS 4087 Figure B5/B6 drilling patterns, as well as classic AS 2129 Table D and Table E patterns for seamless connection to Australian pipelines.
What is the primary operational advantage of a flanged butterfly valve over wafer styles?
Double flanged butterfly valves feature integrated full-face flanges on both ends. This design allows the valve to be securely bolted to the pipeline on either side independently, enabling safe dead-end isolation and pipe maintenance downstream without having to drain or depressurize the upstream system.
How does your factory manage elastomeric seal longevity?
Unlike competitors who source liners from third-party market traders, our corporate parent has manufactured technical rubbers since 1987. We compound our own EPDM, NBR, and Viton in-house, ensuring precise sulfur-cured or peroxide-cured chemistry with minimal compression set and certified potable-water compliance.
What external anti-corrosion protection is provided for Sydney coastal soil?
For aggressive coastal Sydney conditions or buried utility trenches, we apply electrostatically deposited fusion-bonded epoxy (FBE) powder coatings with an average thickness of 250 to 300 microns, verified with porosity pinhole testing at 1.5 kV to prevent cathodic delamination.
What is the standard manufacturing and shipping lead time to Port Botany?
Standard casting and machining cycles for DN50 to DN600 run within 20 to 30 calendar days. Maritime freight from Tianjin Port directly to Sydney's Port Botany typically takes 16 to 22 transit days, with full customs clearance and export packing handled efficiently.
Are actuators interchangeable on your flanged valves?
Yes. All of our flanged butterfly valves are built with standard ISO 5211 top-mounting flanges and standardized square or keyway stems. This ensures universal interchangeability with manual worm gears, pneumatic double-acting/spring-return actuators, or smart electric actuators without field modification.
