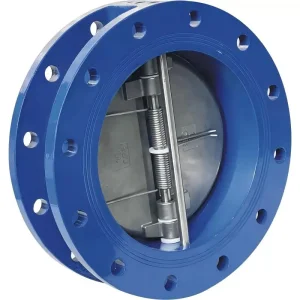
High-Integrity Butterfly Valves for Czech Industrial Applications
Engineered for precision flow control, rapid mechanical grooved coupling, and long service life under mechanical vibrations common in automotive plants and manufacturing centers.

Czech Republic Spec: Manual Grooved Butterfly Valve
High-Quality Grooved Type Manual Butterfly Valve Suppliers, Manufacturers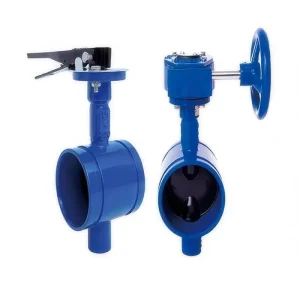
Czech Republic Spec: Reliable Grooved End Butterfly Valve
High-Quality Grooved End Butterfly Valve - Durable & Reliable Flow Control Suppliers, Supplier
Czech Republic Water Grid: Resilient EPDM Butterfly Valve
High-Quality EPDM Lining Butterfly Valve - Durable & Corrosion Resistant Suppliers, Manufacturers
Czech Industrial Chemical: Ceramic Disc Butterfly Valve
Wholesale Ceramic Disc Wafer Butterfly Valve - Durable & Efficient Design Supplier, FactoriesCommercial Dynamics of Grooved Valves in the Czech Republic
Understanding the engineering standards, building codes, and macroeconomic factors driving the adoption of grooved end butterfly valves across Central European mechanical engineering hubs.
Automotive & Heavy Machinery Base
The Czech Republic, boasting heavy manufacturing concentrations across Mladá Boleslav, Kvasiny, and Kolín, enforces high standards on manufacturing cooling circuits and robotic welding chiller loops. Grooved-end butterfly valves reduce downtime significantly compared to flanged alternatives because mechanical couplings absorb thermal vibration without flange gasket creep.
Skilled Labor Deficits in EU Construction
With wage pressure and shortage of certified European pipe welders, Czech mechanical contractors are transitioning fast toward grooved mechanical piping systems. Grooved installations require no open flame or post-weld X-ray inspection, accelerating high-rise HVAC and logistics warehouse pipeline assembly by up to 65% in man-hours.
Stringent EN 12845 & ČSN Regulations
Automatic fire sprinkler networks across modern logistics parks near Brno and Ostrava must strictly comply with ČSN EN 12845 fire safety codes. Grooved butterfly valves with integrated supervisory tamper switches provide positive visual and electrical status indications directly to central building automation units.
Engineered for Demanding Czech Operating Environments
From deep mine dewatering in Northern Moravia to advanced district heating in Prague, our grooved butterfly valves withstand challenging temperature swings and hydraulic shocks.
Prague & Brno District Heating Sub-Stations
In centralized urban thermal exchange hubs, grooved butterfly valves with molded high-temperature EPDM seats sustain cycling temperatures from -10°C in winter peaks up to +120°C in pressurized recirculating water loops, eliminating stem packing leaks.
Chemical & Pharmaceutical Complexes
At processing plants throughout the Ústí nad Labem chemical basin, our valves equipped with PTFE or Ceramic linings handle corrosive cleaning washdowns and harsh acidic media without elastomer degradation or metal embrittlement.
Logistics & Automated Distribution Warehouses
The Czech Republic acts as the logistics hub of Central Europe. Our signal grooved valves operate seamlessly in dry-pipe and wet-pipe sprinkler risers, carrying UL/FM equivalence alongside CE markings for immediate fire marshal commissioning.
| Parameter | Tianjin Top Valve Spec | Standard European Requirement | Engineering Benefit |
|---|---|---|---|
| Nominal Diameters | DN50 – DN300 (2" – 12") | EN 593 / ISO 5752 | Full pipeline dimensional compatibility across Czech metric & imperial installations |
| Working Pressure | PN16, PN20, PN25 (Up to 300 PSI) | EN 12266-1 / PED 2014/68/EU | Safety factor exceeding 1.5x test pressure for water hammer absorption |
| Body & Disc Casting | Ductile Iron EN-GJS-450-10 / CF8M (316 SS) | EN 1563 / EN 10213 | Superior tensile strength preventing groove deformation under pipeline settlement |
| In-House Elastomers | EPDM (WRAS grade) & High-Purity NBR | BS 6920 / EN 681-1 | In-house compounding since 1987 guarantees minimal compression set and zero bubbling |
| Groove Standard | AWWA C606 / ISO 6182 Standard Cut/Roll | ISO 6182-1 | Exact compatibility with standard Victaulic, Tyco, or Viking mechanical couplings |
Direct-from-Foundry Value for European Procurement Teams
Combining the cost efficiency and scale of Tianjin's industrial manufacturing heartland with full European material traceability and engineering documentation.
Vertically Integrated Foundry Control
Unlike trading companies that rebrand unverified castings, Tianjin Top Valve operates its own foundry (operating since 1996) and elastomer compounding plant (since 1987). Every batch of ductile iron is spectrographically checked before casting, preventing porosity under PN25 hydrostatic pressures.
Complete EN 10204 3.1 Certification
Czech civil engineers and project authorities require rigorous compliance documentation. We issue chemical composition, mechanical elongation, and pressure hydro-test certificates for each serial batch, ensuring unhindered EU project acceptance.
Predictable Eurasian Freight Corridors
Located near Tianjin Port with seamless intermodal connections via Hamburg/Koper ports and direct China-Europe freight trains into Central Europe, we ensure steady project delivery schedules for large framework contracts.
Engineering & Procurement FAQ for Czech Buyers
Key technical details regarding groove geometry, actuation matching, European standards compliance, and lead-time guarantees.
Are your grooved dimensions compliant with Czech and EU piping couplings?
Yes. Our grooved end butterfly valves follow AWWA C606 and ISO 6182 cut and roll groove specifications. They integrate seamlessly with standard grooved couplings used throughout the Czech Republic, including Victaulic, Tyco Grinnell, and Viking systems.
Can you provide factory-mounted electric or pneumatic actuators with local voltages?
Yes. All valves can be configured with ISO 5211 direct-mount actuator flanges. We equip them with 230V/400V AC 50Hz electric actuators or double-acting pneumatic actuators fitted with ATEX/CE explosion-proof switchboxes as specified for European installations.
How does your factory ensure bubble-tight sealing on resilient seats?
Because our sister factory has compounded technical rubber since 1987, we formulate our EPDM and NBR compounds internally. Discs are polished to mirror finishes, and 100% of finished valves undergo bidirectional hydrostatic and low-pressure air seat tests before packaging.
What is the typical transit lead time to Prague, Brno, or Ostrava?
Standard production runs require 20–30 days. Sea shipping from Tianjin Port to European transshipment ports (Hamburg or Koper) takes approximately 28–35 days, followed by rapid bonded rail or road transport directly to Czech industrial logistics parks.
Precision Flow Control Line for Central European Infrastructure
Explore our complete product lineup engineered to European pressure vessel standards, complete with WRAS potable water approvals, CE markings, and resilient sealing.

Czech Republic Building Code: Fire Signal Butterfly Valve
Wholesale Fire-Fighting Wafer Signal Butterfly Valve Supplier, Factory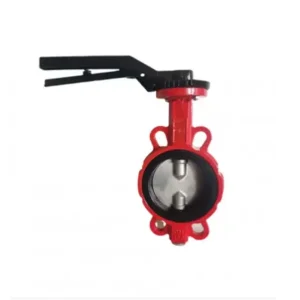
Czech Heavy Industry: Double Half Shaft Butterfly Valve
High-Quality Double Half Shaft Wafer Butterfly Valve Supplier, Manufacturer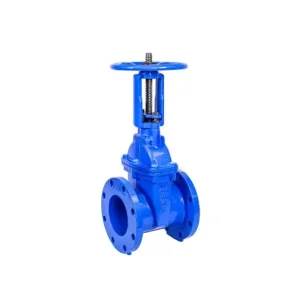
Czech Municipal Water: Rising Stem Resilient Gate Valve
Wholesale Rising Stem Resilient Seat Gate Valve Supplier, Factory
Czech Project Heavy: Grooved End Butterfly Valve
High-Quality Grooved End Butterfly Valve - Durable & Reliable Flow Control Suppliers, Supplier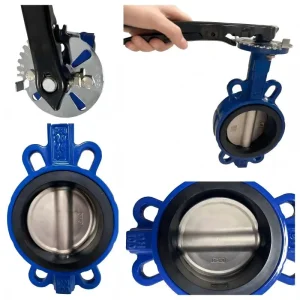
Czech Potable Water: WRAS Butterfly Valve 4020L
High-Quality WRAS Approved Butterfly Valve - High Performance & Durability 4020L Supplier, Manufacturers
Czech Emergency Systems: Quick 3-Way Flanged Ball Valve
CE Certification Quick - Opening Three - Way Flange Ball Valve for Emergency Fluid Diversion Supplier, Factory
Czech Smart Building: Electrical Motorized Butterfly Valve
High-Quality Electrical butterfly valve Supplier, Manufacturer