
Critical Isolation & Throttling Solutions for Pakistan
Advanced globe valve architectures configured for high thermal stress, high-pressure utility boilers, industrial refrigeration, and localized process duties across Karachi, Lahore, Faisalabad, and Multan.
-
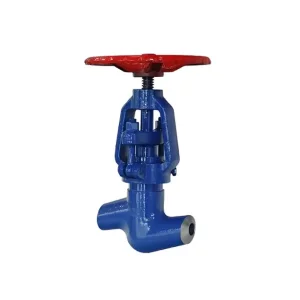
High-Quality High Temperature And High Pressure Power Station Globe Valve Manufacturers, Manufacturer
-

High-Quality High - Temperature - Vacuum Isolation Globe Valve for Vacuum Heat Suppliers, Factory
-

Wholesale Straight-Through Ammonia Globe Valve Manufacturers, Factory
-

High-Quality Water Seal Globe Valve with Quick - Closing Feature Manufacturers, Manufacturer
Industrial Landscape & Fluid Control Requirements in Pakistan
Navigating operating realities across energy corridors, chemical sectors, and expanding municipal supply routes.
The industrial economy of Pakistan is undergoing rapid capital transformation, accelerated by structural investments in the China-Pakistan Economic Corridor (CPEC), thermal plant modernizations under IPP frameworks, and the revitalization of heavy processing clusters in Punjab and Sindh. Fluid handling environments in Pakistani facilities present a punishing matrix of operating conditions: severe thermal cycling, pervasive sand and dust ingress, erratic feedwater water hardness, and variable pipeline operating pressures.
In high-pressure steam distribution, fertilizer synthesis (notably urea plants throughout Multan and Sheikhupura), and processing hubs around Karachi’s Port Qasim, valves encounter severe cavitation and flashing. Standard commercial-grade valves experience premature seating degradation, packing gland erosion, and stem galling under these dynamic stresses. Consequently, plant managers and procurement leads are migrating toward ASME Class 150 to Class 2500 forged and cast globe valves that incorporate Stellite hardfaced seat trims, pressure-seal bonnets, and fugitive emissions-certified gland packings conforming to ISO 15848-1 and API 622.
Engineered Sector Solutions: Meeting Pakistan's Rigorous Operational Standards
Field-proven valve architectures engineered for extreme process regimes across energy, agro-industry, and process lines.
Thermal & Combined-Cycle Power
Superheated steam handling up to 570°C requires chrome-moly body castings (ASTM A217 Gr. WC6, WC9) and pressure-seal bonnets that utilize line pressure to reinforce the seal, eliminating high-pressure boiler feed pump bypass leakage.
Fertilizers & Petrochemicals
Fertilizer facilities utilizing ammonia synthesis gas require deep vacuum isolation and hermetic sealing. Straight-through globe valves with extended bonnets and PTFE/Graphite composite seals stop hazardous ammonia emissions.
Textile Processing & Finishing
High-volume processing in Faisalabad and Karachi requires rapid throttling and frequent cycling on dye-bath steam circuits. Balanced plug trims reduce operating torque and minimize line water hammer during rapid shutoff sequences.
Global Supply Chain Realities & Technical Roadmap
Balancing capital expenditure with whole-life asset reliability through material science and smart actuation.
Shift From Commodity Valves to Performance-Class Solutions
International procurement frameworks are rapidly discarding non-traceable, unregulated valve assemblies. EPC engineering teams executing projects across developing corridors now insist on EN 10204 Type 3.1 material traceability certification, verified positive material identification (PMI), and pressure containment ratings audited under ISO 9001 quality systems. With life cycles expected to surpass 15–20 years in heavy processing plants, total cost of ownership (TCO) calculations favor valves engineered with replaceable seats, non-rotating burnished stems, and cobalt-based hardfacings.
AI-Driven Manufacturing, CNC Machining & Smart Diagnostics
Modern flow control requires zero-leakage tolerances. We deploy multi-axis CNC machining suites to turn stem threads, seat angles, and disc contours down to micron tolerances. Looking to the immediate future, industrial valves serving critical nodes in Pakistan are integrating smart electro-pneumatic positioners equipped with HART and Modbus telemetry, giving plant operators predictive diagnostic data on gland packing friction, disc wear, and seat stroke fidelity before unplanned trips occur.
Localized Support & International Compliance Assurance
End-to-end quality validation designed to satisfy Pakistan engineering consultancies and international EPCs.
Full Standard Harmonization
Valves are engineered to conform to ASME B16.34, BS 1873, API 600, API 623, and DIN EN specifications. Face-to-face dimensions strictly follow ASME B16.10, ensuring drop-in replacement across brownfield infrastructure.
Third-Party Inspection (TPI)
We routinely facilitate third-party witness inspections via international agencies (SGS, BV, TÜV, Lloyd's Register) for raw material metallurgy, radiography, dye penetrant checks, and hydro testing prior to Karachi port shipment.
Logistics & Port Qasim / Karachi Transit
Our Tianjin industrial base provides direct multimodal maritime connections to Karachi Port and Port Muhammad Bin Qasim. Valves are sealed in vacuum-sealed moisture wraps and heavy export sea crates to protect against maritime humidity.
Frequently Asked Questions: Industrial Globe Valves for Pakistan
Direct technical responses addressing engineering specifications, flange standards, and procurement criteria.
Which body materials are recommended for power station steam systems in Pakistan?
How do globe valves compare to gate valves in throttling applications?
Are flange ratings compatible with both British Standard and ANSI installations?
What measures protect ammonia globe valves against atmospheric fugitive emissions?
Consult Our Valve Engineering Specialists
Send us your line sizes, pressure classes, temperature ranges, and medium specifications. Our engineering team will review your data sheet and return 2D/3D CAD models, material trace certifications, and quotation within 24 hours.
Send Inquiry Now →Complementary Fluid Control Lineup for Industrial Pipeline Networks
Comprehensive array of high-pressure check valves, high-performance butterfly valves, and resilient-seated gate solutions.
-

CE Certification Compact Low-Pressure Drop Wafer Lift Check Valve Supplier, Factories
-

Wholesale CE/ISO/DIN/BS High Pressure Metal Seal Hard Seal Butterfly Valve Manufacturers, Manufacturer
-
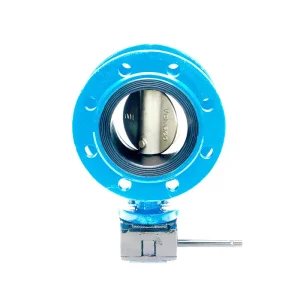
High-Quality Marine flange type manual operated butterfly valve Supplier, Manufacturers
-

High-Quality Grooved Type Manual Butterfly Valve Suppliers, Manufacturers
-

Wholesale Full Rubber Coated Check Valve Supplier, Factories
-
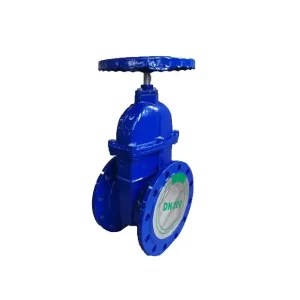
CE Certification German Standard Elastic Seat Gate Valve Manufacturers, Manufacturer
-
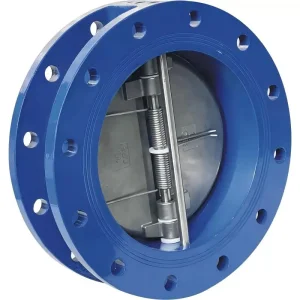
CE Certification Dual Plate Check Valve, Reliable Backflow Prevention Device Suppliers, Manufacturer
-

CE Certification Duplex Type Pinless Butterfly Valve Factories, Factory
