
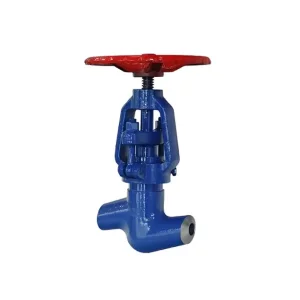
Caspian Critical Duty Models
Primary Industrial Valve Solutions for Azerbaijan
Field-proven globe valves configured for petrochemical refining, high-enthalpy thermal generation, and aggressive utility infrastructure in the Baku-Tbilisi-Ceyhan energy corridor.

High-Quality High - Temperature - Vacuum Isolation Globe Valve for Azerbaijan Refineries & Vacuum Heat Systems
Explore Specification
Wholesale Straight-Through Ammonia Globe Valve for Azerbaijan Chemical Processing & Industrial Cold-Chains
Explore Specification
High-Quality Water Seal Globe Valve with Quick - Closing Feature for Absheron Regional Water Trunklines
Explore Specification
Market Dynamics & Infrastructure
Industrial Landscape of Azerbaijan & Fluid Control Dynamics
The Republic of Azerbaijan represents a cornerstone of the Southern Gas Corridor, bridging vast energy reserves with European consumer markets. The country's infrastructure relies heavily on mission-critical flow isolation systems.
High-Pressure Energy Corridors
With major pipeline trunks such as the South Caucasus Pipeline (SCP), Sangachal Terminal expansions, and offshore platforms in Shah Deniz and Azeri-Chirag-Gunashli (ACG), operating environments demand CE-certified globe valves capable of withstanding cyclic thermal stresses, micro-vibrations, and high differential pressures without stem packing leakage.
Downstream Petrochemical Shift
SOCAR's modernizations at the Heydar Aliyev Baku Oil Refinery and the Azerikimya Production Union require specialized throttling globe valves. Media containing aromatic hydrocarbons, aggressive sour condensates, and catalytic cracking gases require high-grade metallurgy, including Monel trims, Stellite hardfacing, and Duplex steels.
Decarbonization & Green Transition
Following Azerbaijan's hosting of COP29 and national strategies for energy efficiency, regional power plants (such as the Mingachevir and Shimal combined-cycle facilities) are upgrading high-pressure steam bypassed loops to minimize enthalpy losses and fugitive methane/carbon emissions.
100%
PED 2014/68/EU Module H Traceability
Class 2500
Maximum Pressure Rating Engineered
ISO 15848-1
Low Fugitive Emission Compliance
< 0.01%
Allowable Seat Leakage Rate (Class VI)
Engineering Excellence
Macro Flow Control Solutions: CE PED Globe Valve Architecture
A comprehensive technical breakdown of how our globe valves address thermal cycling, cavitation erosion, and stem galling in continuous processing facilities.
Hydrodynamic Plug Profiles & Trim Topologies
Linear isolation valves often succumb to wire-drawing and seat scrubbing under tight throttling duties. Our globe valves integrate tailored plug designs: Parabolic Throttling Plugs for linear control, Perforated Cage Trims to dissipate acoustic energy and mitigate cavitation during severe pressure breakdowns, and Flat Face Shut-off Discs with satellite overlay (CoCr-A) to resist micro-particulate scouring typical of Caspian basin raw untreated crudes.
- Zero chattering due to upper/lower guided valve plugs
- Hardened seating faces: Stellite 6, Monel K500, or Nitride hardened 410 SS
- Balanced trim designs minimizing actuator torque under high differential pressure
Fugitive Emission & Pressure Containment Integrity
Meeting European CE standards requires absolute pressure containment integrity under EN 12516, ASME B16.34, and BS 1873. Our forged and cast valve bodies undergo finite element analysis (FEA) to confirm wall thickness margins under seismic loads and pressure surge conditions.
- Pressure seal bonnet architecture for Class 900 to Class 2500 services
- Die-formed flexible graphite rings with braided anti-extrusion carbon packing
- Full conformity with TA-Luft / ISO 15848-1 Class AH emission thresholds
Operational Assurance
Localized Support, Regulatory Compliance & Caspian Logistics
Overcoming cross-border technical barriers through rigorous quality assurance, customized documentation, and established transport routes directly to Baku, Sumgayit, and Ganja.
CE & International Certification
Procurement teams in Azerbaijan operating under foreign joint ventures (BP, TotalEnergies, Equinor) require strict adherence to international norms. We supply complete EN 10204 3.1 / 3.2 Material Test Certificates (MTC), NDT dossiers (Radiographic, Ultrasonic, Magnetic Particle), and PED Module H CE certification valid across trans-national pipeline projects.
Caspian Climate & Soil Adaptation
Atmospheric conditions along the Caspian shoreline present saline, windy, and semi-arid conditions that induce rapid external chloride stress corrosion. Our globe valves feature marine-grade epoxy coatings (minimum 300 microns C5-M compliant) or thermal spray aluminum (TSA) treatments to guarantee decades of atmospheric exposure survival without degradation.
Direct Logistics via Middle Corridor
Utilizing the multimodal Trans-Caspian International Transport Route (TITR) and accelerated air cargo to Heydar Aliyev International Airport, we ensure predictable supply lines, minimizing downtime during turnaround events and scheduled plant shutdowns across Absheron and Mingachevir industrial parks.
Application Casebooks
Localized Application Scenarios in Azerbaijan's Industrial Clusters
Targeted flow control implementations solving specific process challenges across regional production nodes.
Baku Refining Hub
High-Temperature Hydrocracker Loops
Deployment of Stellite-faced, high-pressure forged globe valves in catalytic cracking fractionators. Zero packing blowout ensures compliance with strict environmental leak-detection and repair (LDAR) initiatives.
Sumgayit Chemical Park
Industrial Ammonia & Urea Synthesis
Specialized straight-through ammonia globe valves engineered with PTFE/Graphite composite disc inserts and zero-leakage back-seating arrangements, supporting fertilizer and polymer intermediate manufacture.
Caspian Offshore Tie-backs
Seawater Lift & Injection Services
Super Duplex (UNS S32750) and Nickel-Aluminum Bronze globe valves engineered to regulate high-pressure seawater injection wells, completely eliminating crevice corrosion and pitting from hyper-saline Caspian brine.
Future Engineering
Technology Roadmap: Smart Actuation & Decarbonized Flow Control
How next-generation valve manufacturing anticipates the digital transformation and hydrogen readiness of the Caspian basin.
Predictive Diagnostics & IoT-Enabled Positioners
Integration of HART and Foundation Fieldbus intelligent digital valve positioners on globe throttling systems. Real-time stem friction profiling, partial stroke testing (PST), and acoustic emission sensors detect cavitation or internal wire-drawing before catastrophic failure occurs, enabling predictive maintenance during planned maintenance turnarounds.
Hydrogen & Clean Fuel Blending Readiness
As Azerbaijan explores green hydrogen integration through the Southern Gas Corridor, our R&D division tests globe valve metallic microstructures against high-pressure hydrogen embrittlement. Certified low-stress concentration body geometry, specialized non-elastomeric stem seals, and Class VI seat shut-off ensure safe handling of volatile light gases.
Procurement Intelligence
Frequently Asked Questions for Valve Procurement in Azerbaijan
Addressing engineering specifications, PED certification nuances, material compatibility, and documentation for international projects.
What specific CE PED certifications apply to globe valves imported into Azerbaijan?
Our globe valves conform to the European Pressure Equipment Directive (PED 2014/68/EU) under Conformity Assessment Module H (Full Quality Assurance). This covers design, casting, machining, hydrostatic pressure testing, and final tagging. Because many major operators in Azerbaijan (e.g., BP-operated consortia) adopt European design codes, CE marking along with ISO 9001 and EN 10204 3.1 metallic traceability provides direct regulatory clearance for greenfield and brownfield projects alike.
How do your globe valves combat cavitation during high differential pressure throttling?
For critical applications such as boiler feedwater, steam bypass, or gas blowdown, we employ multi-stage tortuous path trims and perforated anti-cavitation cages. These designs force fluid through multiple pressure-drop stages, ensuring the localized vena contracta pressure remains strictly above the fluid vapor pressure, preventing micro-implosions and cavitation erosion of the seat and body.
Are materials compliant with NACE MR0175 / ISO 15156 for Caspian sour gas and crude oil?
Yes. Crude and natural gas streams extracted from the Caspian offshore fields contain elevated concentrations of hydrogen sulfide (H2S) and carbon dioxide (CO2). We manufacture NACE-compliant globe valves using heat-treated carbon steels (WCB/A105 with maximum hardness under 22 HRC), 316/316L, Duplex (2205), and Inconel 625 trims that systematically prevent sulfide stress cracking (SSC) and hydrogen-induced cracking (HIC).
What lead times and logistical solutions exist for deliveries to Baku or Sumgayit?
Standard stocked carbon and stainless steel components allow lead times as brief as 3 to 4 weeks for common sizes (DN15–DN200, Class 150–600). Custom forged, high-pressure alloy models are completed within 8 to 12 weeks. We routinely coordinate freight forwarding through the Middle Corridor rail and sea routes, clearing through the Port of Baku (Alat) or arriving via air freight for urgent operational shutdowns.
Can valves be supplied with electric, pneumatic, or electro-hydraulic actuators?
All our globe valves feature ISO 5210 / ISO 5211 top mounting flanges designed to accommodate pneumatic piston/diaphragm actuators, multi-turn electric actuators (AUMA, Rotork, or equivalent), and hydraulic systems. Actuated assemblies undergo factory integration, stroke speed calibration, and zero-leakage bench validation prior to dispatch.
Comprehensive Flow Inventory
Integrated Check & Butterfly Valve Solutions for Azerbaijan Projects
Engineered fluid handling assemblies built to complement globe valve configurations across utility, municipal water, fire protection, and industrial systems in the Caspian market.
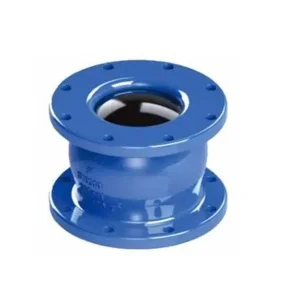
High-Quality High - Performance Silent Check Valve for Water Supply Systems in Azerbaijan
Explore Specification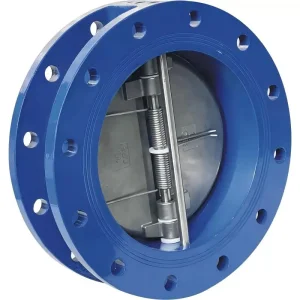
CE Certification Dual Plate Check Valve, Reliable Backflow Prevention Device for Azerbaijan Process Plants
Explore Specification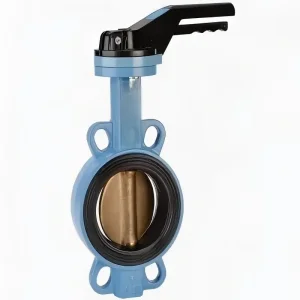
CE Certification Bronze Disc Wafer Butterfly Valve - Durable & Efficient for Caspian Seawater Cooling
Explore Specification
High-Quality EPDM Lining Butterfly Valve - Durable & Corrosion Resistant for Absheron Utility Mains
Explore Specification
Wholesale Wafer Butterfly Valve - Durable & Efficient Flow Control Solution for Azerbaijan Facilities
Explore Specification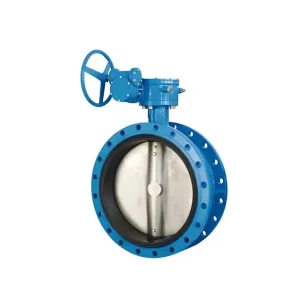
Wholesale Low - Torque Flange Type Butterfly Valve for Heavy Pipeline Infrastructure in Azerbaijan
Explore Specification
Wholesale Fire-Fighting Wafer Signal Butterfly Valve for Critical Commercial & Industrial Sites
Explore Specification
