
Featured Industrial Flow Control Units · Direct Sourced
Engineered under stringent internal foundry controls with vulcanized elastomeric seals, certified for subterranean, municipal, marine, and process fluid infrastructures.





Global Landscape: The Subterranean Pipeline Valve Evolution
Modern urbanization demands infrastructure that operates reliably out of sight. The transition from legacy metal-seated valves housed in expensive concrete inspection chambers to directly buried elastic seat gate valves has redefined pipeline life-cycle economics worldwide.
North American Water Works Standard (AWWA C509/C515)
In the Americas, direct burial standards require high-strength ductile iron bodies (ASTM A536) coated with thermosetting fusion-bonded epoxy (AWWA C550). Municipal asset management programs prioritize manual buried elastic seat gate valves equipped with 2-inch square operating nuts and telescopic ground stems to withstand freeze-thaw cycles without surface soil disruption.
European & British Standards (EN 1074-1/2, DIN 3352)
Across Western Europe and Scandinavia, directives mandate non-rising stainless steel stems with triple O-ring shaft sealing systems rated for chamberless subterranean immersion. GSK-certified epoxy powder coatings (>250 μm) safeguard against electrolytic soil corrosion, eliminating manhole maintenance, traffic interference, and road settlement hazards.
Middle East, Asia & Mega-Desalination Outlets
High ambient ground temperatures and hyper-saline desert subsoils in the GCC and APAC require extreme chemical resilience. Buried elastic seat gate valves with internal/external electrostatically applied FBE, paired with fully rubber-encapsulated ductile iron wedges and dezincification-resistant brass or duplex stem nuts, resist groundwater brackish permeation.
Vertically Integrated Valve Foundry & Rubber Compounding
Why do EPC contractors and global utility conglomerates partner with Tianjin Top Valve? Unlike trading intermediaries, our group controls every metallurgical and elastomer parameter under one manufacturing roof.
Foundry Heritage Since 1996
Tianjin Donglian Valve Factory pours our ductile iron (QT450-10 / QT500-7) bodies in automated resin-sand molding lines, guaranteeing minimum 10% elongation and high impact toughness against ground shift.
Rubber Plant Since 1987
Tianjin Dongfang Rubber Factory synthesizes and vulcanizes our EPDM wedge encapsulation. Achieving exceptional permanent compression set resistance, our wedges ensure zero micro-cracking and flawless elastic memory over 50 years.
CNC Precision Machining
Multi-axis CNC machining centers finish stem threads (AISI 420 / 431 / 316), seal journals, and flange faces in single clamping setups, eliminating axial runout and reducing operating torque by over 30%.
100% Dual-Direction Pressure Test
Every manufactured unit undergoes 1.5x body hydrostatic shell testing and 1.1x bi-directional seat leakage testing in our physical and chemical lab before receiving ISO 9001, WRAS, or CE sign-off.
Technical Specification Architecture: Buried Elastic Seat Gate Valve
Engineered explicitly for direct underground burial without manholes, featuring an extension spindle assembly, surface street box, and multi-layered debris ingress exclusion.
| Engineering Parameter | Standard Specification | Advanced Heavy-Duty Customization | Diagnostic Benefit |
|---|---|---|---|
| Nominal Diameter (DN) | DN50 to DN600 (2" – 24") | DN700 to DN1200 (28" – 48") | Full-bore passage; piggable, zero sediment traps. |
| Pressure Rating | PN10, PN16 (1.0 – 1.6 MPa) | PN25 (2.5 MPa) / Class 150/250 | Withstands transient water hammer and pump pressure surges. |
| Body & Bonnet Material | Ductile Iron EN-GJS-450-10 / 500-7 | ASTM A536 65-45-12 / WCB Cast Steel | High yield strength; resists overburden and dynamic traffic loads. |
| Resilient Wedge Lining | Potable Grade EPDM (WRAS Approved) | NBR for hydrocarbons / FKM for chemical | 100% vulcanization to wedge core; zero adhesive failure. |
| Stem Metallurgy | Stainless Steel 2Cr13 / AISI 420 | AISI 304, AISI 316, Duplex 2205 | Cold-rolled ACME threads ensure low operating torque. |
| Stem Sealing System | 3× NBR O-Rings + Dust Lip Seal | Replaceable under full line pressure (online) | Guarantees zero soil water back-contamination. |
| External/Internal Coating | Fusion Bonded Epoxy (FBE) ≥250 μm | GSK Certified ≥300 μm (Holiday-free 3kV) | Immune to biogenic acidic subsoil and galvanic corrosion. |
| Direct Burial Actuation | Square Cap (30×30mm) + Telescopic Stem | Bevel Gearbox + IP68 Smart Actuator | Enables surface operation via T-key through a road box. |
Technology Roadmap: 2026–2030
Integration of passive RFID chips and NB-IoT wireless pressure/torque sensors embedded inside the subterranean street box. Real-time telemetry detects illegal tap-ins, valve position verification (open/close percentage), and predictive gasket degradation.
PFAS-Free Rubber Compounding
Ahead of stringent EU and EPA potable water guidelines, our in-house rubber lab is transitioning to ultra-pure, peroxide-cured EPDM elastomers that are 100% free of forever chemicals, eliminating micro-contaminant leaching in drinking water mains.
Seismic & Ground Subsidence Resilience
Incorporating self-aligning ball-socket flanged adaptations and flexible restrained joints. When tectonic shifting or ground soil compaction occurs, our manual buried gate valves absorb angular deflection without wedge jamming.
Engineered Solutions for Critical Infrastructure Networks
Direct burial configurations eliminate confined-space worker hazards, minimize roadway congestion, and isolate distribution segments during mainline bursts.
Municipal Potable Water Mains
Installed below the frost line with telescopic spindles reaching grade level. The full-bore, cavity-free bottom design prevents the accumulation of sand, grit, and pipe scale, ensuring zero leakage during emergency quadrant isolation.
District Cooling & Chilled Water Sub-Loops
For campus and metropolitan district energy schemes, valves are buried directly in wet, compacted gravel backfill. Multi-layer external polyurethane or fusion epoxy prevents sweat corrosion, maintaining insulation integrity.
Subsurface Fire Protection Ring Mains
Industrial petrochemical refineries and logistics hubs deploy non-rising stem elastic seat gate valves equipped with ground surface position indicators, ensuring quick verification of valve status during NFPA safety audits.
Engineering & Procurement FAQ
Key considerations for utility engineers, pipeline contractors, and procurement officers specifying subterranean valves.
What distinguishes a manual buried elastic seat gate valve from a conventional flanged gate valve?
How does your factory prevent wedge elastomer stripping or disbonding over decades underground?
Can the stem sealing O-rings be serviced or replaced while the pipeline is in active operation?
What anti-corrosion coating standards do your buried valves comply with?
Which international pipe connection drilling patterns can you match?
Specialized Process Valves & Pipeline Check Solutions
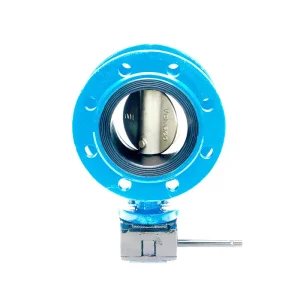
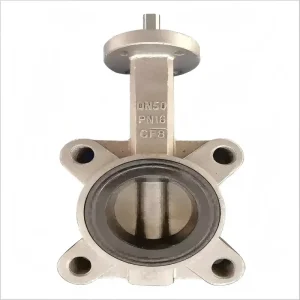
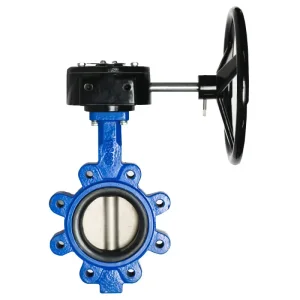
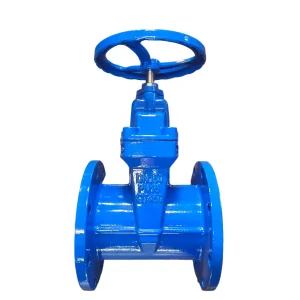
Complementing our buried elastic seat gate valves, Tianjin Top Valve produces an exhaustive array of high-durability valves for comprehensive plant, municipal, and process pipeline management.



Partner Directly with Tianjin Top Valve Group
Eliminate intermediary risk with our foundry-direct supply chain. Access standard compliance certificates, 2D/3D CAD models, material mill test certificates (EN 10204 3.1), and schedule a live engineer video factory audit.
